BODY PANEL FRONT SIDE MEMBER(for TMC Made) ASSEMBLY REPLACEMENT
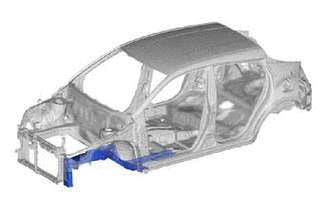
With the front fender apron assembly removed.
REMOVAL
| Symbol Meaning | |
|---|---|

|
Remove Weld Points |

|
Cut with Disc Sander etc. |
Remove the torque box sub-assembly front.
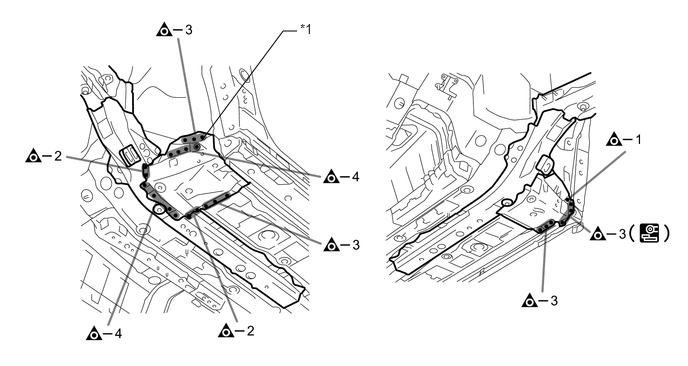
| *1 | TORQUE BOX SUB-ASSEMBLY FRONT | - | - |
Remove the front side member sub-assembly and A.
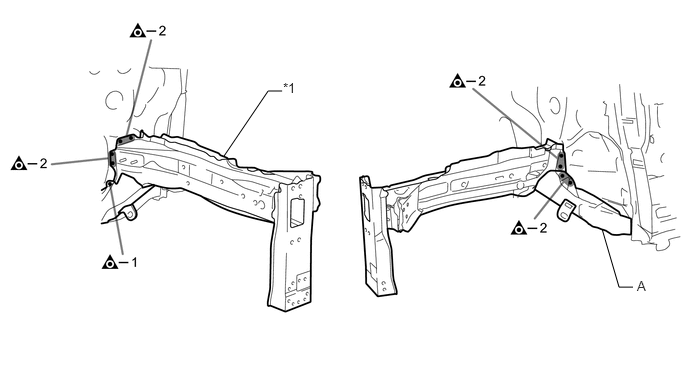
| *1 | FRONT SIDE MEMBER SUB-ASSEMBLY | - | - |
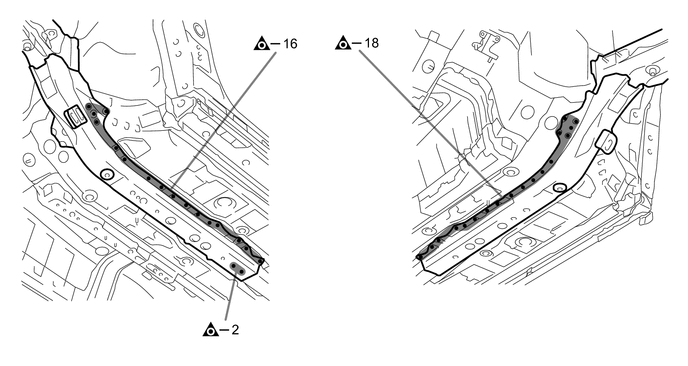
INSTALLATION
| Symbol Meaning | |
|---|---|

|
Plug Weld |

|
Plug Weld |

|
Fillet Weld |
Temporarily install the new parts and measure each part of the new parts in accordance with the body dimension diagram. (See the body dimensions)
Make sure to attach correctly in accordance with the body dimension diagram as this part affects the front wheel alignment.
Before temporarily installing the new parts, weld the front side member inner rear,front side member reinforcement sub-assembly No.2,front side member plate rear and transport hook with the standard number of welding points.
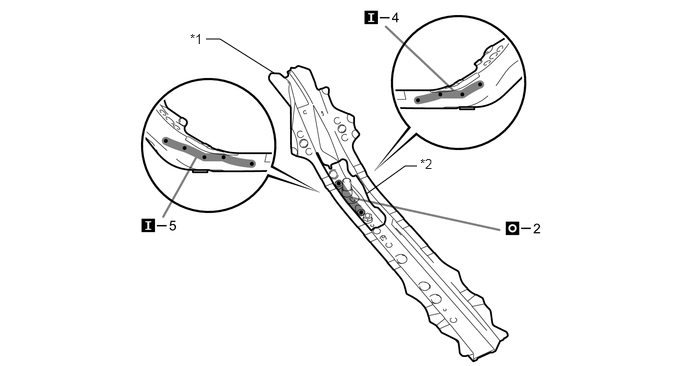
| *1 | FRONT SIDE MEMBER INNER REAR | *2 | FRONT SIDE MEMBER REINFORCEMENT SUB-ASSEMBLY NO. 2 |
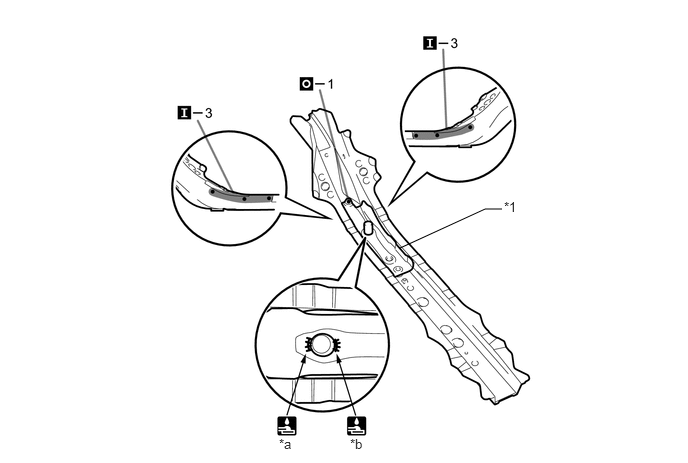
| *1 | FRONT SIDE MEMBER PLATE REAR | - | - |
| *a | 14.8 mm (0.58 in.) | *b | 20 mm (0.79 in.) |
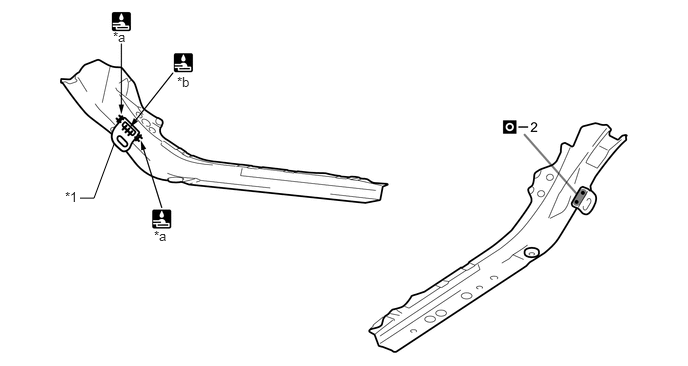
| *1 | TRANSPORT HOOK | - | - |
| *a | 18 mm (0.71 in.) | *b | 27 mm (1.06 in.) |
Before temporarily installing the new parts, weld the front side member sub-assembly and A with the standard number of welding points.
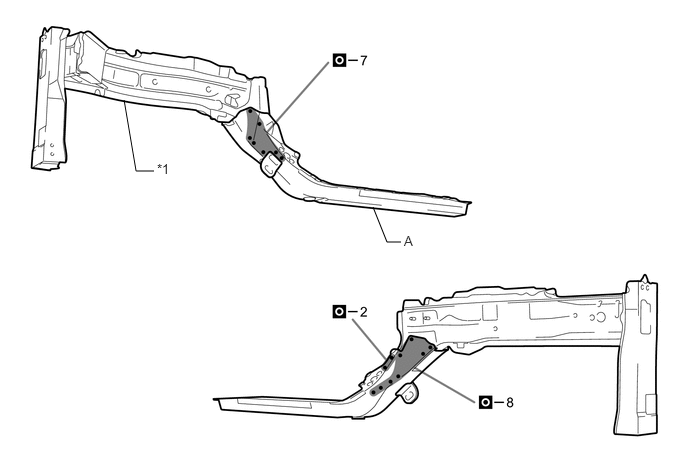
| *1 | FRONT SIDE MEMBER SUB-ASSEMBLY | - | - |
Weld the front side member sub-assembly and A to the vehicle side.
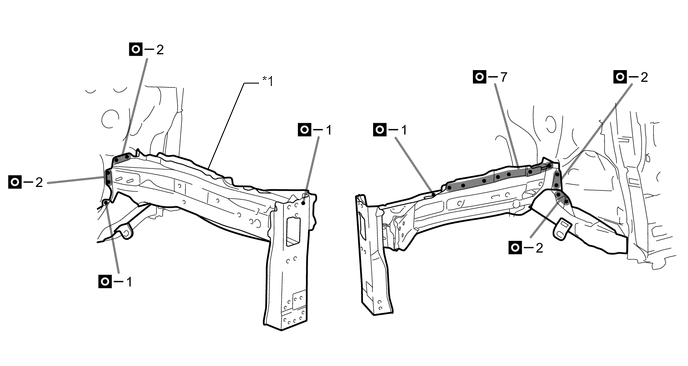
| *1 | FRONT SIDE MEMBER SUB-ASSEMBLY | - | - |
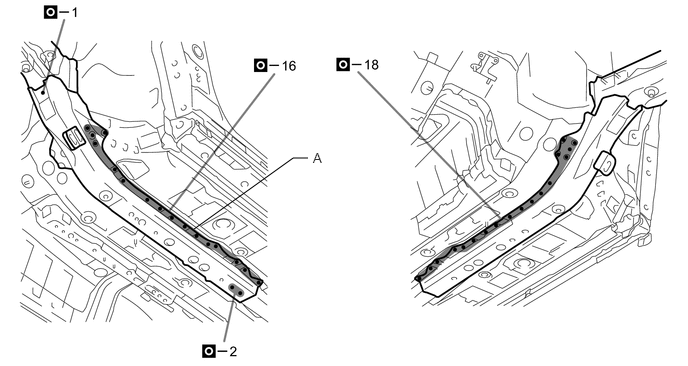
Weld the torque box sub-assembly front to the vehicle side.
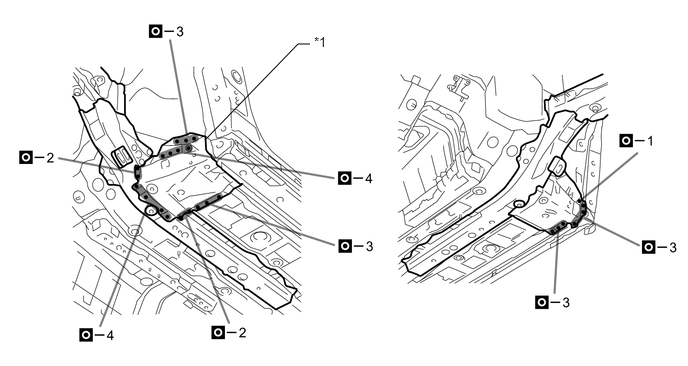
| *1 | TORQUE BOX SUB-ASSEMBLY FRONT | - | - |
After welding, apply body sealer and undercoating to the corresponding parts. (See the painting/coating)
After applying the top coat, apply anti-rust agent to the internal panel portion of the closed section structural weld points.