3ZR-FAE ENGINE MECHANICAL CYLINDER HEAD REPAIR
PROCEDURE

 11131
1.REPAIR INTAKE VALVE SEAT
- NOTICE:
- ·
Repair the intake valve seat while checking the seating position.
·Keep the lip free from foreign matter.
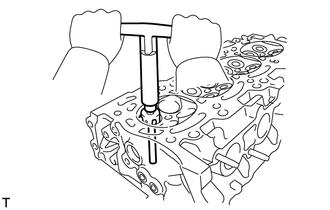
Using a 45° cutter, resurface the intake valve seat so that the intake valve seat width is more than the standard.
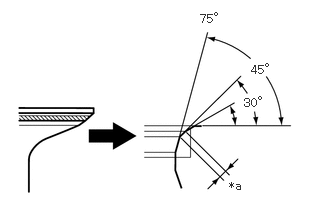
| *a | Width |
Using 30° and 75° cutters, correct the intake valve seat so that the intake valve contacts the entire circumference of the intake valve seat. The contact should be in the center of the intake valve seat, and the intake valve seat width should be as specified around the entire circumference of the intake valve seat.
- Standard Width:
1.0 to 1.4 mm (0.0394 to 0.0551 in.)
Hand lap the intake valve and intake valve seat with an abrasive compound.
Check the intake valve seating position.
11135
2.REPAIR EXHAUST VALVE SEAT
- NOTICE:
- ·
Repair the exhaust valve seat while checking the seating position.
·Keep the lip free from foreign matter.
Using a 45° cutter, resurface the exhaust valve seat so that the exhaust valve seat width is more than the standard.
| *a | Width |
Using 30° and 75° cutters, correct the exhaust valve seat so that the exhaust valve contacts the entire circumference of the exhaust valve seat. The contact should be in the center of the exhaust valve seat, and the exhaust valve seat width should be as specified around the entire circumference of the exhaust valve seat.
- Standard Width:
1.0 to 1.4 mm (0.0394 to 0.0551 in.)
Hand lap the exhaust valve and exhaust valve seat with an abrasive compound.
Check the exhaust valve seating position.