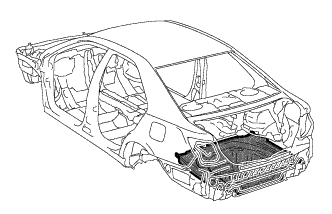
REAR FLOOR PAN > ASSEMBLY REPLACEMENT | |
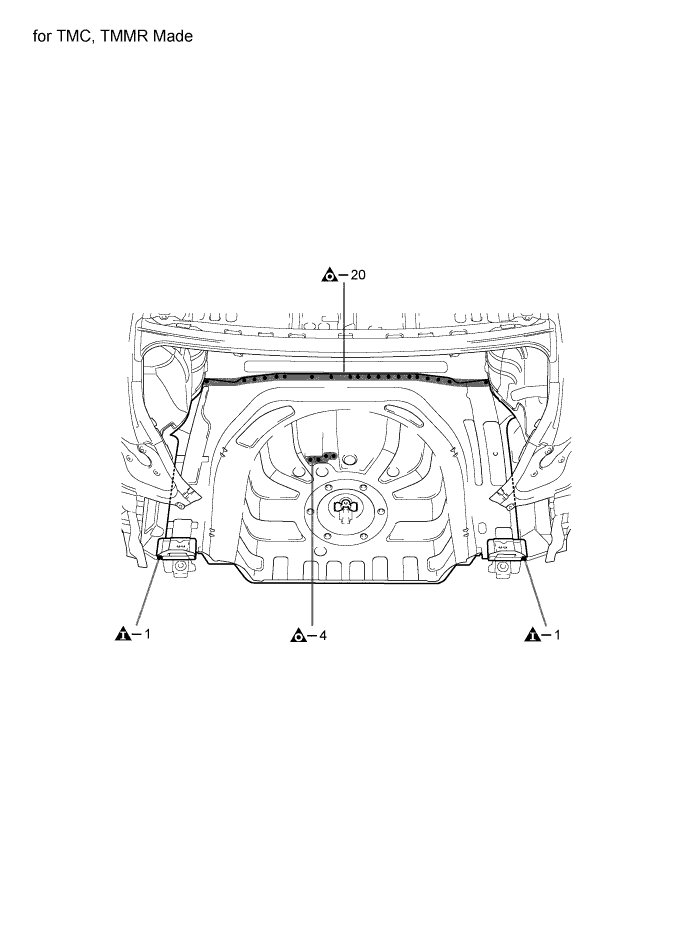
- With the rear floor rear inner crossmember removed.
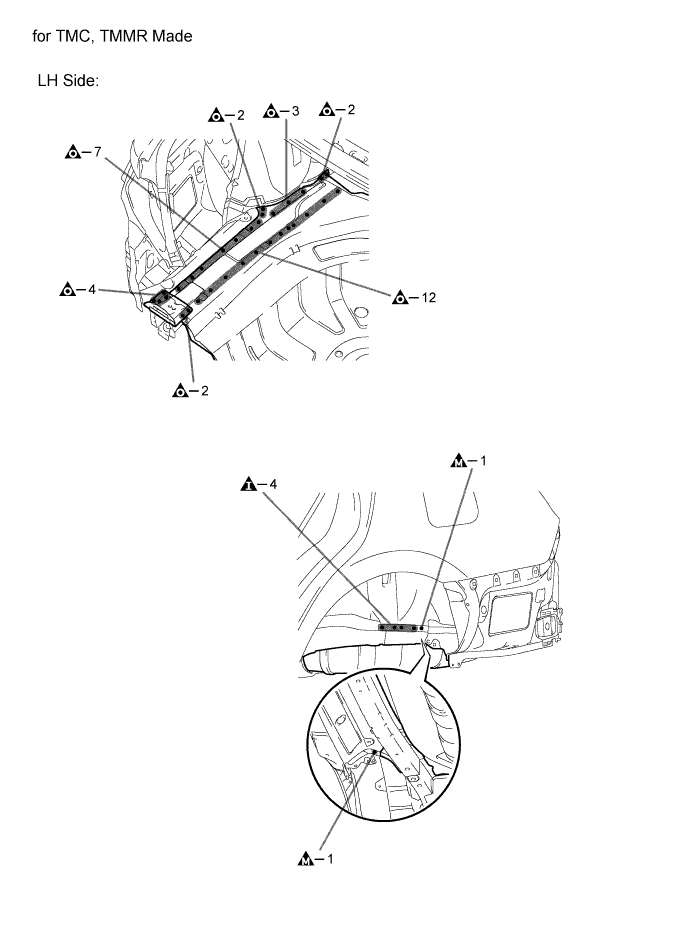
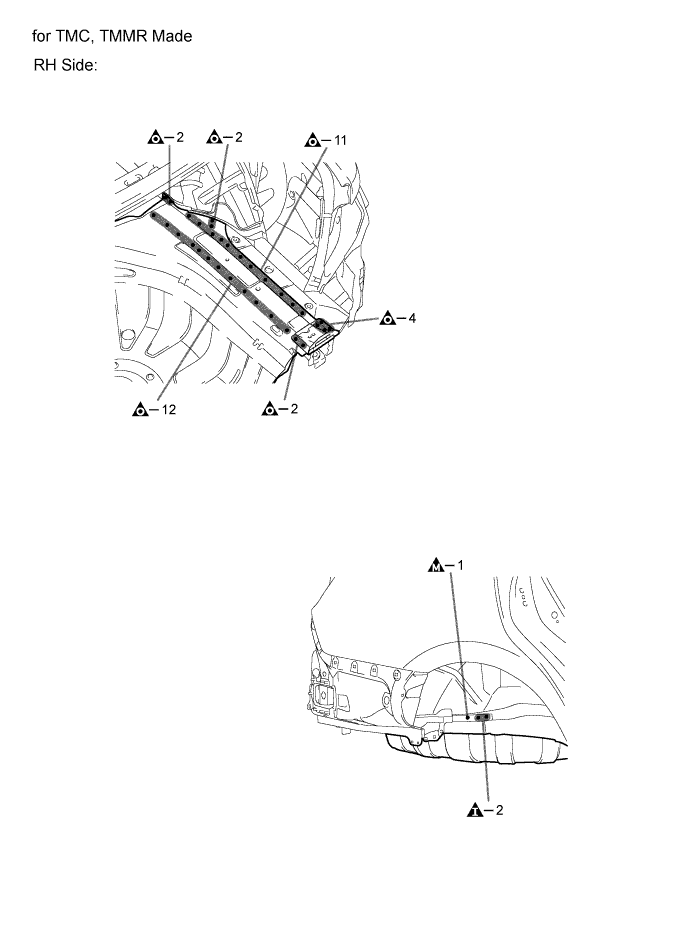
Symbol meaning
|

| Remove Weld Points
|

| Remove Weld Points
|

| Remove Weld Points
|
Symbol meaning
|

| Plug Weld
|

| Plug Weld
|

| Plug Weld
|

| Fillet Weld
|
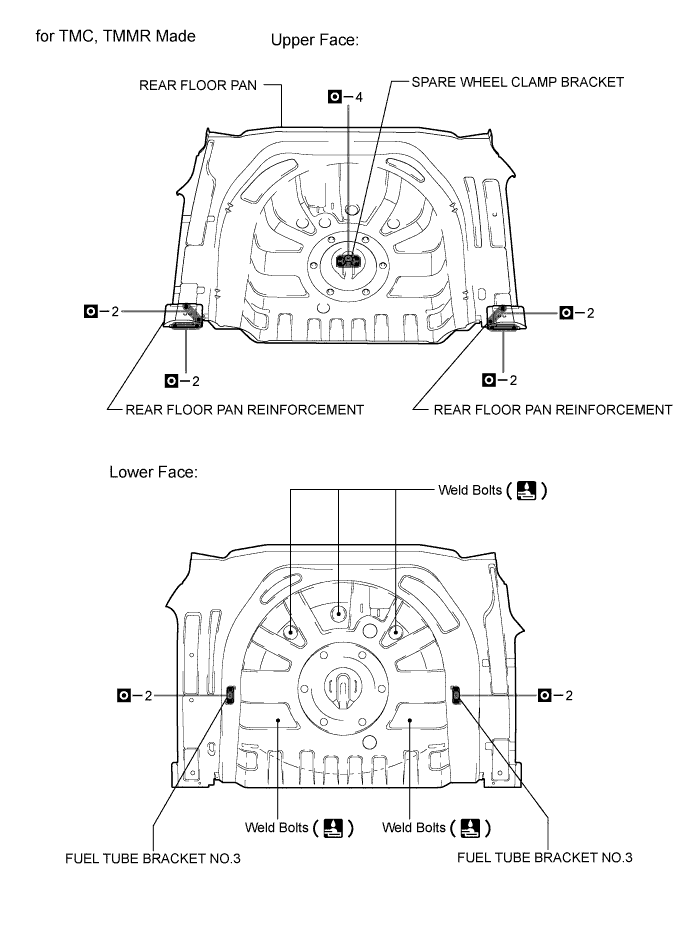
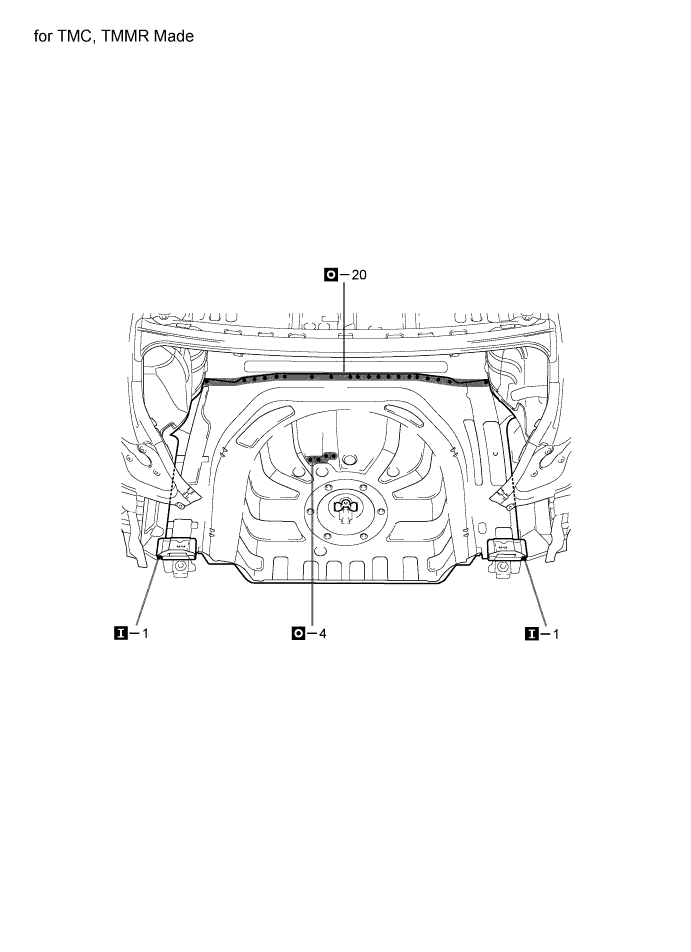
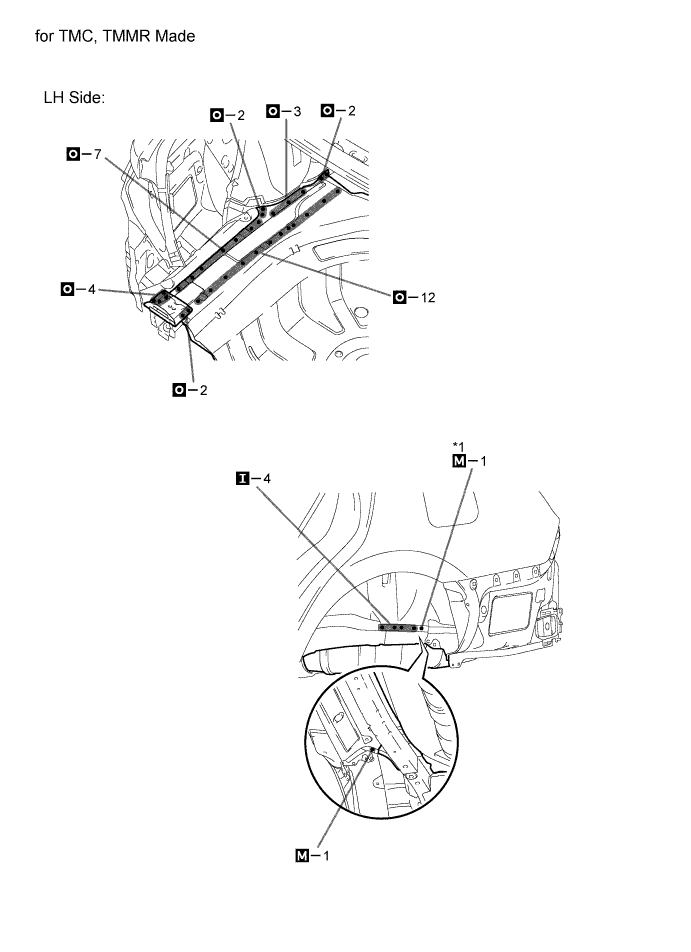
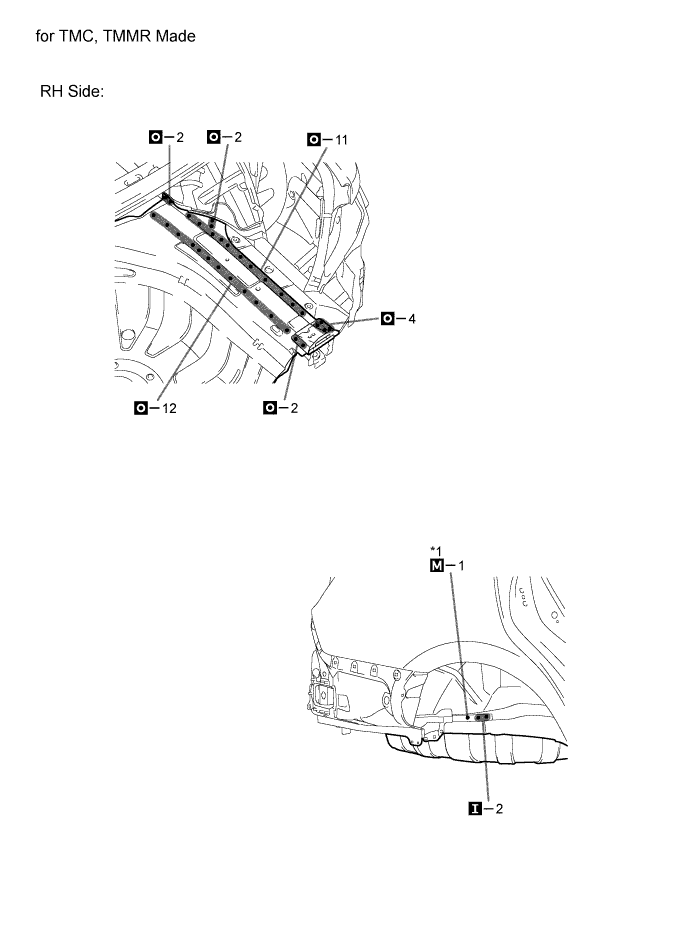
INSTALLATION POINT (for TMC, TMMR Made)
- Temporarily install the new parts and measure each part of the new parts in accordance with the body dimension diagram. (See the body dimension diagram)
- Before temporarily installing the new parts, weld the spare wheel clamp bracket, rear floor pan reinforcement, fuel tube bracket No. 3 and weld bolts with the standard number of welding points.
- When welding *1, make a hole on a new part for plug welding and weld the panel with the panel behind completely.
- After welding, apply body sealer and undercoating to the corresponding parts. (See the painting / coating)
- After applying the top coat, apply anti-rust agent to the internal panel portion of the closed section structural weld points.
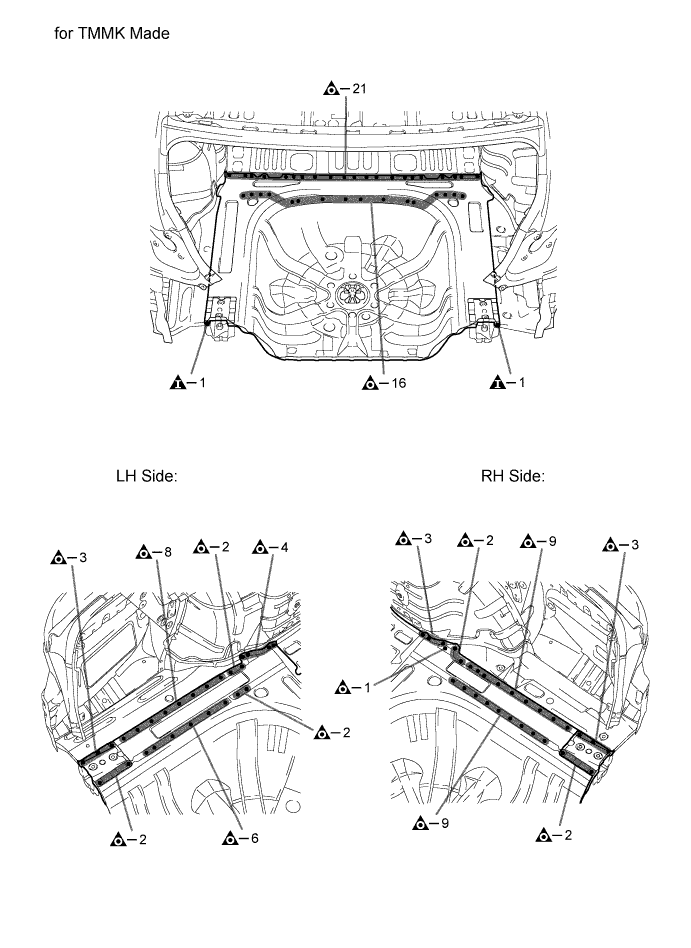
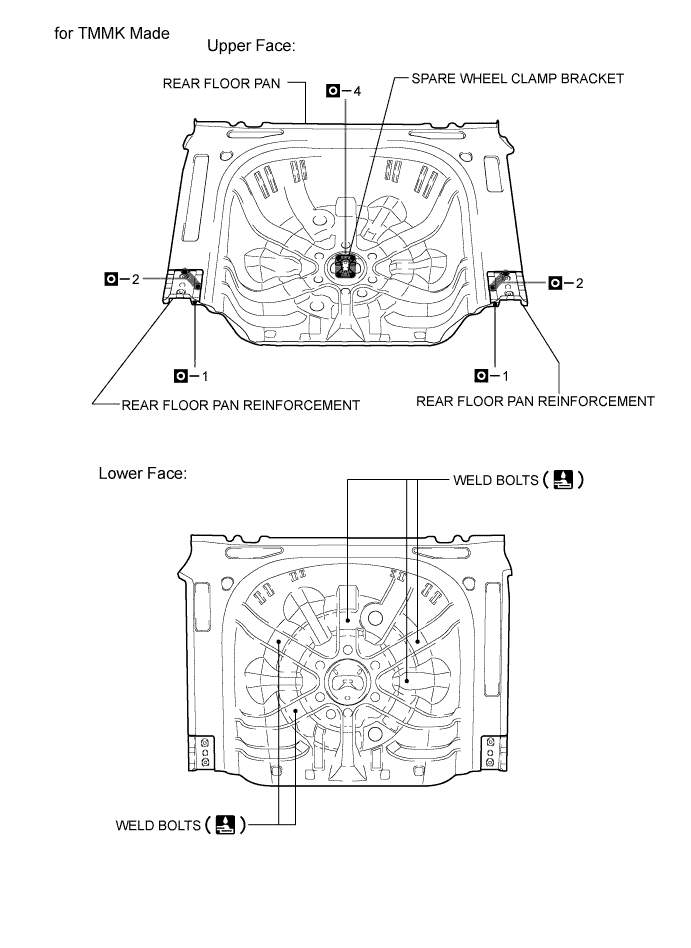
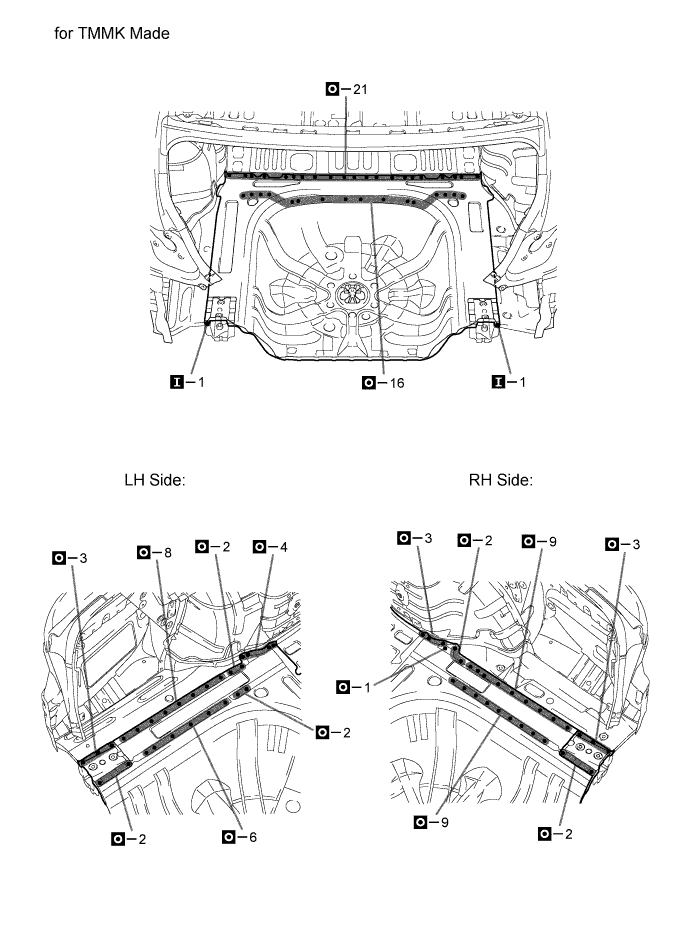
INSTALLATION POINT (for TMMK Made)
- Temporarily install the new parts and measure each part of the new parts in accordance with the body dimension diagram. (See the body dimension diagram)
- Before temporarily installing the new parts, weld the spare wheel clamp bracket, rear floor pan reinforcement and weld bolts with the standard number of welding points.
- When welding *1, make a hole on a new part for plug welding and weld the panel with the panel behind completely.
- After welding, apply body sealer and undercoating to the corresponding parts. (See the painting / coating)
- After applying the top coat, apply anti-rust agent to the internal panel portion of the closed section structural weld points.