CYLINDER HEAD > INSPECTION |
| 1. INSPECT CYLINDER HEAD SUB-ASSEMBLY |
![]() |
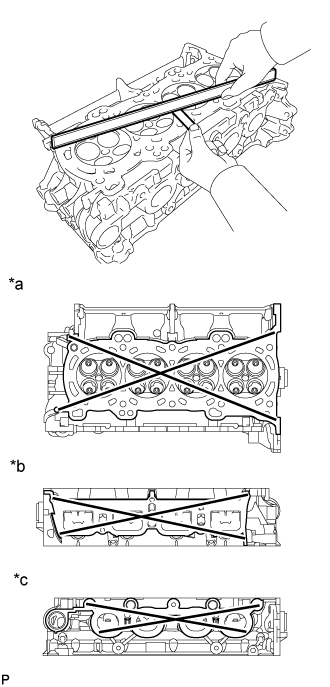
Using a precision straightedge and feeler gauge, measure the warpage of the contact surfaces where the cylinder head contacts the cylinder block and manifold.
| Item | Specified Condition |
| Cylinder head lower side | 0.05 mm (0.00197 in.) |
| Intake manifold side | 0.10 mm (0.00394 in.) |
| Exhaust manifold side | 0.10 mm (0.00394 in.) |
| *a | Cylinder Head Lower Side |
| *b | Intake Manifold Side |
| *c | Exhaust Manifold Side |
![]() |
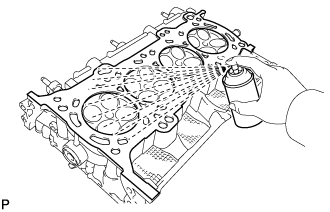
Using a dye penetrant, check the intake ports, exhaust ports and cylinder surface for cracks.
If cracked, replace the cylinder head.
| 2. INSPECT COMPRESSION SPRING |

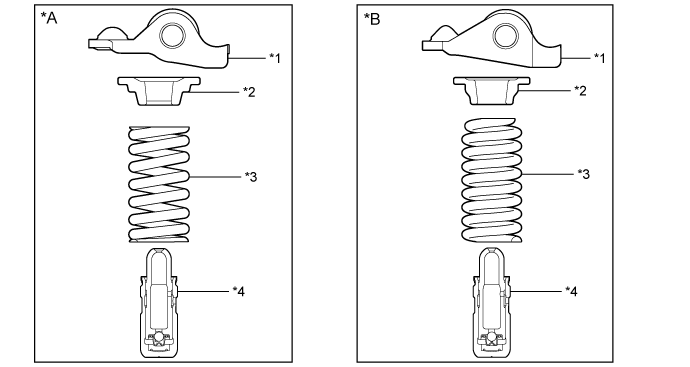
| *A | Type A (Compression Spring Shape: Straight) | *B | Type B (Compression Spring Shape: Tapered) |
| *1 | No. 1 Valve Rocker Arm Sub-assembly | *2 | Valve Spring Retainer |
| *3 | Compression Spring | *4 | Valve Lash Adjuster Assembly |
Type A:
![]() |
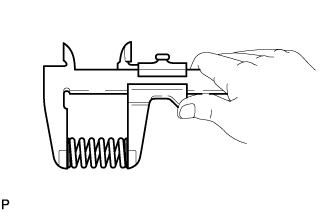
Using a vernier caliper, measure the free length of the compression spring.
| Wire Diameter | Specified Condition |
| 3.3 mm (0.130 in.) | 49.0 to 51.0 mm (1.93 to 2.01 in.) |
| 3.4 mm (0.134 in.) | 47.2 to 49.2 mm (1.86 to 1.94 in.) |
![]() |
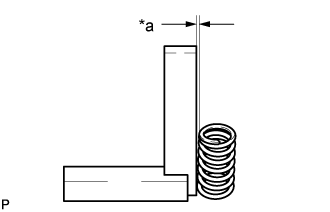
Using a steel square, measure the deviation of the compression spring.
| *a | Deviation |
Type B:
![]() |
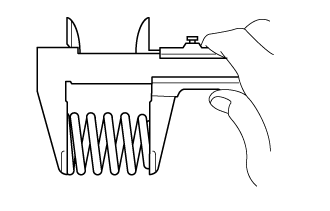
Using a vernier caliper, measure the free length of the compression spring.
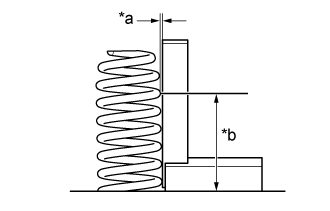
![]() |
Using a steel square, measure the deviation of the compression spring at the position shown in the illustration.
| *a | Deviation |
| *b | 30 mm (1.18 in.) |
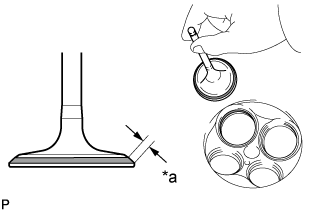
| 3. INSPECT INTAKE VALVE |
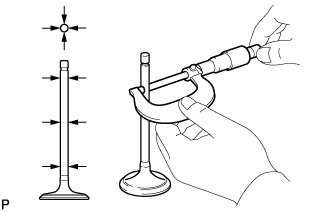
![]() |
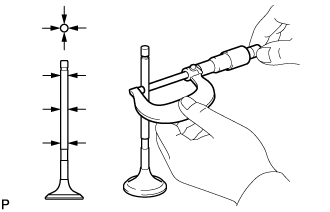
Using a micrometer, measure the diameter of the valve stem.
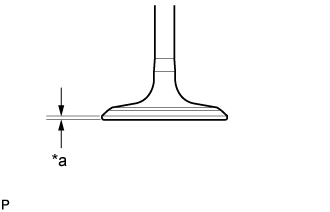
![]() |
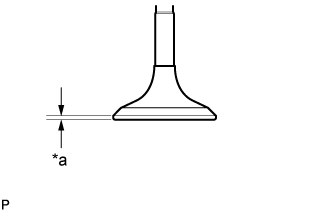
Using a vernier caliper, measure the valve head margin thickness.
| *a | Margin Thickness |
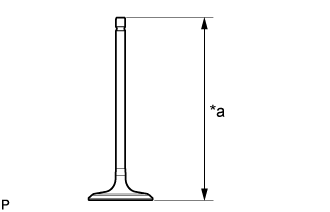
![]() |
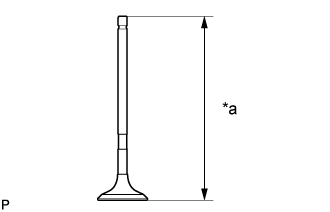
Using a vernier caliper, measure the overall length of the valve.
| *a | Overall Length |
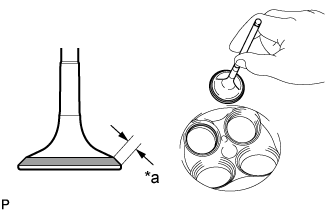
| 4. INSPECT EXHAUST VALVE |
![]() |
Using a micrometer, measure the diameter of the valve stem.
![]() |
Using a vernier caliper, measure the valve head margin thickness.
| *a | Margin Thickness |
![]() |
Using a vernier caliper, measure the overall length of the valve.
| *a | Overall Length |
| 5. INSPECT VALVE GUIDE BUSH OIL CLEARANCE |
![]() |
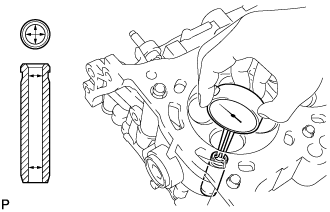
Using a caliper gauge, measure the inside diameter of the guide bush.
Subtract the valve stem diameter measurement from the guide bush inside diameter measurement.
| Item | Specified Condition |
| Intake | 0.025 to 0.060 mm (0.000984 to 0.00236 in.) |
| Exhaust | 0.030 to 0.065 mm (0.00118 to 0.00256 in.) |
| Item | Specified Condition |
| Intake | 0.08 mm (0.00315 in.) |
| Exhaust | 0.10 mm (0.00394 in.) |
| 6. INSPECT INTAKE VALVE SEAT |
Apply a light coat of Prussian blue to the valve face.
![]() |
Lightly press the valve face against the valve seat.
| *a | Width |
Check the valve face and valve seat.
Check that the contact surfaces of the valve seat and valve face are in the middle area of their respective surfaces, with the width between 1.0 and 1.4 mm (0.0394 and 0.0551 in.).
If not, correct the valve seat.
Check that the contact surfaces of the valve seat and valve face are even around the entire valve seat.
If not, correct the valve seat.
| 7. INSPECT EXHAUST VALVE SEAT |
Apply a light coat of Prussian blue to the valve face.
![]() |
Lightly press the valve face against the valve seat.
| *a | Width |
Check the valve face and valve seat.
Check that the contact surfaces of the valve seat and valve face are in the middle area of their respective surfaces, with the width between 1.2 and 1.6 mm (0.0472 and 0.0630 in.).
If not, correct the valve seat.
Check that the contact surfaces of the valve seat and valve face are even around the entire valve seat.
If not, correct the valve seat.
| 8. INSPECT CAMSHAFT OIL CLEARANCE |
Clean the bearing caps, camshaft housing and camshaft journals.
Place the camshafts on the camshaft housing.
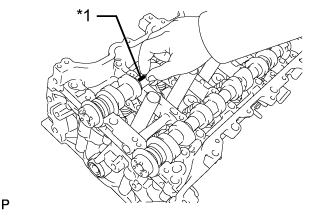
![]() |
Lay a strip of Plastigage across each of the camshaft journals.
| *1 | Plastigage |
Install the camshaft bearing caps .
Install the camshaft housing sub-assembly .
Remove the camshaft bearing caps .
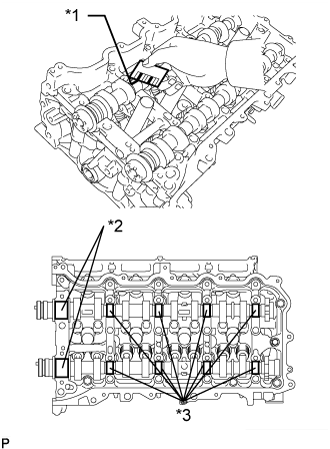
![]() |
Measure the Plastigage at its widest point.
| Item | Specified Condition |
| Intake No. 1 journal | 0.035 to 0.072 mm (0.00137 to 0.00283 in.) |
| Exhaust No. 1 journal | 0.049 to 0.086 mm (0.00193 to 0.00339 in.) |
| Other journal | 0.025 to 0.062 mm (0.000984 to 0.00244 in.) |
| Item | Specified Condition |
| Intake No. 1 journal | 0.085 mm (0.00335 in.) |
| Exhaust No. 1 journal | 0.095 mm (0.00374 in.) |
| Other journal | 0.085 mm (0.00335 in.) |
| *1 | Plastigage |
| *2 | No. 1 Journal |
| *3 | Other Journal |
| 9. INSPECT CAMSHAFT THRUST CLEARANCE |
Clean the bearing caps, camshaft housing and camshaft journals.
Place the camshafts on the camshaft housing.
Install the camshaft bearing caps .
Install the camshaft housing sub-assembly .
![]() |
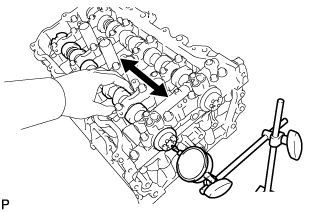
Using a dial indicator, measure the thrust clearance while moving the camshaft back and forth.
| Item | Specified Condition |
| Intake | 0.060 to 0.155 mm (0.00236 to 0.00610 in.) |
| Exhaust | 0.060 to 0.155 mm (0.00236 to 0.00610 in.) |
| Item | Specified Condition |
| Intake | 0.170 mm (0.00669 in.) |
| Exhaust | 0.170 mm (0.00669 in.) |