BODY PANEL FRONT SIDE MEMBER FRONT(for Type A) ASSEMBLY REPLACEMENT
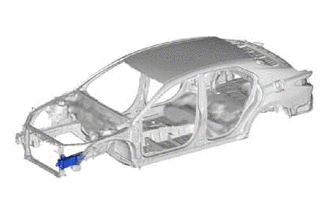
With the radiator side support assembly and front fender front apron cut and join replacement sections removed.
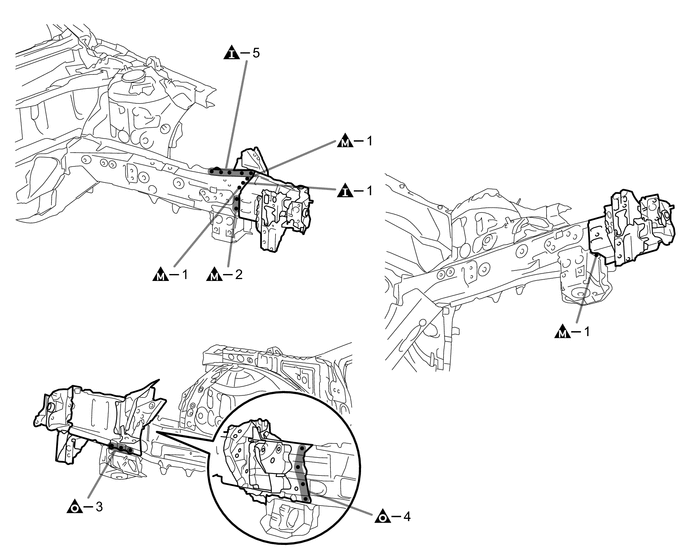
REMOVAL
| Symbol Meaning | |
|---|---|

|
Remove Weld Points |

|
Remove Weld Points |

|
Remove Weld Points |
Do not butt weld or heat repair because the heat decreases the strength of areas where ultra high strength steel is used. (See the introduction)
INSTALLATION
| Symbol Meaning | |
|---|---|

|
Spot Weld |

|
Plug Weld |

|
Plug Weld |

|
Plug Weld |
Temporarily install the new parts and measure each part of the new parts in accordance with the body dimension diagram. (See the body dimensions)
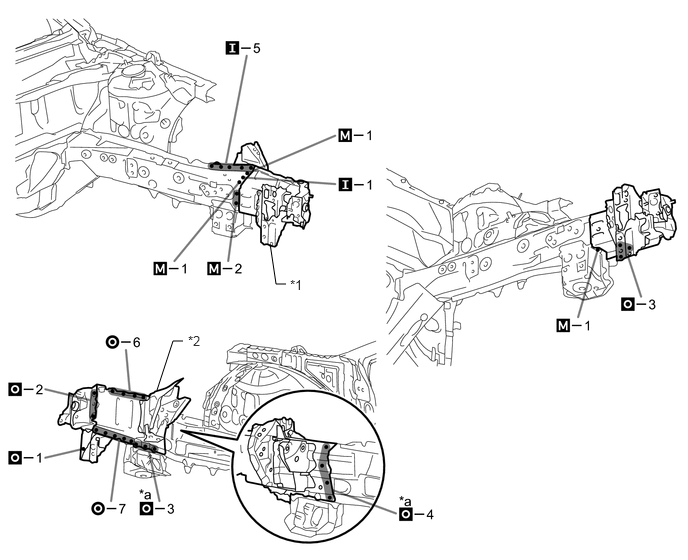
| *1 | FRONT SIDE MEMBER BRACKET SUB-ASSEMBLY | *2 | BODY MOUNTING BRACKET SUB-ASSEMBLY NO. 2 |
| *a | Ultra High Strength Steel Welding Point | - | - |
When welding 2 panels together including 980 MPa ultra high strength steel.
| *a: Plug weld | Plug diameter | 10 mm (0.39 in.) |
| Wire type | AWS A5.18 ER70S-3 | |
| Shield gas | Metal active gas |
- NOTICE:
-
Be sure to use Metal active gas (Ar 80% + CO2 20%) as the shield gas when plug welding.Sufficient weld strength cannot be assured when using 100% CO2 shield gas.
After applying the top coat, apply anti-rust agent to the internal panel portion of the closed section structural weld points.