INTRODUCTION ABOUT THIS VEHICLE STRUCTURAL OUTLINE
for Standard Body
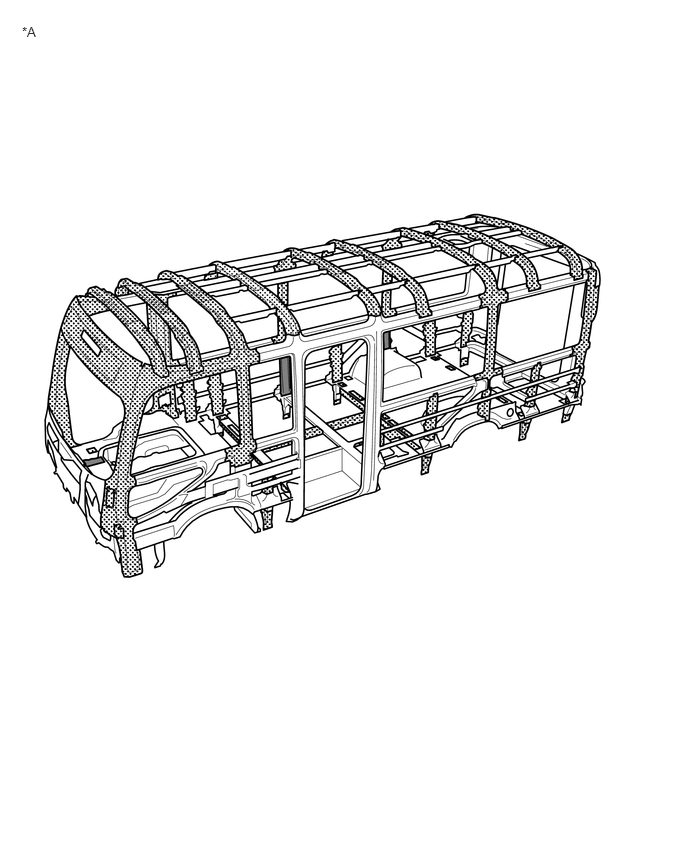
| *A | for Double Swing Out Type | - | - |

0,0 0,0
false
|
590 MPa High Strength Steel | 
0,0 0,0
false
|
440 MPa High Strength Steel |
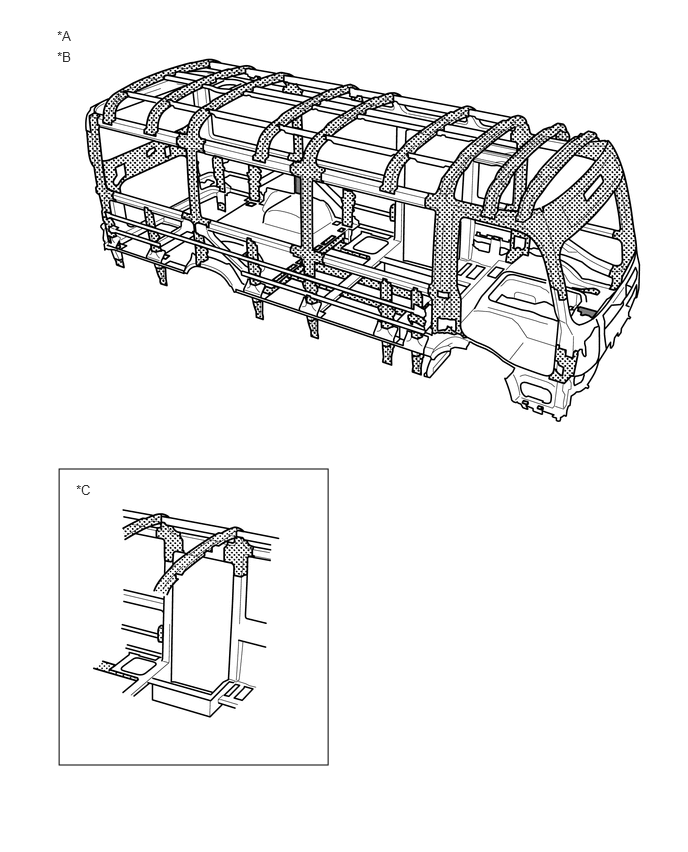
| *A | for Luggage Compartment | *B | for Glide Type |
| *C | for Folding Type | - | - |

0,0 0,0
false
|
590 MPa High Strength Steel | 
0,0 0,0
false
|
440 MPa High Strength Steel |
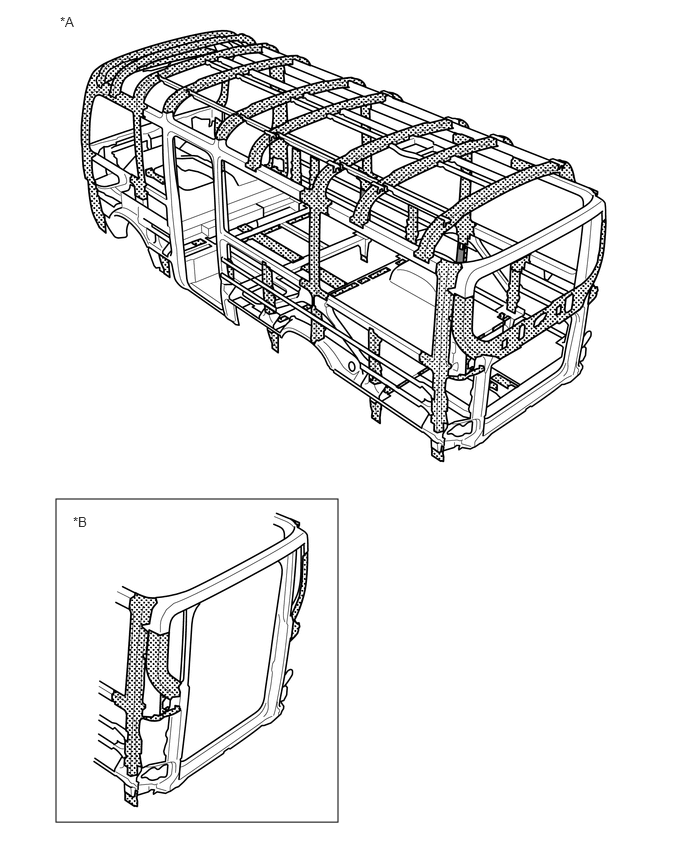
| *A | for Luggage Compartment | *B | for Double Swing Out Type |
|
0,0 0,0
false
|
590 MPa High Strength Steel |
0,0 0,0
false
|
440 MPa High Strength Steel |
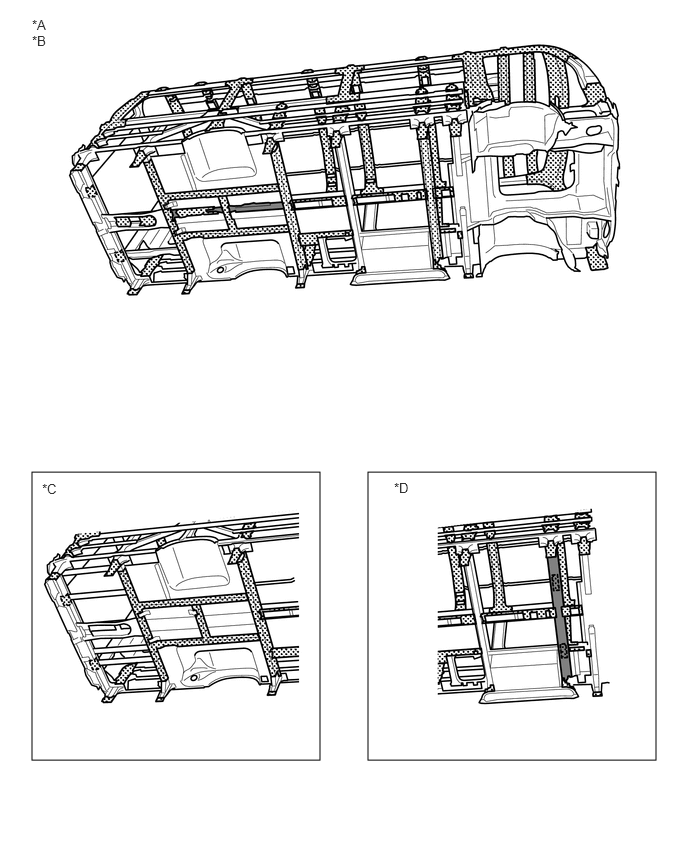
| *A | for Type A | *B | for 6AT |
| *C | for Type B | *D | exept 6AT |
|
0,0 0,0
false
|
590 MPa High Strength Steel |
0,0 0,0
false
|
440 MPa High Strength Steel |
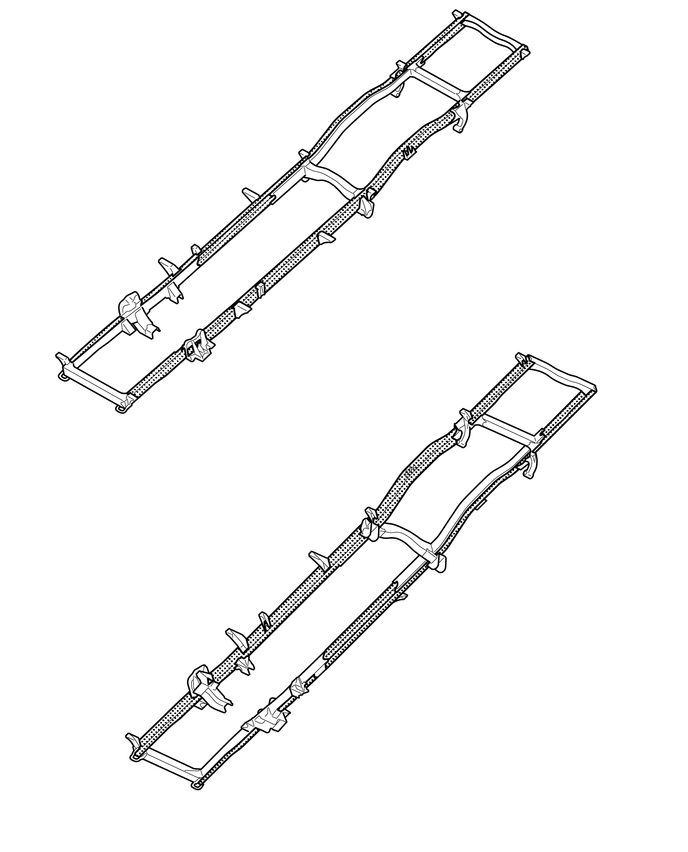
|
0,0 0,0
false
|
440 MPa High Strength Steel | - | - |
for Long Body
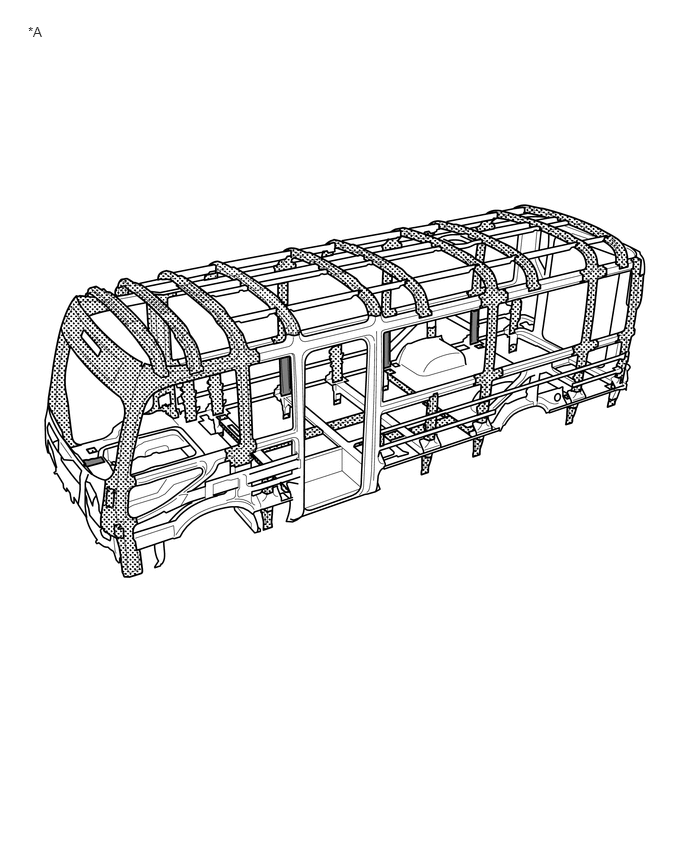
| *A | for Double Swing Out Type | - | - |
|
0,0 0,0
false
|
590 MPa High Strength Steel |
0,0 0,0
false
|
440 MPa High Strength Steel |
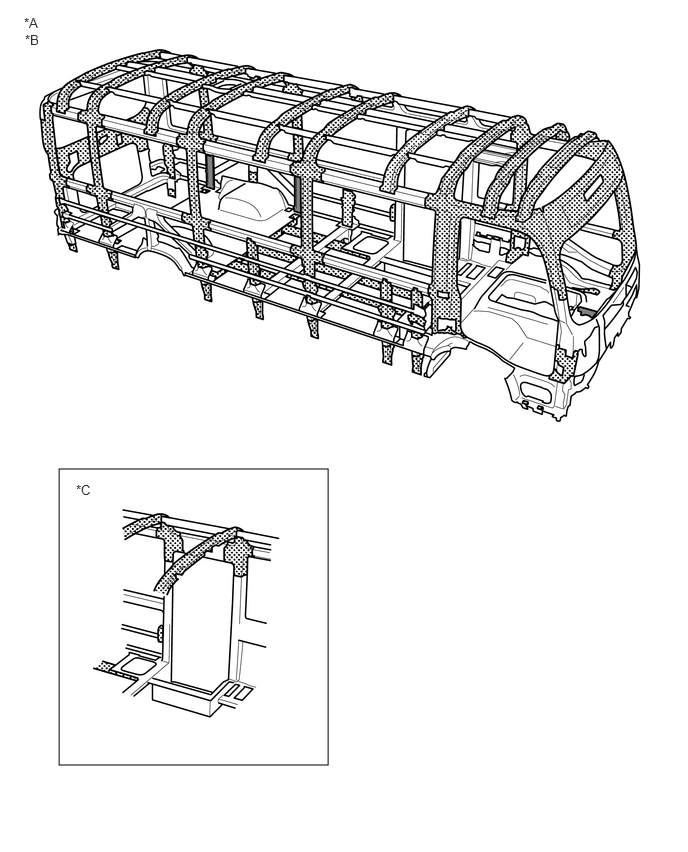
| *A | for Luggage Compartment | *B | for Glide Type |
| *C | for Folding Type | - | - |
|
0,0 0,0
false
|
590 MPa High Strength Steel |
0,0 0,0
false
|
440 MPa High Strength Steel |
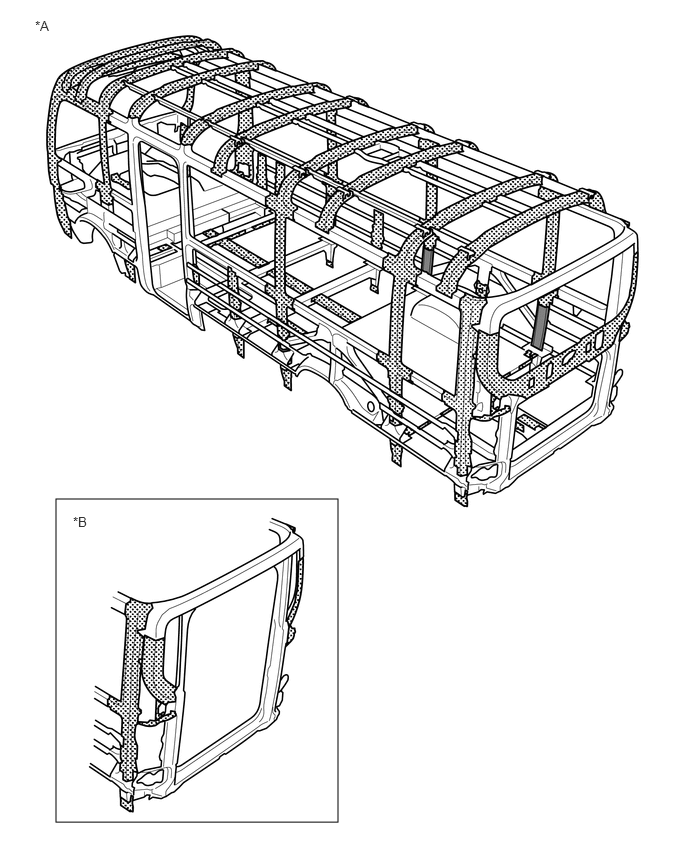
| *A | for Luggage Compartment | *B | for Double Swing Out Type |
|
0,0 0,0
false
|
590 MPa High Strength Steel |
0,0 0,0
false
|
440 MPa High Strength Steel |
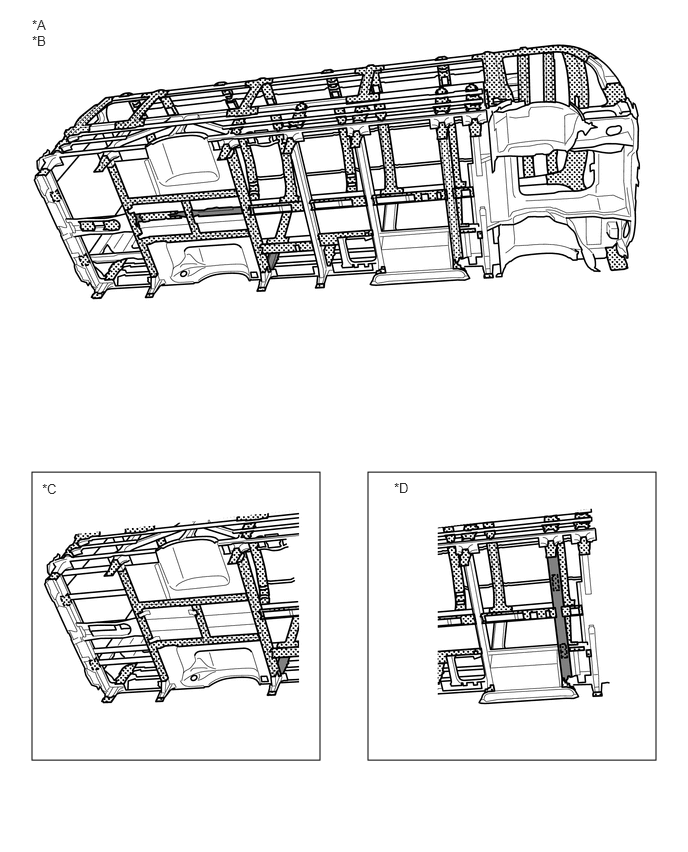
| *A | for Type A | *B | for 6AT |
| *C | for Type B | *D | exept 6AT |
|
0,0 0,0
false
|
590 MPa High Strength Steel |
0,0 0,0
false
|
440 MPa High Strength Steel |
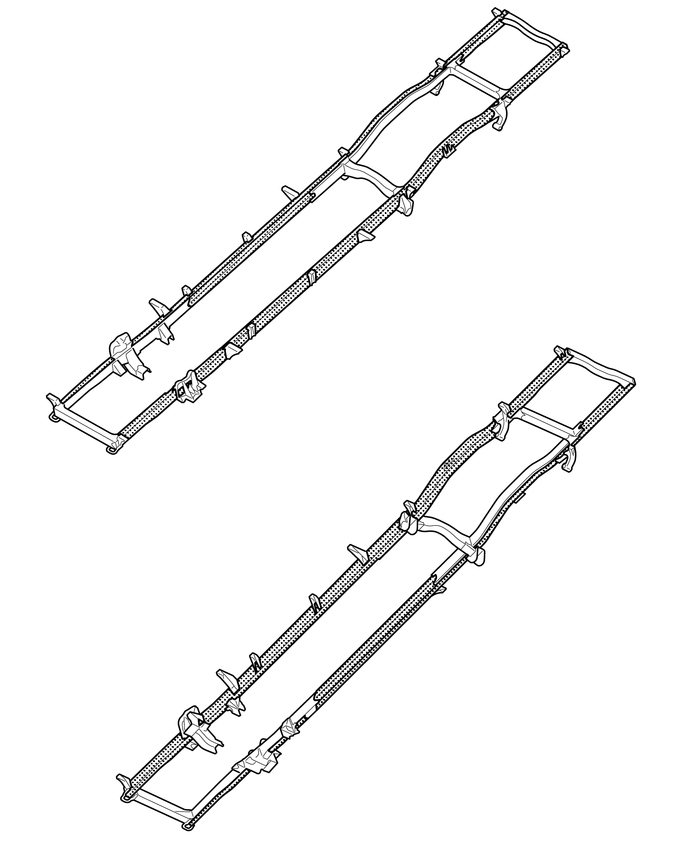
|
0,0 0,0
false
|
440 MPa High Strength Steel | - | - |
Adhesive Application Area
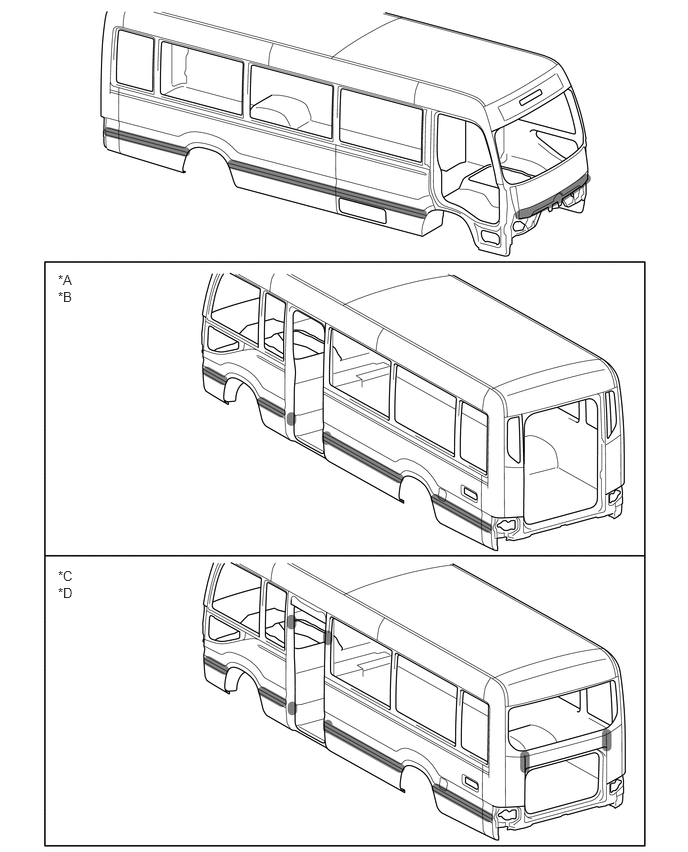
| *A | for Double Swing Out Type | *B | for Glide Type |
| *C | for Luggage Compartment | *D | for Folding Type |
|
0,0 0,0
false
|
Adhesive Application Areas | - | - |
Parts used for laser welding
Laser welding cross section
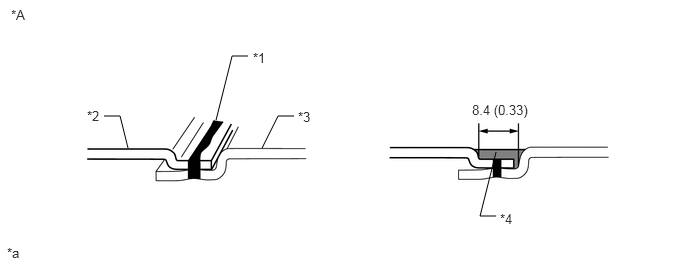
| *A | Laser welding cross section | - | - |
| *1 | Laser Welding | *2 | Upper Plate |
| *3 | Lower Plate | *4 | Body Sealer |
| *a | mm (in.) | - | - |
How to Use This Manual (Detailed information is recorded on the page for each panel)
| Replacement Panel | Removal | Installation |
|---|---|---|
| Upper Plate | The upper panel is removed in procedures 1 and 2 in order to leave the lower panel.
1.
Cut roughly before the joining points. 2.
Grind only the upper plate in the groove. |
1.
In order to avoid heat distortion, some parts are welded from inside the cabin. 2.
Set the plug hole diameter to 5.0 or 4.0. |
| Lower Plate | Cut before the joining points.
(If the joining points are damaged, also replace the adjacent panel) |
·
For long parts, perform "lap welding". ·
For short parts, perform "butt welding". |
| Note | The replacement panels are indicated in the repair manual. (Only a select portion of cut repairs are listed) Depending on the extent of the damage, if the cut repairs (lap welding or butt welding) are effective, perform the cut repairs as usual. | |
Laser welding parts
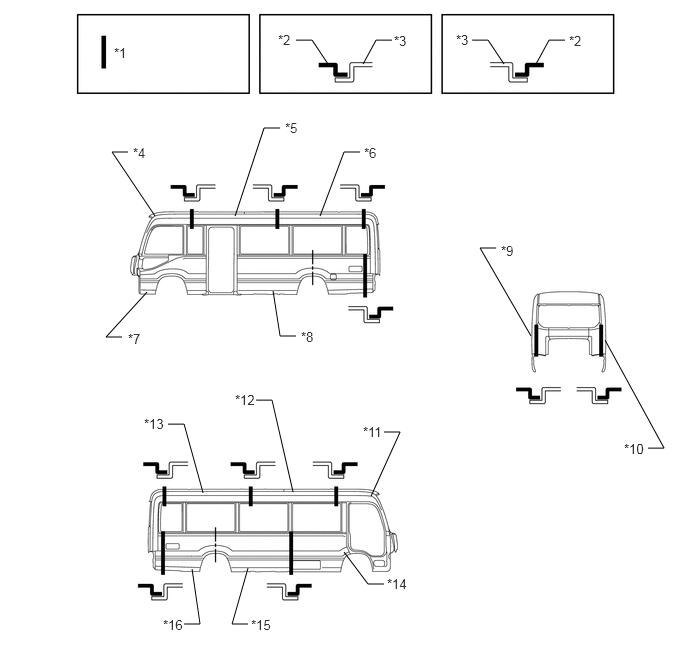
| *1 | Laser Welding | *2 | Upper Plate |
| *3 | Lower Plate | *4 | ROOF PANEL NO.4 LH |
| *5 | ROOF PANEL NO.5 LH | *6 | ROOF PANEL NO.6 LH |
| *7 | SIDE PANEL NO.1 LH | *8 | SIDE PANEL NO.2 LH |
| *9 | SIDE PANEL NO.4 LH | *10 | SIDE PANEL NO.4 RH |
| *11 | ROOF PANEL NO.4 RH | *12 | ROOF PANEL NO.5 RH |
| *13 | ROOF PANEL NO.6 RH | *14 | SIDE PANEL NO.1 RH |
| *15 | SIDE PANEL NO.2 RH | *16 | SIDE PANEL NO.3 RH |
Supply parts
Supply parts without joining parts (single panels).
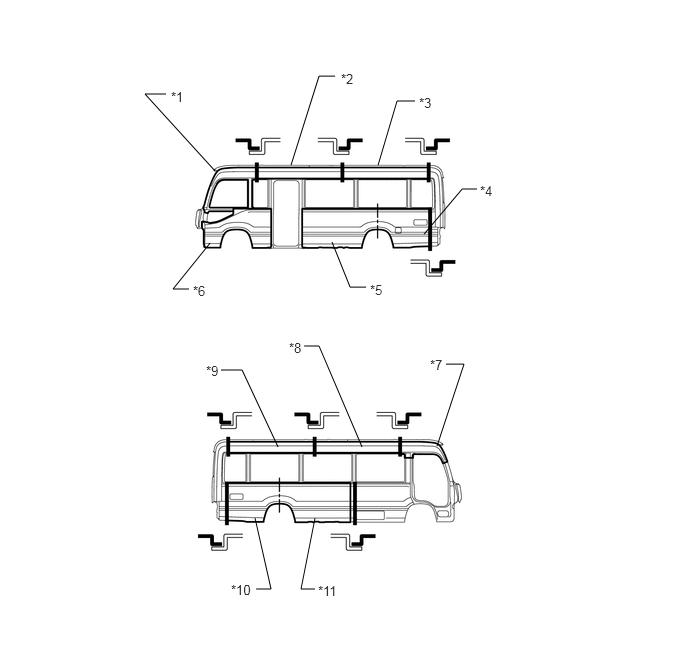
| *1 | ROOF PANEL NO.4 LH | *2 | ROOF PANEL NO.5 LH |
| *3 | ROOF PANEL NO.6 LH | *4 | SIDE PANEL NO.3 LH |
| *5 | SIDE PANEL NO.2 LH | *6 | SIDE PANEL NO.1 LH |
| *7 | ROOF PANEL NO.4 RH | *8 | ROOF PANEL NO.5 RH |
| *9 | ROOF PANEL NO.6 RH | *10 | SIDE PANEL NO.3 RH |
| *11 | SIDE PANEL NO.2 RH (*a) | - | - |
*a: SIDE PANEL NO.2 Cut before the laser joining points.
Supply parts with joining parts (single panels).
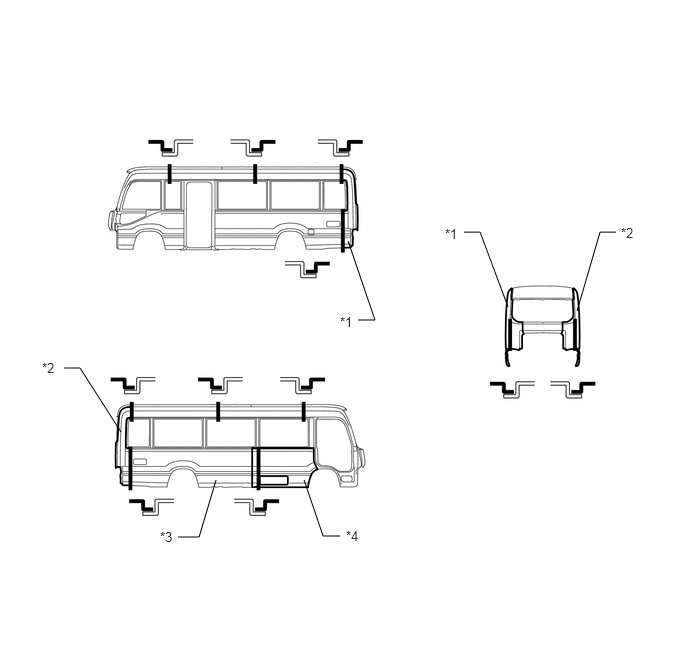
| *1 | SIDE PANEL NO.4 LH (*a) | *2 | SIDE PANEL NO.4 RH (*a) |
| *3 | SIDE PANEL NO.2 RH | *4 | SIDE PANEL NO.1 RH (*b) |
*a: SIDE PANEL NO.4 Reinstall the laser-joined panel
*b: SIDE PANEL NO.1 Reinstall the panel with a portion of the No. 2 side panel joined (laser or spot welded) to No. 1 side panel