N04C-VL ENGINE MECHANICAL CYLINDER HEAD REPLACEMENT
PROCEDURE

 11131
1.REMOVE INTAKE VALVE SEAT
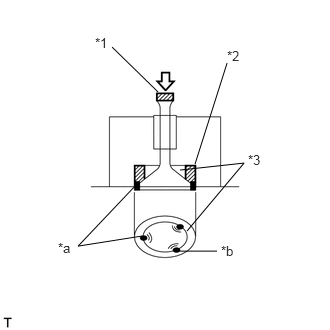
Grind the 3 places on the circumference of a used valve and weld it to the valve seat as shown in the illustration.
| *1 | Brass Block |
| *2 | Valve Seat |
| *3 | Valve |
| *a | Electric Welding Applied |
| *b | Grind these Points with Grinder |
- NOTICE:
-
To protect the lower surface of the cylinder head from welding spatters, be sure to apply grease before welding.
Place a brass block on the top of the valve stem and strike it with a hammer to remove the valve seat.
- CAUTION:
-
When striking, the valve tips may break off on impact. Wear safety glasses to protect your eyes.
11135
2.REMOVE EXHAUST VALVE SEAT
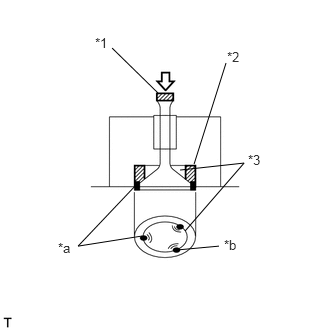
Grind 3 places on the circumference of a used valve and weld it to the valve seat as shown in the illustration.
| *1 | Brass Block |
| *2 | Valve Seat |
| *3 | Valve |
| *a | Electric Welding Applied |
| *b | Grind these Points with Grinder |
- NOTICE:
-
To protect the lower surface of the cylinder head from welding spatters, be sure to apply grease before welding.
Place a brass block on the top of the valve stem and strike it with a hammer to remove the valve seat.
- CAUTION:
-
When striking, the valve tips may break off on impact. Wear safety glasses to protect your eyes.
11176
3.REMOVE INJECTION NOZZLE SEAT
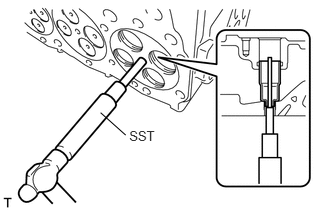
Using SST, remove the injection nozzle seat.
- SST
- 09201-10000 (09201-01050)
09950-70010 (09951-07100)
Remove the O-ring from the cylinder head sub-assembly.
11122
4.REMOVE INTAKE VALVE GUIDE BUSH
Heat the cylinder head up to between 80 and 100°C (176 to 212 °F).
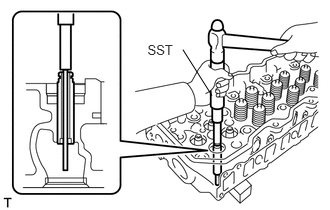
Using SST and a hammer, tap out the valve guide bush.
- SST
- 09201-10000 (09201-01070)
09950-70010 (09951-07100)
11126
5.REMOVE EXHAUST VALVE GUIDE BUSH
Heat the cylinder head up to between 80 and 100°C (176 to 212 °F).
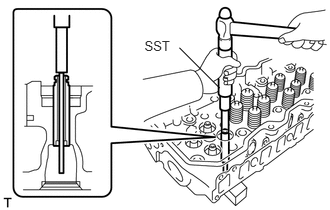
Using SST and a hammer, tap out the valve guide bush.
- SST
- 09201-10000 (09201-01070)
09950-70010 (09951-07100)
11122
6.INSTALL INTAKE VALVE GUIDE BUSH
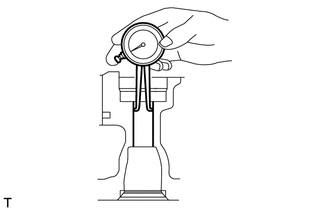
Using a caliper gauge, measure the inside diameter of the guide bush hole.
- Bush Hole Inside Diameter:
13.000 to 13.018 mm (0.5118 to 0.5125 in.)
- HINT:
-
If the inside diameter of the cylinder head is greater than the maximum, replace the cylinder head.
Heat the cylinder head up to between 80 and 100°C (176 to 212 °F).
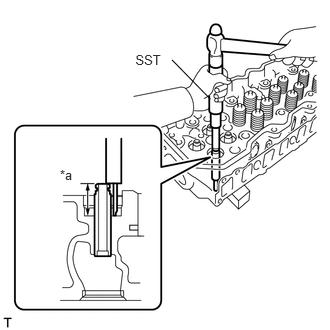
Using SST, tap in a new valve guide bush to the specified protrusion height.
- SST
- 09201-10000 (09201-01070)
09950-70010 (09951-07100)
- Protrusion Height:
26.4 to 26.8 mm (1.039 to 1.055 in.)
| *a | Protrusion Height |
- NOTICE:
-
Do not tap in the guide bush too much.
Using a reamer, ream the inside of the valve guide bush to the specified oil clearance between the valve guide bush and valve stem.
- Standard Oil Clearance:
0.028 to 0.058 mm (0.00110 to 0.00228 in.)
11126
7.INSTALL EXHAUST VALVE GUIDE BUSH
Using a caliper gauge, measure the inside diameter of the guide bush hole.
- Bush Hole Inside Diameter:
13.000 to 13.018 mm (0.5118 to 0.5125 in.)
- HINT:
-
If the inside diameter of the cylinder head is greater than the maximum, replace the cylinder head.
Heat the cylinder head up to between 80 and 100°C (176 to 212 °F).
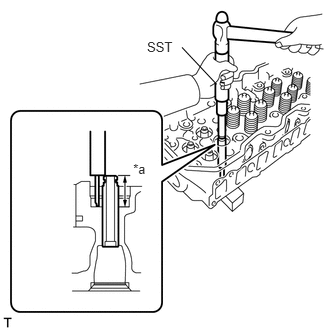
Using SST, tap in a new valve guide bush to the specified protrusion height.
- SST
- 09201-10000 (09201-01070)
09950-70010 (09951-07100)
- Protrusion Height:
26.4 to 26.8 mm (1.039 to 1.055 in.)
| *a | Protrusion Height |
- NOTICE:
-
Do not tap in the guide bush too much.
Using a reamer, ream the inside of the valve guide bush to the specified oil clearance between the valve guide bush and valve stem.
- Standard oil clearance:
0.053 to 0.083 mm (0.00209 to 0.00327 in.)
11176
8.INSTALL INJECTION NOZZLE SEAT
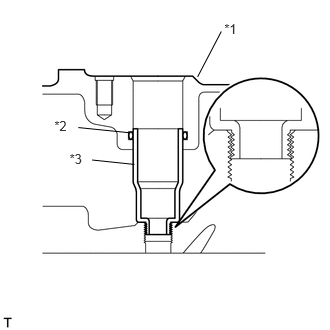
Apply a light coat of engine oil to a new O-ring, and install it into the cylinder head.
| *1 | Cylinder Head |
| *2 | O-ring |
| *3 | Injection Nozzle Seat |
- NOTICE:
-
Do not reuse the O-ring, as it may cause water or gas leakage inside the cylinder and the cylinder head may overheat or crack.
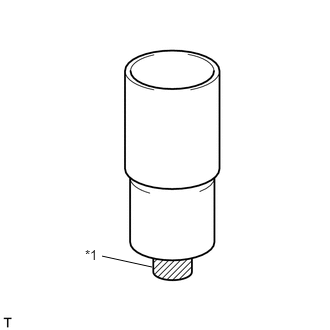
Apply seal packing to a new injection nozzle seat.
- Seal packing:
Three Bond 1211,1215 or equivalent
| *1 | Seal Packing |
- NOTICE:
- ·
Remove any oil from the installation surface of the cylinder head and injection nozzle seat.
·Do not reuse the injection nozzle seat, as it may cause water or gas leakage inside the cylinder and the cylinder may overheat or crack.
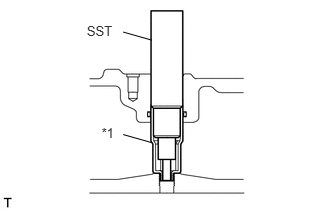
Using SST, install the injection nozzle seat into the cylinder head.
- SST
- 09260-69015 (09268-06020)
| *1 | Injection Nozzle Seat |
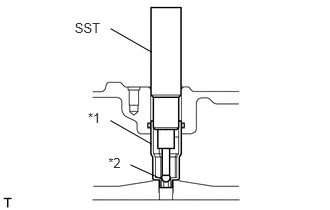
Using SST, stake the injection nozzle seat.
- SST
- 09260-69015 (09268-06010, 09268-06020)
| *1 | Injection Nozzle Seat |
| *2 | SST (Steel Ball) |
- NOTICE:
-
Put a container under the cylinder head to prevent the steel ball from being lost.
11131
9.INSTALL INTAKE VALVE SEAT
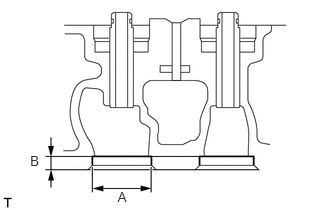
Using a caliper gauge and vernier caliper, measure the dimensions of the valve seat installation hole.
- Cylinder Head Dimension:
- A:
36.000 to 36.016 mm (1.4173 to 1.4179 in.)
- B:
8.4 to 8.6 mm (0.3307 to 0.3386 in.)
If either result is not as specified, replace the cylinder head.
Heat the cylinder head up to between 80 and 100°C (176 to 212 °F).
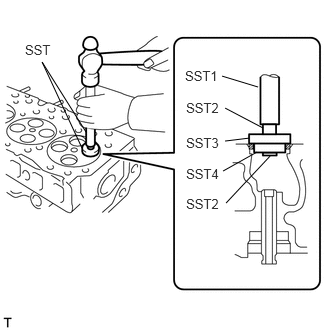
Using SST and a hammer, lightly tap the valve seat into the cylinder head.
- SST
- 09950-60011 (09951-00300, 09951-00360, 09952-06010)
09950-70010 (09951-07100)
| SST 1 | 09951-07100 |
| SST 2 | 09952-06010 |
| SST 3 | 09951-00360 |
| SST 4 | 09951-00300 |
Using SST and a hammer, completely tap in the valve seat.
- SST
- 09950-60011 (09951-00300, 09951-00360, 09952-06010)
09950-70010 (09951-07100)
11135
10.INSTALL EXHAUST VALVE SEAT
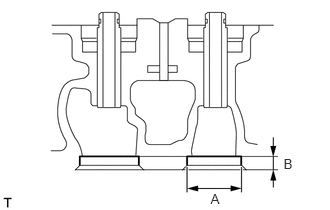
Using a caliper gauge and vernier caliper, measure the dimensions of the valve seat installation hole.
- Cylinder Head Dimension:
- A:
32.000 to 32.016 mm (1.2598 to 1.2605 in.)
- B:
7.6 to 7.8 mm (0.2992 to 0.3071 in.)
If either result is not as specified, replace the cylinder head.
Heat the cylinder head up to between 80 and 100°C (176 to 212 °F).
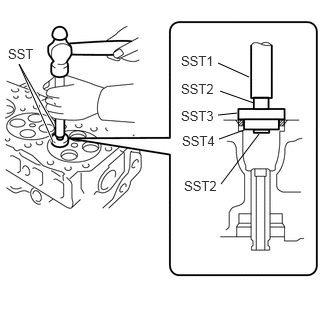
Using SST and a hammer, lightly tap the valve seat into the cylinder head.
- SST
- 09950-60011 (09951-00250, 09951-00320, 09952-06010)
09950-70010 (09951-07100)
| SST 1 | 09951-07100 |
| SST 2 | 09952-06010 |
| SST 3 | 09951-00320 |
| SST 4 | 09951-00250 |
Using SST and a hammer, completely tap in the valve seat.
- SST
- 09950-70010 (09951-07100)
09950-60011 (09951-00250, 09951-00320, 09952-06010)