14B ENGINE MECHANICAL CYLINDER BLOCK CYLINDER BLOCK INSPECTION
PROCEDURE

 1.CLEAN CYLINDER BLOCK
Remove gasket material
Using a gasket scraper, remove all the gasket material from the top surface of the cylinder block.
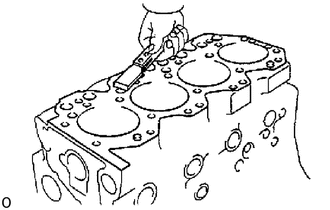
Clean cylinder block
Using a soft brush and solvent, thoroughly clean the cylinder block.
2.INSPECT TOP SURFACE OF CYLINDER BLOCK FOR FLATNESS
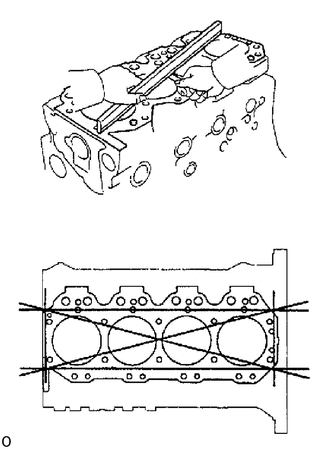
Using a precision straight edge and feeler gauge, measure the surfaces contacting the cylinder head gasket for warpage.
- Maximum warpage:
0.20 mm (0.0079 in.)
If warpage is greater than maximum, replace the cylinder block.
3.INSPECT CYLINDER FOR VERTICAL SCRATCHES
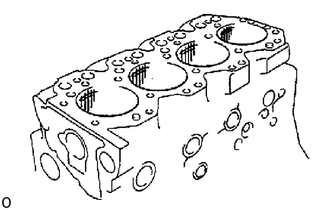
Visually check the cylinder for vertical scratches.
If deep scratches are present, rebore all the 4 cylinders. If necessary, replace the cylinder block.
4.INSPECT CYLINDER BORE DIAMETER
- HINT:
-
-
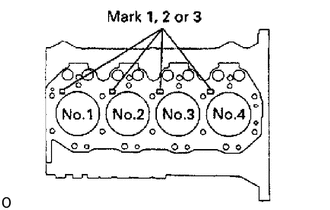
There are 3 sizes of the standard cylinder bore diameter, marked "1", "2" and "3" accordingly. The mark is stamped on the top of the cylinder block.
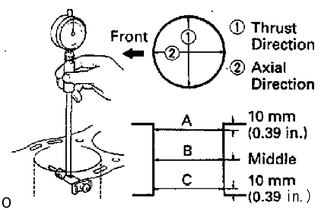
Using a cylinder gauge, measure the cylinder bore diameter at positions A, B and C in the thrust and axial directions.
- Standard diameter:
3B,14B STD Mark "1" 102.000 - 102.010 mm (4.0157 - 4.0161 in.) Mark "2 102.010 - 102.020 mm (4.0161 - 4.0165 in.) Mark "3" 102.020 - 102.030 mm (4.0165 - 4.0169 in.) O/S 0.50 102.500 - 102.530 mm (4.0354 - 4.0366 in.) O/S 0.75 102.750 - 102.780 mm (4.0453 - 4.0464 in.) O/S 1.00 103.000 - 103.030 mm (4.0551 - 4.0563 in.)
15B-F, 15B-FT STD Mark "1" 108.000 - 108.010 mm (4.2520 - 4.2524 in.) Mark "2 108.010 - 108.020 mm (4.2524 - 4.2528 in.) Mark "3" 108.020 - 108.030 mm (4.2528 - 4.2531 in.) O/S 0.50 108.500 - 108.530 mm (4.2717 - 4.2728 in.) O/S 0.75 108.750 - 106.780 mm (4.2815 - 4.2827 in.) O/S 1.00 109.000 - 109.030 mm (4.2913 - 4.2925 in.)
- Maximum diameter:
3B,14B STD 102.23 mm (4.0248 in.) O/S 0.50 102.73 mm (4.0445 in.) O/S 0.75 102.98 mm (4.0543 in.) O/S 1.00 103.23 mm (4.0642 in.)
15B-F, 15B-FT STD 108.23 mm (4.2610 in.) O/S 0.50 108.73 mm (4.2807 in.) O/S 0.75 108.98 mm (4.2906 in.) O/S 1.00 109.23 mm (4.3004 in.)
If the diameter is greater than maximum, re bore all the 4 cylinders. If necessary, replace the cylinder block.
5.REMOVE CYLINDER RIDGE
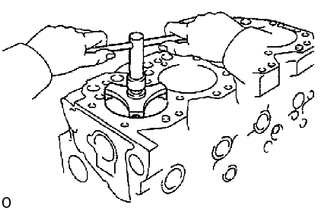
If the wear is less than 0.2 mm (0.008 in.), using a ridge reamer, grind the top of the cylinder.