RM2850E
_51
Engine / Hybrid System
_073170
14B ENGINE MECHANICAL
_0356054
CYLINDER BLOCK
A
14B ENGINE MECHANICAL CYLINDER BLOCK CYLINDER BORING
CAUTION / NOTICE / HINT
- HINT:
- ·
Bore all the 4 cylinders to the oversized piston outside diameter.
·Replace all the piston rings with ones to match the oversized pistons.
PROCEDURE

 1.KEEP OVERSIZED PISTONS
- Oversized piston diameter:
3B O/S 0.50 102.300 - 102.330 mm (4.0278 - 4.0287 in.) O/S 0.75 102.550 - 102.580 mm (4.0372 - 4.0386 in.) O/S 1.00 102.800 - 102.830 mm (4.0472 - 4.0484 in.)
14B O/S 0.50 102.260 - 102.290 mm (4.0260 - 4.0272 in.) O/S 0.75 102.510 - 102.540 mm (4.0358 - 4.0370 in.) O/S 1.00 102.760 - 102.790 mm (4.0457 - 4.0466 in.)
15B-F O/S 0.50 108.330 - 108.360 mm (4.2650 - 4.2661 in.) O/S 0.75 108.580 - 108.610 mm (4.2748 - 4.2760 in.) O/S 1.00 108.830 - 108.860 mm (4.2846 - 4.2858 in.)
15B-FT O/S 0.50 108.320 - 108.350 mm (4.2846 - 4.2657 in.) O/S 0.75 108.570 - 108.600 mm (4.2744 - 4.2756 in.) O/S 1.00 108.820 - 108.850 mm (4.2843 - 4.2854 in.)
2. CALCULATE AMOUNT TO BORE CYLINDERS
a.
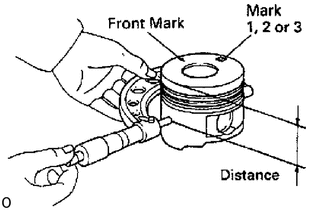
Using a micrometer, measure the piston diameter at right angles to the piston pin center line, the indicated distance from the piston head.
- Distance:
3B 45.20 mm (1.7795 in.) 14B 42.83 mm (1.6862 in.) 15B-F, 15B-FT 50.55 mm (1.9902 in.)
b.
Calculate the amount each cylinder is to be rebored as follows:
Size to be rebored = P + C - H
P = Piston diameter
C = Piston clearance
| 3B | 0.190 - 0.210 mm (0.0057 - 0.0065 in.) |
| 14B | 0.230 - 0.250 mm (0.0091 - 0.0098 in.) |
| 15B-F | 0.160 - 0.180 mm (0.0063 - 0.0071 in.) |
| 15B-FT | 0.170 - 0.190 mm (0.0067 - 0.0075 in.) |
H = Allowance for honing
0.02 mm (0.0008 in.) or less
3. BORE AND HONE CYLINDER TO CALCULATED DIMENSIONS
- Maximum honing:
0.02 mm (0.0008 in.)
- NOTICE:
-
Excess honing will destroy the finished roundness.