BM3250E
_01
Vehicle Exterior
_040520
BODY WELD POINT
_0187901
FRAME REAR CROSSMEMBER
F
BODY WELD POINT FRAME REAR CROSSMEMBER ASSEMBLY REPLACEMENT
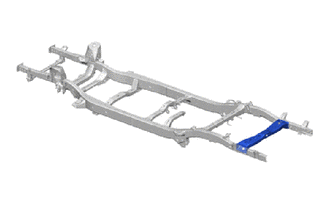
With the spring bracket assembly and exhaust pipe support assembly removed.
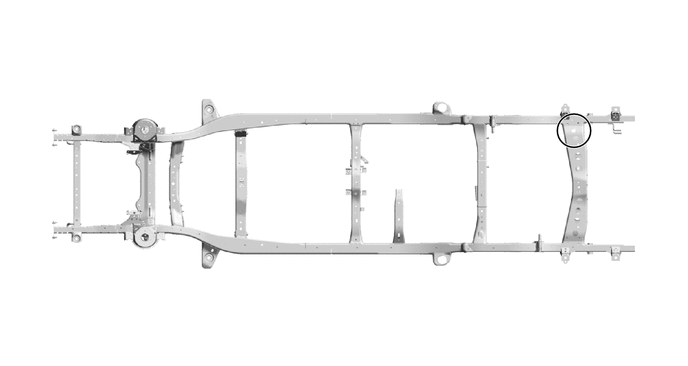
- HINT:
- ·
Use the same procedure for the RH side and LH side.
·The procedure listed below is for the RH side.
REMOVAL
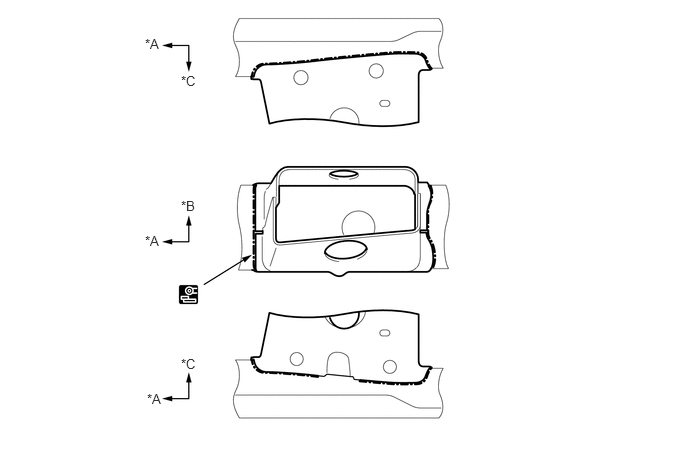
| Symbol Meaning | |
|---|---|

|
Cut with Disc Sander etc. |
1.531,4.073 1.844,4.229
0.313,0.156
10
false
*A
1.51,2.427 1.823,2.583
0.313,0.156
10
false
*A
1.885,3.708 2.198,3.865
0.313,0.156
10
false
*C
1.51,0.375 1.823,0.531
0.313,0.156
10
false
*A
1.885,2.063 2.198,2.219
0.313,0.156
10
false
*B
1.885,0.76 2.198,0.917
0.313,0.156
10
false
*C
| *A | FRONT | *B | UPPER |
| *C | LH | - | - |
INSTALLATION
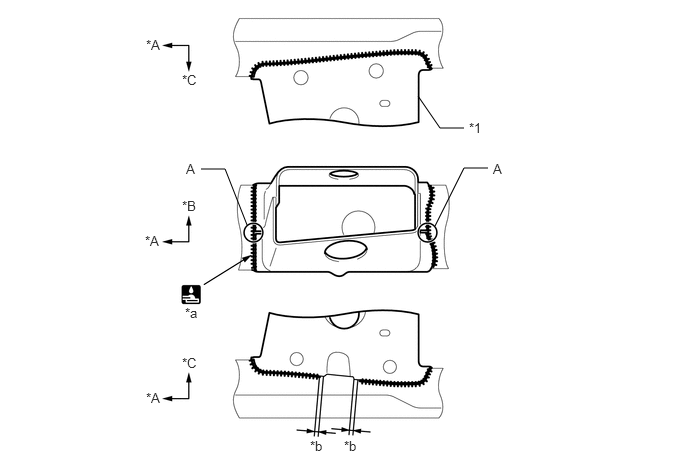
| Symbol Meaning | |
|---|---|

|
Fillet Weld |
a.
Make sure that proper welding can be performed by setting up the welding conditions as necessary before performing work.
b.
To prevent heat deformation, weld the right and left side of each part before continuing to the next part.
c.
Make sure that the welding bead at A is overlapped.
4.833,1.333 4.583,1.333
4.583,1.333 4.354,1
false
5.083,1.75 4.833,1.75
4.833,1.75 4.531,2.354
false
2.573,2.344 2.344,1.76
2.344,1.76 2.094,1.76
false
1.521,4.063 1.833,4.219
0.313,0.156
10
false
*A
1.51,2.427 1.823,2.583
0.313,0.156
10
false
*A
1.896,3.698 2.208,3.854
0.313,0.156
10
false
*C
3.583,4.563 3.896,4.719
0.313,0.156
10
false
*b
1.521,0.385 1.833,0.542
0.313,0.156
10
false
*A
1.896,2.063 2.208,2.219
0.313,0.156
10
false
*B
1.896,0.75 2.208,0.906
0.313,0.156
10
false
*C
4.885,1.25 5.198,1.406
0.313,0.156
10
false
*1
1.927,3.177 2.24,3.333
0.313,0.156
10
false
*a
3.229,4.563 3.542,4.719
0.313,0.156
10
false
*b
1.938,1.677 2.188,1.917
0.25,0.24
10
false
A
5.135,1.677 5.333,1.927
0.198,0.25
10
false
A
| *A | FRONT | *B | UPPER |
| *C | LH | - | - |
| *1 | FRAME CROSSMEMBER SUB-ASSEMBLY REAR | - | - |
| *a | 589 mm (23.19 in.) | *b | 5 +/- 5 mm (0.20 +/- 0.20 in.) |
d.
After applying the top coat, apply anti-rust agent to the internal panel portion of the closed section structural weld points.