5L-E ENGINE MECHANICAL CYLINDER BLOCK INSPECTION
PROCEDURE

 11448
1.INSPECT CYLINDER BLOCK OIL ORIFICE
Check the cylinder block oil orifice for damage or clogging.
If necessary, replace the cylinder block oil orifice.
15605
2.INSPECT OIL CHECK VALVE SUB-ASSEMBLY
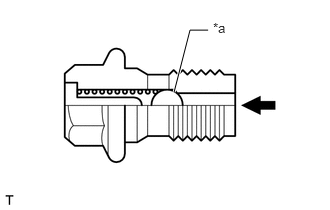
| *a | Ball |

|
Push |
Push the ball of the oil check valve sub-assembly with a wooden stick to check if it is stuck.
If the ball of the oil check valve sub-assembly is stuck, replace the oil check valve sub-assembly.
15708
3.INSPECT NO. 1 OIL NOZZLE SUB-ASSEMBLY
Check the No. 1 oil nozzle sub-assembly for damage or clogging.
If necessary, replace the No. 1 oil nozzle sub-assembly.
11401
4.CLEAN CYLINDER BLOCK SUB-ASSEMBLY
Using a gasket scraper, remove all the gasket material from the top surface of the cylinder block sub-assembly.
Using a soft brush and solvent, thoroughly clean the cylinder block sub-assembly.
11401
5.INSPECT CYLINDER BLOCK SUB-ASSEMBLY
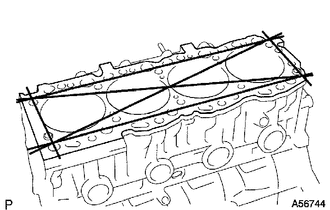
Using a precision straightedge and feeler gauge, measure the surface of the cylinder block sub-assembly that contacts the cylinder head sub-assembly for warpage.
- Maximum warpage:
0.2 mm (0.00787 in.)
If the warpage is more than the maximum, replace the cylinder block sub-assembly.
Visually check the cylinders for vertical scratches.
If deep scratches are present, rebore all 4 cylinders. If necessary, replace the cylinder block sub-assembly.
6.INSPECT CYLINDER BORE
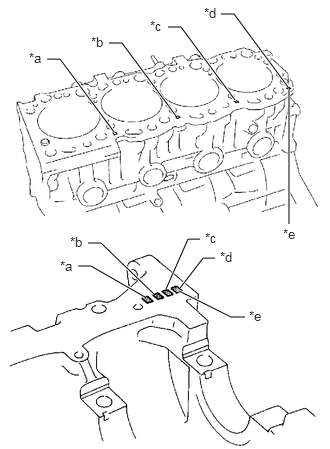
| *a | No. 1 |
| *b | No. 2 |
| *c | No. 3 |
| *d | No. 4 |
| *e | Mark 1, 2 or 3 |
Inspect the cylinder bore diameter.
- HINT:
-
There are 3 sizes of the standard cylinder bore diameter, marked "1", "2" and "3" accordingly. The mark is stamped on the lower left rear of the cylinder block.
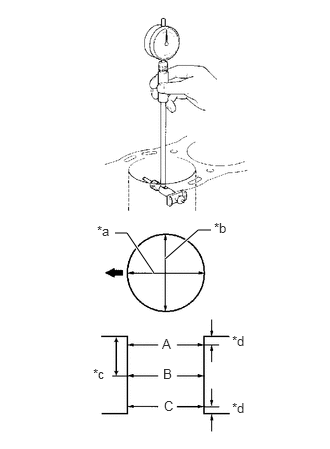
| *a | Axial Direction |
| *b | Thrust Direction |
| *c | Center |
| *d | 10 mm (0.394 in.) |
|
|
Front |
Using a cylinder gauge, measure the cylinder bore diameter at positions A, B and C in the thrust and axial directions.
- Standard Diameter:
Item Specified Condition Mark 1 99.50 to 99.51 mm (3.9173 to 3.9177 in.) Mark 2 99.51 to 99.52 mm (3.9177 to 3.9181 in.) Mark 3 99.52 to 99.53 mm (3.9181 to 3.9185 in.)
- Maximum Diameter:
Item Specified Condition STD 99.73 mm (3.93 in.) O/S 0.50 100.23 mm (3.95 in.)
If the diameter is more than the maximum, rebore all 4 cylinders. If necessary, replace the cylinder block sub-assembly.
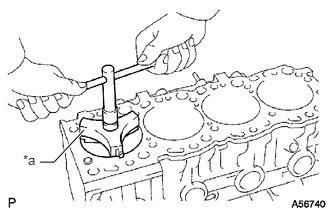
| *a | Ridge Reamer |
Inspect the cylinder ridge.
If the wear is less than 0.2 mm (0.00787 in.), using a ridge reamer, grind the top of the cylinder.
13101
7.CLEAN PISTON
Using a gasket scraper, remove the carbon from the piston top.
Using a groove cleaning tool or broken ring, clean the piston ring grooves.
Using solvent and a brush, thoroughly clean the piston.
- NOTICE:
-
Do not use a wire brush.
13101
8.INSPECT PISTON WITH PIN SUB-ASSEMBLY
- HINT:
-
When replacing the piston sub-assembly (w/ pin) with a supply part, there are a number of piston diameter sizes to choose from, but there is only one size of piston pin diameter.
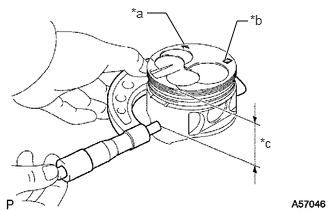
| *a | Front Mark |
| *b | Size Mark |
| *c | Distance |
Using a micrometer, measure the piston diameter at right angles to the piston center line where the distance from the piston head is as specified.
- Distance:
61.27 to 61.33 mm (2.41 to 2.42 in.)
- Standard Piston Diameter:
Item Specified Condition Mark 1 99.45 to 99.46 mm (3.9153 to 3.9157 in.) Mark 2 99.46 to 99.47 mm (3.9157 to 3.9161 in.) Mark 3 99.47 to 99.48 mm (3.9161 to 3.9165 in.) O/S 0.50 99.95 to 99.98 mm (3.935 to 3.936 in.)
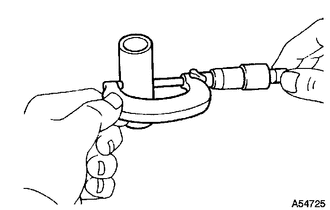
Using a micrometer, measure the piston pin diameter.
- Standard Piston Pin Diameter:
Item Specified Condition Mark A 29.000 to 29.004 mm (1.1417 to 1.1419 in.) Mark B 29.004 to 29.008 mm (1.1419 to 1.1420 in.) Mark C 29.008 to 29.012 mm (1.1420 to 1.1422 in.)
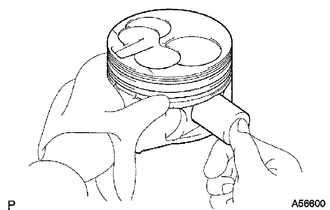
Inspect the piston pin fit.
At 60°C (140°F), check that the piston pin can be pushed into the piston pin hole with your thumb.
If the pin can be installed at a lower temperature, replace the piston with pin sub-assembly.
9.INSPECT PISTON OIL CLEARANCE
Measure the cylinder bore diameter in the thrust direction.
Subtract the piston diameter measurement from the cylinder bore diameter measurement.
- Standard oil clearance:
0.04 to 0.06 mm (0.00157 to 0.00236 in.)
- Maximum oil clearance:
0.13 mm (0.00512 in.)
If the oil clearance is more than the maximum, replace all the piston with pin sub-assemblies. If necessary, replace the cylinder block sub-assembly.
10.INSPECT RING GROOVE CLEARANCE
Using a feeler gauge, measure the clearance between a new piston ring and the wall of the ring groove.
- Standard Groove Clearance:
Item Specified Condition No. 1 piston ring 0.057 to 0.101 mm (0.00224 to 0.00398 in.) No. 2 piston ring 0.06 to 0.10 mm (0.00236 to 0.00394 in.) Oil ring 0.03 to 0.07 mm (0.00118 to 0.00276 in.)
- Maximum groove clearance:
0.2 mm (0.00787 in.)
If the clearance is more than the maximum, replace the piston.
11.INSPECT PISTON RING END GAP
Insert the piston ring into the cylinder bore.
Using a piston, push the piston ring a little beyond the bottom of the ring travel, 140 mm (5.15 in.) from the top of the cylinder block.
Using a feeler gauge, measure the end gap.
- Standard End Gap:
Item Specified Condition No. 1 piston ring 0.35 to 0.47 mm (0.0138 to 0.0185 in.) No. 2 piston ring 0.47 to 0.60 mm (0.0185 to 0.0236 in.) Oil ring 0.2 to 0.4 mm (0.00787 to 0.0157 in.)
- Maximum End Gap:
Item Specified Condition No. 1 piston ring 1.29 mm (0.0508 in.) No. 2 piston ring 1.42 mm (0.0559 in.) Oil ring 1.22 mm (0.0480 in.)
If the end gap is more than the maximum, replace the piston ring.
If the end gap is more than the maximum even with a new piston ring, rebore all 4 cylinders or replace the cylinder block sub-assembly.
12.INSPECT PISTON PIN OIL CLEARANCE
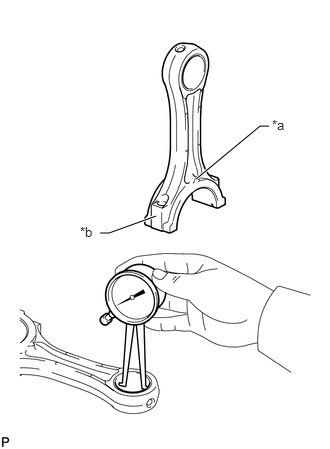
| *a | Front Mark |
| *b | Connecting Rod Bush Inside Diameter Mark A, B or C |
Using a caliper gauge, measure the inside diameter of the connecting rod bush.
- Standard Bush Inside Diameter:
Item Specified Condition Mark A 29.008 to 29.012 mm (1.1420 to 1.1422 in.) Mark B 29.012 to 29.016 mm (1.1422 to 1.1424 in.) Mark C 29.016 to 29.020 mm (1.1424 to 1.1425 in.)
Subtract the piston pin diameter measurement from the connecting rod bush inside diameter measurement.
- Standard oil clearance:
0.004 to 0.012 mm (0.000157 to 0.000472 in.)
- Maximum oil clearance:
0.05 mm (0.00197 in.)
If the oil clearance is more than the maximum, replace the connecting rod sub-assembly.
If necessary, replace the piston with pin sub-assembly.
13201
13.INSPECT CONNECTING ROD SUB-ASSEMBLY
Using a rod aligner and feeler gauge, check the connecting rod alignment.
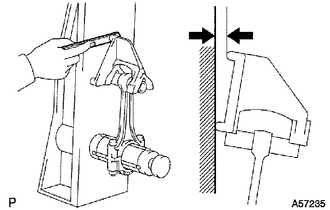
Check if the connecting rod sub-assembly is bent.
- Maximum bend:
0.05 mm (0.00196 in.) per 100 mm (3.94 in.)
If the bend is more than the maximum, replace the connecting rod sub-assembly.
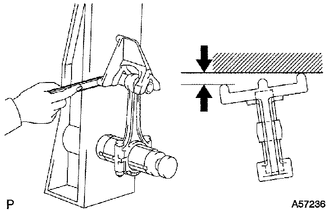
Check if the connecting rod sub-assembly is twisted.
- Maximum twist:
0.15 mm (0.00591 in.) per 100 mm (3.94 in.)
If the twist is more than the maximum, replace the connecting rod sub-assembly.
13265
14.INSPECT CONNECTING ROD BOLT
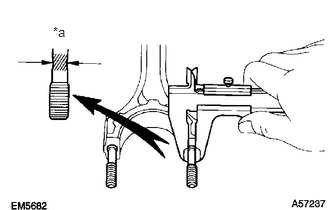
| *a | Compressed Bolt |
Using a vernier caliper, measure the diameter of the tension portion of the connecting rod bolt.
- Standard diameter:
8.4 to 8.6 mm (0.331 to 0.339 in.)
- Minimum diameter:
8.2 mm (0.323 in.)
If the diameter is less than the minimum, replace the connecting rod bolt.
13411
15.INSPECT CRANKSHAFT
Inspect for circle runout.
Place the crankshaft on V-blocks.
Using a dial indicator, measure the circle runout at the center journal.
- Maximum circle runout:
0.06 mm (0.00236 in.)
If the circle runout is more than the maximum, replace the crankshaft.
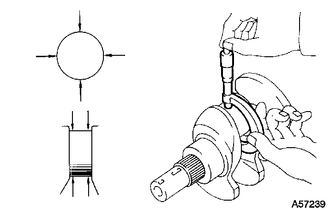
Inspect the main journals and crank pins.
Using a micrometer, measure the diameter of each main journal and crank pin.
- Standard main journal diameter:
61.985 to 62.000 mm (2.4403 to 2.4409 in.)
- Standard crank pin diameter:
54.988 to 55.000 mm (2.1649 to 2.1654 in.)
If the diameter is not as specified, check the connecting rod oil clearance (Click hereEngine / Hybrid System>5L-E ENGINE MECHANICAL>CYLINDER BLOCK>DISASSEMBLY) and crankshaft oil clearance (Click hereEngine / Hybrid System>5L-E ENGINE MECHANICAL>CYLINDER BLOCK>DISASSEMBLY). If necessary, grind or replace the crankshaft.
Check each main journal and crank pin for taper and out of round as shown in the illustration.
- Maximum taper and out of round:
0.02 mm (0.000787 in.)
If the taper and out of round is more than the maximum, replace the crankshaft.
If necessary, grind and hone the main journals and/or crank pins.
Grind and hone the main journals and/or crank pins to the finished undersized diameter.
Install new main journal and/or crankshaft pin undersized bearing.