2TR-FE ENGINE MECHANICAL CYLINDER BLOCK REPAIR
CAUTION / NOTICE / HINT
- HINT:
- ·
Bore all 4 cylinders to fit the O/S piston outside diameter.
·Replace all the piston rings with ones to match the O/S pistons.
PROCEDURE

 1.BORE CYLINDER
Prepare 4 new O/S pistons.
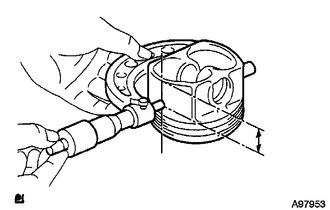
| *1 | Distance |
Using a micrometer, measure the piston diameter at right angles to the piston center line where the distance from the piston end is as specified.
- Standard piston diameter (O/S 0.50):
95.440 to 95.450 mm (3.7575 to 3.7579 in.)
- Distance:
13.8 mm (0.543 in.)
Calculate the amount each cylinder is to be rebored as follows.
- HINT:
Size to be rebored = P + C - H
P = Piston diameter
C = Piston oil clearance: 0.019 to 0.052 mm (0.000748 to 0.00205 in.)
H = Allowance for honing: 0.02 mm (0.000787 in.) or less
Bore and hone the cylinders to the calculated dimensions.
- NOTICE:
-
Excess honing will destroy the finished roundness.
Using a cylinder gauge, measure the cylinder bore diameter and calculate the honing allowance.
- HINT:
-
Honing allowance = cylinder bore diameter - (piston diameter + oil clearance)
Finish the cylinder bore using the calculated value.
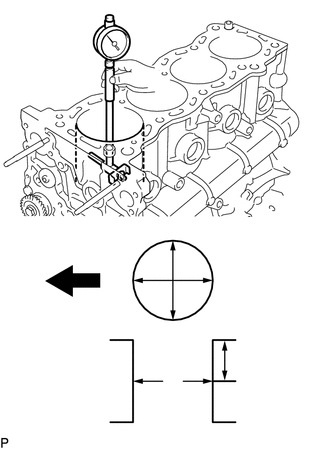
| *1 | Thrust Direction |
| *2 | Axial Direction |

|
Front |
Using a cylinder gauge, measure the cylinder bore diameter.
- Standard oil clearance:
0.019 to 0.052 mm (0.000748 to 0.00205 in.)