AXLE AND DIFFERENTIAL REAR DIFFERENTIAL CARRIER ASSEMBLY(w/o Differential Lock) REASSEMBLY
PROCEDURE

 1.ASSEMBLE DIFFERENTIAL CASE
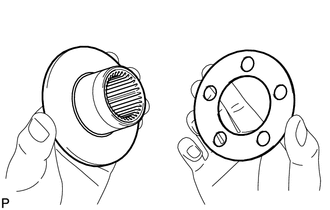
Install the rear differential side gear thrust washer to the rear differential side gear.
Install the rear differential pinion thrust washer and rear differential pinion to the rear differential spider.
Fix the differential case RH in place.
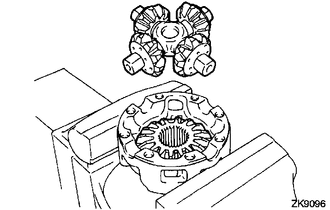
Install the rear differential side gear and rear differential spider to the differential case RH.
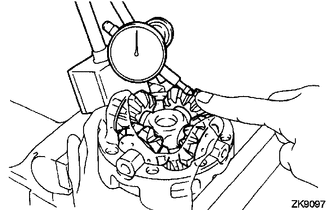
Using a dial indicator, measure the differential case RH side backlash while pushing the pinion toward the case.
- Standard backlash:
0.05 to 0.20 mm (0.00197 to 0.00787 in.)
Remove the rear differential spider from the differential case RH.
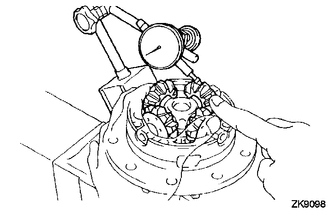
Install the rear differential side gear and rear differential spider to the differential case LH.
Using a dial indicator, measure the differential case LH side backlash while pushing the pinion toward the case.
- Standard backlash:
0.05 to 0.20 mm (0.00197 to 0.00787 in.)
If the backlash is not within the specification, install 2 side gear thrust washers of a different thickness.
- Standard Thrust Washer:
Thickness Thickness 0.87 to 0.93 mm (0.0343 to 0.0366 in.) 1.17 to 1.23 mm (0.0461 to 0.0484 in.) 0.97 to 1.03 mm (0.0382 to 0.0406 in.) 1.27 to 1.33 mm (0.0500 to 0.0524 in.) 1.07 to 1.13 mm (0.0421 to 0.0445 in.) -
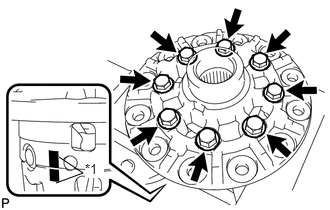
Align the matchmarks and assemble the differential case from the RH and LH cases.
| *a | Matchmark |
Using a plastic-faced hammer, install the differential case.
Install the 8 bolts.
- Torque:
- 47 N*m (480 kgf*cm, 35 ft.*lbf)
2.INSTALL DIFFERENTIAL RING GEAR
Clean the contact surfaces of the differential case and ring gear.
Heat the ring gear in water that is approximately 100°C (212°F).
Carefully remove the ring gear from the boiling water.
After the moisture on the ring gear has completely evaporated, quickly install the ring gear to the differential case.
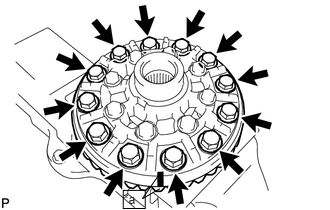
Align the matchmarks on the ring gear with that of the differential case.
| *a | Matchmark |
After the ring gear cools down sufficiently, apply adhesive to the 12 bolts and install them.
- Adhesive:
Toyota Genuine Adhesive 1360K, Three Bond 1360K or equivalent
- Torque:
- 97 N*m (985 kgf*cm, 71 ft.*lbf)
41301A
3.INSTALL REAR DIFFERENTIAL CASE BEARING
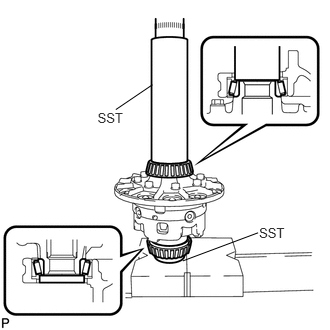
Using SST and a press, press the bearing onto the differential case.
- SST
- 09308-14010
09950-60010 (09951-00490)
4.INSPECT DIFFERENTIAL RING GEAR RUNOUT
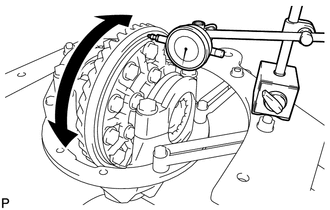
Install the differential case to the carrier and install the 2 plate washers so that there is no play in the bearing.
Install the 2 bearing caps with the 4 bolts.
- Torque:
- 103 N*m (1049 kgf*cm, 76 ft.*lbf)
Using a dial indicator, measure the runout of the ring gear.
- Maximum runout:
0.07 mm (0.00276 in.)
Remove the 2 bearing caps, 2 plate washers and differential case.
41201B
5.INSTALL REAR DRIVE PINION FRONT TAPERED ROLLER BEARING
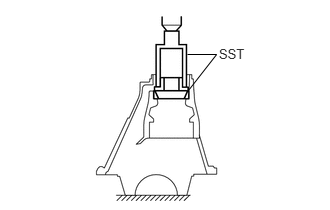
Using SST and a press, press in the roller bearing (outer) to the carrier.
- SST
- 09308-14010
09309-14040
41201A
6.INSTALL REAR DRIVE PINION REAR TAPERED ROLLER BEARING
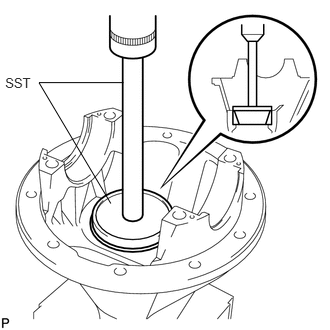
Install the plate washer to the carrier.
- HINT:
-
First, install a washer with the same thickness as the removed washer, and then check the tooth contact pattern. Replace the washer with one of a different thickness if necessary.
Using SST and a press, press the roller bearing (outer) into the carrier.
- SST
- 09950-70010 (09951-07200)
09255-10012
41201A
7.INSTALL REAR DRIVE PINION REAR TAPERED ROLLER BEARING
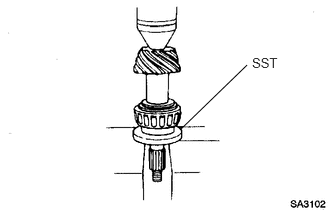
Using SST and a press, press the roller bearing (inner) onto the drive pinion.
- SST
- 09309-14040
8.ADJUST DIFFERENTIAL DRIVE PINION PRELOAD
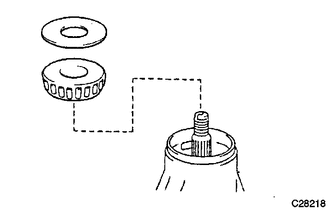
Install the drive pinion, rear drive pinion tapered roller bearing and rear differential drive pinion oil slinger.
- HINT:
-
Install the spacer and oil seal after adjusting the gear contact pattern.
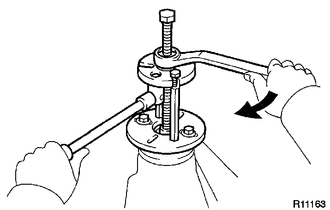
Using SST, install the companion flange.
- SST
- 09950-30012 (09951-03010, 09953-03010, 09954-03010, 09955-03030, 09956-03040)
- NOTICE:
-
Before using SST (center bolt), apply hypoid gear oil LSD to its threads and tip.
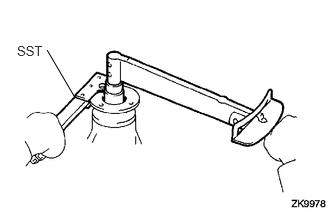
Using a 30 mm socket wrench, adjust the drive pinion preload by tightening the companion flange nut.
Using SST to hold the companion flange in place, then slowly tighten the nut within the drive pinion preload adjustment range so that it reaches the specified drive pinion preload (at Starting).
- SST
- 09330-00021
- Limit Torque Value:
457 N*m (4660 kgf*cm, 337ft.*lbf) or less
- NOTICE:
- ·
As there is no spacer, tighten the nut a little at a time. Be careful not to overtighten the nut.
- ·
Apply hypoid gear oil LSD to drive pinion thread and seat face.
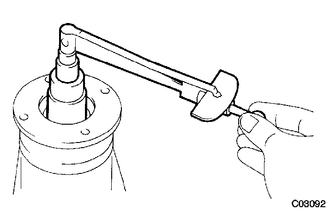
Using a torque wrench, measure the preload.
- Standard Preload (at Starting):
Item Specified Condition New bearing 0.68 to 2.03 N*m (6.94 to 20.7 kgf*cm, 6.02 to 17.9 in.*lbf) Used bearing 0.73 to 1.83 N*m (7.45 to 18.6 kgf*cm, 6.46 to 16.1 in.*lbf)
- NOTICE:
-
For a more accurate measurement, rotate the bearing forward and backward several times before measuring.
9.INSTALL DIFFERENTIAL CASE ASSEMBLY
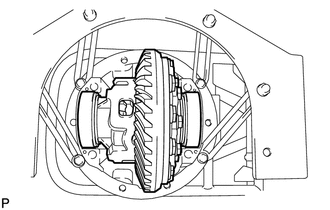
Place the 2 bearing outer races on their respective bearings.
- HINT:
-
Do not interchange the right and left races.
10.ADJUST RING GEAR BACKLASH
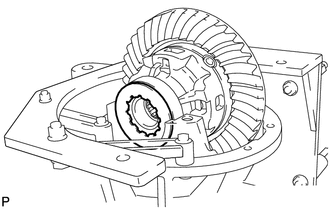
Install the plate washer on the side without the ring gear teeth.
- NOTICE:
-
Make sure that the ring gear has backlash.
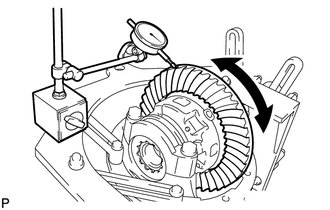
Using a dial indicator, while holding the companion flange, measure the ring gear backlash.
- Standard backlash (reference):
0.10 to 0.20 mm (0.00394 to 0.00787 in.)
Select a plate washer for the side without the ring gear teeth using the backlash as a reference.
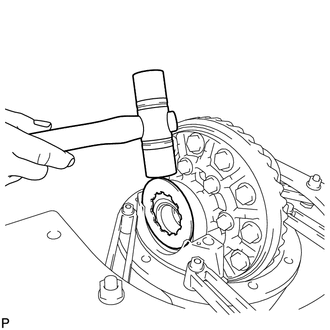
Select a plate washer for the side with the ring gear teeth so that there is no clearance between the outer race and case.
Using a plastic-faced hammer, install the plate washer for the side with the ring gear teeth.
Using a dial indicator, while holding the companion flange, measure the ring gear backlash.
- Standard backlash:
0.10 to 0.20 mm (0.00394 to 0.00787 in.)
If the backlash is not within the specification, adjust it by either increasing or decreasing the thickness of the washers on both sides by an equal amount.
- HINT:
- ·
There should be no clearance between the plate washer and case.
·Make sure that there is ring gear backlash.
11.ADJUST SIDE BEARING PRELOAD
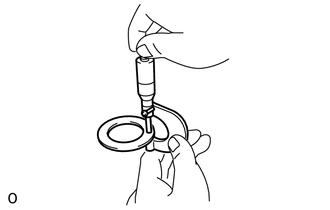
Remove the ring gear teeth side plate washer and, using a micrometer, measure the thickness.
Using the backlash as a reference, select a new washer that is 0.05 to 0.20 mm (0.00197 to 0.00787 in.) thicker than the removed washer and, using a plastic-faced hammer, tap it in so that it fits against the bearing.
- HINT:
-
Select a washer which can be pressed in 2/3 of the full amount with your finger.
Recheck the ring gear backlash.
- Standard backlash:
0.10 to 0.20 mm (0.00394 to 0.00788 in.)
If the backlash is not within the specification, adjust it by either increasing or decreasing the thickness of the washers on both sides by an equal amount.
- HINT:
-
An approximately 0.02 mm (0.000787 in.) change in each plate washer results in a 0.03 mm (0.00118 in.) change in the backlash.
- Standard Washer:
Mark Thickness Mark Thickness 70 2.05 to 2.07 mm (0.0808 to 0.0816 in.) 62 2.41 to 2.43 mm (0.0950 to 0.0957 in.) 71 2.07 to 2.09 mm (0.0816 to 0.0823 in.) 63 2.43 to 2.45 mm (0.0957 to 0.0965 in.) 72 2.09 to 2.11 mm (0.0823 to 0.0831 in.) 64 2.45 to 2.47 mm (0.0965 to 0.0973 in.) 73 2.11 to 2.13 mm (0.0831 to 0.0839 in.) 65 2.47 to 2.49 mm (0.0972 to 0.0980 in.) 74 2.13 to 2.15 mm (0.0839 to 0.0847 in.) 66 2.49 to 2.51 mm (0.0980 to 0.0988 in.) 75 2.15 to 2.17 mm (0.0847 to 0.0855 in.) 67 2.51 to 2.53 mm (0.0988 to 0.0996 in.) 76 2.17 to 2.19 mm (0.0855 to 0.0863 in.) 68 2.53 to 2.55 mm (0.0996 to 0.1000 in.) 77 2.19 to 2.21 mm (0.0863 to 0.0871 in.) 69 2.55 to 2.57 mm (0.1000 to 0.1012 in.) 78 2.21 to 2.23 mm (0.0871 to 0.0879 in.) 01 2.57 to 2.59 mm (0.1012 to 0.1020 in.) 79 2.23 to 2.25 mm (0.0879 to 0.0887 in.) 32 2.59 to 2.61 mm (0.1020 to 0.1028 in.) 80 2.25 to 2.27 mm (0.0887 to 0.0894 in.) 33 2.61 to 2.63 mm (0.1028 to 0.1035 in.) 81 2.27 to 2.29 mm (0.0894 to 0.0902 in.) 03 2.63 to 2.65 mm (0.1035 to 0.1043 in.) 82 2.27 to 2.31 mm (0.0902 to 0.0891 in.) 34 2.65 to 2.67 mm (0.1043 to 0.1051 in.) 83 2.31 to 2.33 mm (0.0910 to 0.0918 in.) 35 2.67 to 2.69 mm (0.1051 to 0.1059 in.) 84 2.33 to 2.35 mm (0.0918 to 0.0926 in.) 05 2.69 to 2.71 mm (0.1059 to 0.1067 in.) 85 2.35 to 2.37 mm (0.0926 to 0.0934 in.) 36 2.71 to 2.73 mm (0.1067 to 0.1075 in.) 86 2.37 to 2.39 mm (0.0934 to 0.0942 in.) 37 2.73 to 2.75 mm (0.1075 to 0.1082 in.) 87 2.39 to 2.41 mm (0.0942 to 0.0950 in.) 07 2.75 to 2.77 mm (0.1082 to 0.1091 in.)
12.INSTALL BEARING CAP
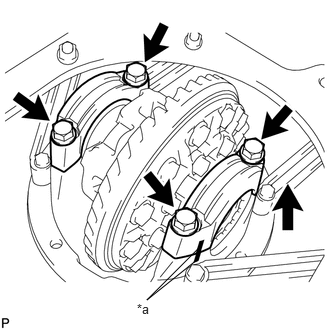
Align the matchmarks on the cap and carrier.
| *a | Matchmark |
Install the 2 bearing caps with the 4 bolts.
- Torque:
- 103 N*m (1049 kgf*cm, 76 ft.*lbf)
- HINT:
-
After rotating the ring gear 5 times or more, recheck the backlash.
13.INSPECT DIFFERENTIAL RING GEAR RUNOUT
Using a dial indicator, measure the runout of the ring gear.
- Maximum runout:
0.07 mm (0.00276 in.)
If the runout is more than the maximum, replace the ring gear.
14.INSPECT TOTAL PRELOAD
Using a torque wrench, measure the preload with the teeth of the drive pinion and ring gear in contact.
- Standard total preload (at starting):
Drive pinion preload plus 0.20 to 0.40 N*m (2.0 to 4.1 kgf*cm, 1.8 to 3.5 in.*lbf)
If necessary, disassemble and inspect the differential.
15.INSPECT TOOTH CONTACT BETWEEN RING GEAR AND DRIVE PINION
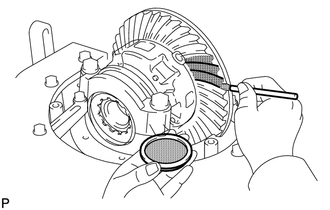
Coat 3 or 4 teeth at 3 different positions on the ring gear with Prussian blue.
Hold the companion flange firmly in place and rotate the ring gear in both directions.
Inspect the tooth contact pattern.
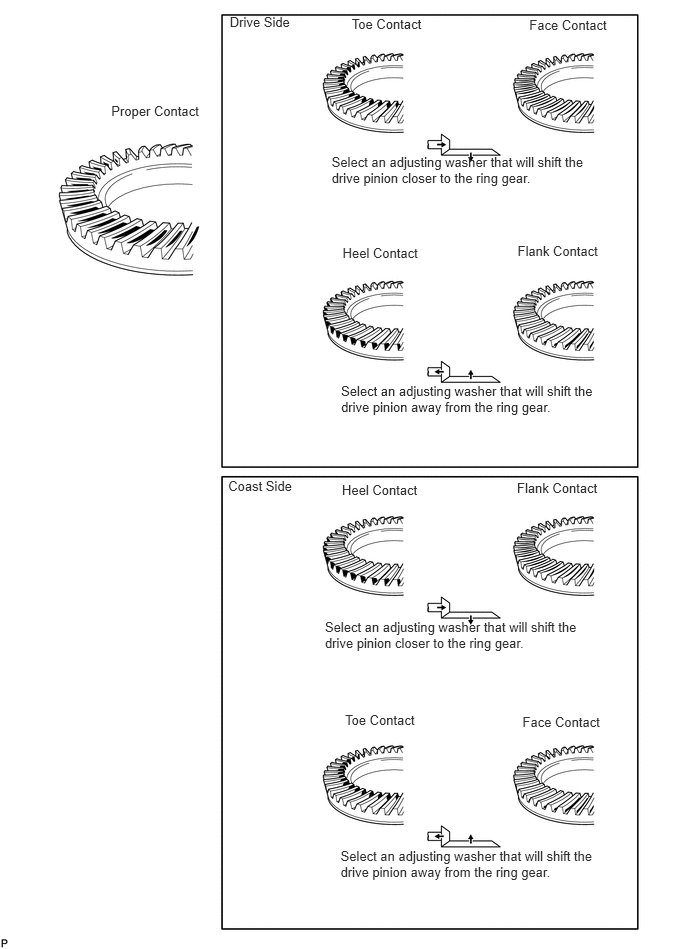
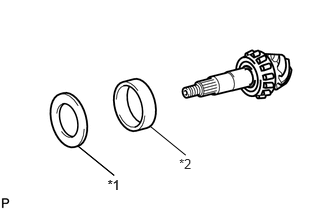
If the teeth are not engaged properly, use the following chart to select a proper washer.
| *1 | Plate Washer |
| *2 | Rear Drive Pinion Rear Tapered Roller Bearing (Outer) |
- Standard Plate Washer:
Mark Thickness Mark Thickness 29 1.84 to 1.86 mm (0.0725 to 0.0732 in.) 53 2.08 to 2.10 mm (0.0819 to 0.0826 in.) 31 1.86 to 1.88 mm (0.0733 to 0.0740 in.) 55 2.10 to 2.12 mm (0.0827 to 0.0834 in.) 33 1.88 to 1.90 mm (0.0741 to 0.0748 in.) 57 2.12 to 2.14 mm (0.0835 to 0.0842 in.) 35 1.90 to 1.92 mm (0.0749 to 0.0755 in.) 59 2.14 to 2.16 mm (0.0843 to 0.0850 in.) 37 1.92 to 1.94 mm (0.0756 to 0.0763 in.) 61 2.16 to 2.18 mm (0.0851 to 0.0858 in.) 39 1.94 to 1.96 mm (0.0764 to 0.0771 in.) 63 2.18 to 2.20 mm (0.0859 to 0.0866 in.) 41 1.96 to 1.98 mm (0.0772 to 0.0779 in.) 65 2.20 to 2.22 mm (0.0867 to 0.0874 in.) 43 1.98 to 2.00 mm (0.0780 to 0.0787 in.) 67 2.22 to 2.24 mm (0.0875 to 0.0881 in.) 45 2.00 to 2.02 mm (0.0788 to 0.0795 in.) 69 2.24 to 2.26 mm (0.0882 to 0.0889 in.) 47 2.02 to 2.04 mm (0.0796 to 0.0803 in.) 71 2.26 to 2.28 mm (0.0890 to 0.0897 in.) 49 2.04 to 2.06 mm (0.0804 to 0.0811 in.) 73 2.28 to 2.30 mm (0.0898 to 0.0905 in.) 51 2.06 to 2.08 mm (0.0812 to 0.0818 in.) 75 2.30 to 2.32 mm (0.0906 to 0.0913 in.)
41204B
16.REMOVE REAR DRIVE PINION NUT
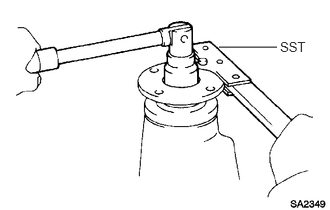
Using SST to hold the companion flange in place, remove the nut.
- SST
- 09330-00021
41204
17.REMOVE REAR DRIVE PINION COMPANION FLANGE SUB-ASSEMBLY
41214
18.REMOVE REAR DIFFERENTIAL DRIVE PINION OIL SLINGER
41201B
19.REMOVE REAR DRIVE PINION FRONT TAPERED ROLLER BEARING (INNER)
41201B
20.REMOVE REAR DRIVE PINION FRONT TAPERED ROLLER BEARING (OUTER)
41231
21.INSTALL REAR DIFFERENTIAL DRIVE PINION BEARING SPACER
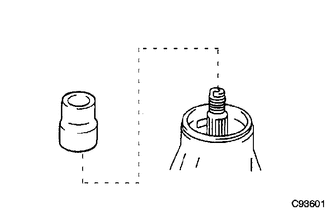
Install a new bearing spacer to the drive pinion.
41115
22.INSTALL DIFFERENTIAL OIL STORAGE RING
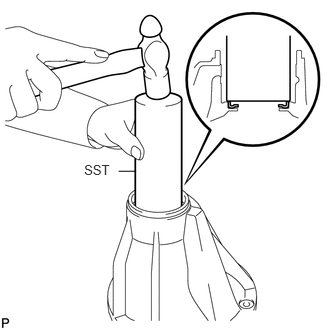
Using SST, tap in a new oil storage ring.
- SST
- 09308-14010
41201B
23.INSTALL REAR DRIVE PINION FRONT TAPERED ROLLER BEARING (INNER)
41201B
24.INSTALL REAR DRIVE PINION FRONT TAPERED ROLLER BEARING (OUTER)
41214
25.INSTALL REAR DIFFERENTIAL DRIVE PINION OIL SLINGER
41201C
26.INSTALL REAR DIFFERENTIAL CARRIER OIL SEAL
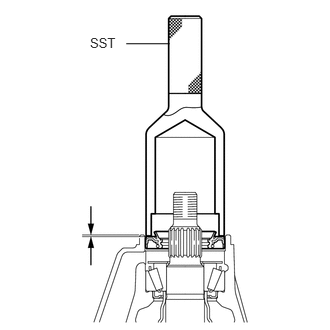
Apply MP grease to a new oil seal.
Using SST and a hammer, tap in the oil seal.
- SST
- 09554-30011
- Standard oil seal depth:
-0.3 to 0.3 mm (-0.0118 to 0.0118 in.)
41204
27.INSTALL REAR DRIVE PINION COMPANION FLANGE SUB-ASSEMBLY
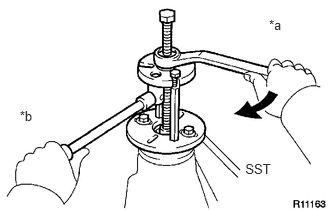
Using SST, install the companion flange to the drive pinion.
- SST
- 09950-30012 (09951-03010, 09953-03010, 09954-03010, 09955-03030, 09956-03040)
| *a | Turn |
| *b | Hold |
- NOTICE:
-
Before using SST (center bolt), apply hypoid gear oil to its threads and tip.
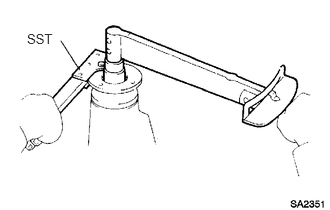
Coat the threads of a new nut with hypoid gear oil.
Using SST to hold the companion flange in place, then slowly tighten the nut within the drive pinion preload adjustment range so that it reaches the specified drive pinion preload (at Starting).
- SST
- 09330-00021
- Limit Torque Value:
457 N*m (4660 kgf*cm, 337ft.*lbf) or less
28.INSPECT DRIVE PINION PRELOAD
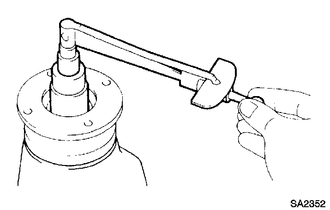
Using a torque wrench, measure the preload of the backlash between the drive pinion and ring gear.
- Standard Preload (at Starting):
Item Specified Condition New bearing 0.83 to 2.18 N*m (8.64 to 22.2 kgf*cm, 7.35 to 19.3 in.*lbf) Used bearing 0.88 to 1.98 N*m (8.97 to 20.2 kgf*cm, 7.79 to 17.5 in.*lbf)
If the result not as specified, replace the bearing spacer.
If the preload is less than the minimum, retighten the nut with 13 N*m (130 kgf*cm, 9 ft.*lbf) of torque at a time until the specified preload is reached.
- Limit Torque Value:
457 N*m (4660 kgf*cm, 337ft.*lbf) or less
If the maximum torque is exceeded while retightening the nut, replace the bearing spacer and repeat the preload adjusting procedure.
- HINT:
-
Do not loosen the pinion nut to reduce the preload.
29.INSPECT TOTAL PRELOAD
Using a torque wrench, measure the preload with the teeth of the drive pinion and ring gear in contact.
- Standard total preload (at starting):
Drive pinion preload plus 0.20 to 0.40 N*m (2.0 to 4.1 kgf*cm, 1.8 to 3.5 in.*lbf)
If necessary, disassemble and inspect the differential.
30.INSPECT DIFFERENTIAL RING GEAR BACKLASH
Using a dial indicator, check the backlash of the ring gear.
- Standard backlash:
0.10 to 0.20 mm (0.00394 to 0.00787 in.)
If the backlash is not as specified, adjust the side bearing preload or perform repairs as necessary.
- HINT:
-
Perform the measurement at 3 or more positions around the circumference of the ring gear.
41204
31.INSPECT RUNOUT OF REAR DRIVE PINION COMPANION FLANGE SUB-ASSEMBLY
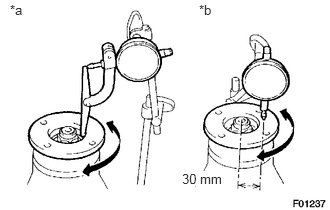
Using a dial indicator, measure the runout of the drive pinion companion flange vertically and laterally.
- Distance from center to runout measurement point:
30 mm (1.18 in.)
- Maximum Runout:
Item Specified Condition Vertical runout 0.10 mm (0.00394 in.) Lateral runout 0.10 mm (0.00394 in.)
| *a | Vertical Runout |
| *b | Lateral Runout |
If the runout is more than the maximum, replace the companion flange.
41204B
32.STAKE DRIVE PINION NUT
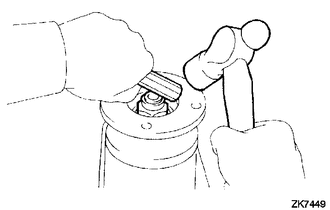
Using a chisel and hammer, stake the nut.