INTRODUCTION WORK NOTICES AND PRECAUTIONS PRECAUTIONS FOR WELDING
REMOVAL OF ADJACENT COMPONENTS
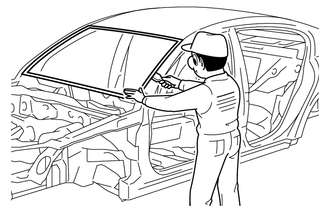
To prevent damage to the body and parts, apply protective tape to the body and tools before removing the parts.
- NOTICE:
-
If the paint film is damaged, make sure to refinish the paint.
CUTTING WORK
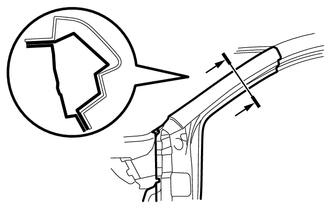
When cutting a panel, be careful not to damage the surrounding panels or any panels underneath.
- NOTICE:
-
If any panels are damaged, be sure to repair them.
ANTI-RUST TREATMENT BEFORE WELDING
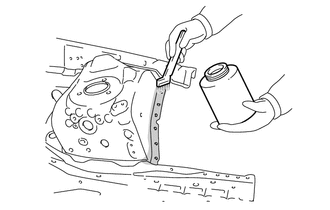
Apply welding primer to the contact surfaces of the welding areas to protect them from rust.
- NOTICE:
-
Do not apply welding primer outside of the contact surfaces.
WELDING WORK
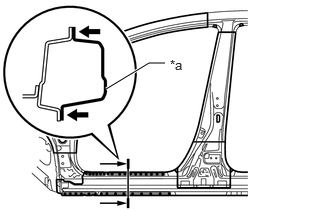
| *a | 1500 MPa or 1180 MPa or 980 MPa or 780 MPa ultra high strength steel |
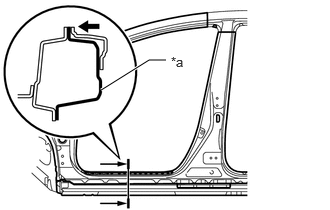
| *a | 1500 MPa or 1180 MPa or 980 MPa or 780 MPa Ultra High Strength Steel |
Follow the welding conditions below when welding ultra high strength steel to assure sufficient weld strength.
| Plug weld | Plug diameter | 10 mm (0.39 in.) |
| Wire type | AWS A5.18 ER70S-6/ER70S-3 | |
| Shield gas | Metal active gas |
| Spot weld | Pressure | 2940 N (300 kgf, 661 lbf) | |
| Weld current | 10000 A | ||
| Weld time | ROCKER PANEL (See the body weld point) |
16 Cyc.(0.27 Sec.) | |
| Plug weld | Plug diameter | 10 mm (0.39 in.) | |
| Wire type | AWS A5.18 ER70S-6/ER70S-3 | ||
| Shield gas | Metal active gas | ||
- NOTICE:
-
Be sure to use Metal active gas (Ar + CO2 20 to 30% or Ar + O2 2%) as the shield gas when plug welding. Sufficient weld strength cannot be assured when using 100% CO2 shield gas.
| Plug weld | Plug diameter | Same as the standard method (See the introduction) |
| Wire type | AWS A5.18 ER70S-6/ER70S-3 | |
| Shield gas | Metal active gas |
- NOTICE:
-
Be sure to use Metal active gas (Ar + CO2 20 to 30% or Ar + O2 2%) as the shield gas when plug welding. Sufficient weld strength cannot be assured when using 100% CO2 shield gas.
Standard Number of Welds
| Number of spot welds | 980 MPa ultra high strength steel | More than the number of welds made by the manufacturer |
| Normal steel or high strength steel | More than 1.3x the number of welds made by the manufacturer | |
| Number of plug welds | 1500 MPa or 1180 MPa or 980 MPa or 780 MPa ultra high strength steel | More than the number of welds made by the manufacturer |
| Normal steel or high strength steel |
- NOTICE:
-
Inspect the welds after spot welding. For points with insufficient weld strength join the panels using plug welds.
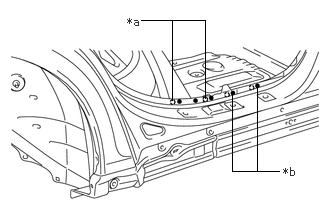
| *a | Old Spot Locations |
| *b | New Spot Locations |
Spot weld locations
Avoid welding over previously welded areas.
MAKING HOLES FOR PLUG WELDING
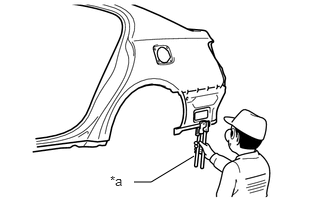
| *a | Puncher |
For areas where a spot welder cannot be used, use a puncher or drill to make holes for plug welding.
| Thickness of Welded Portion | Diameter of Plug Hole |
|---|---|
| Under 1.0 mm (0.04 in.) | Over 5.0 mm (0.20 in.) |
| 1.0 to 1.6 mm (0.04 to 0.06 in.) | Over 6.5 mm (0.26 in.) |
| 1.7 to 2.3 mm (0.07 to 0.09 in.) | Over 8.0 mm (0.31 in.) |
| Over 2.4 mm (0.09 in.) | Over 10 mm (0.39 in.) |