INTRODUCTION ABOUT THIS VEHICLE STRUCTURAL OUTLINE
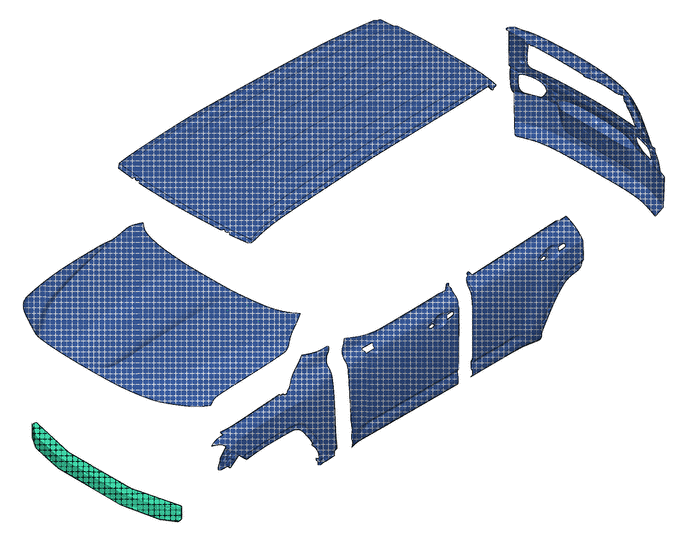

|
Aluminum (6000 series) |

|
Aluminum |
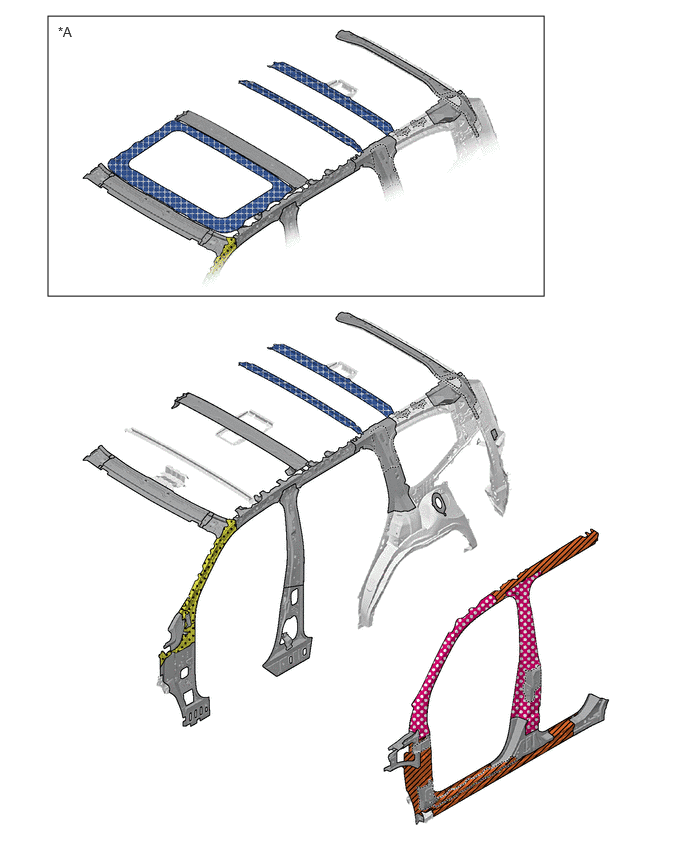
| *A | for Moon Roof | - | - |

|
1500 MPa Ultra High Strength Steel |

|
1180 MPa Ultra High Strength Steel |

|
980 MPa Ultra High Strength Steel |

|
590 MPa High Strength Steel or less |
|
|
Aluminum (6000 series) | - | - |
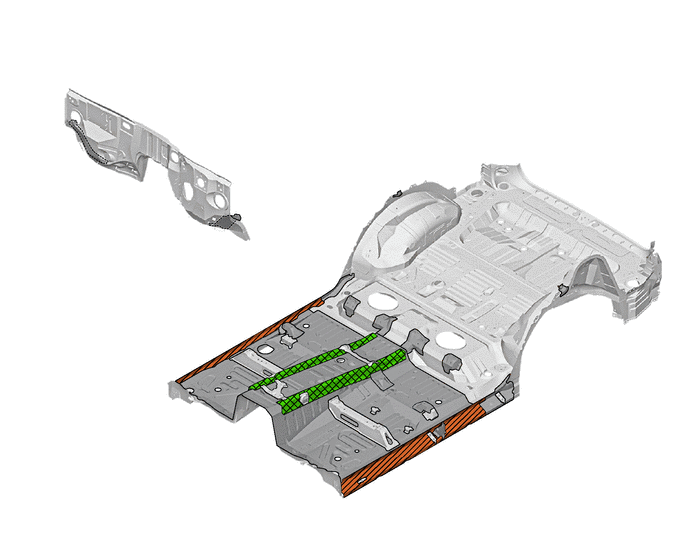
|
|
1180 MPa Ultra High Strength Steel |

|
780 MPa High Strength Steel |
|
|
590 MPa High Strength Steel or less | - | - |
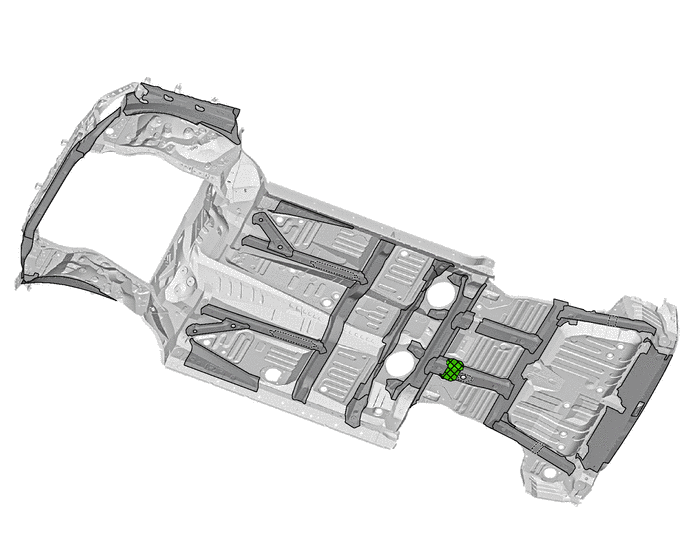
|
|
780 MPa High Strength Steel |
|
590 MPa High Strength Steel or less |
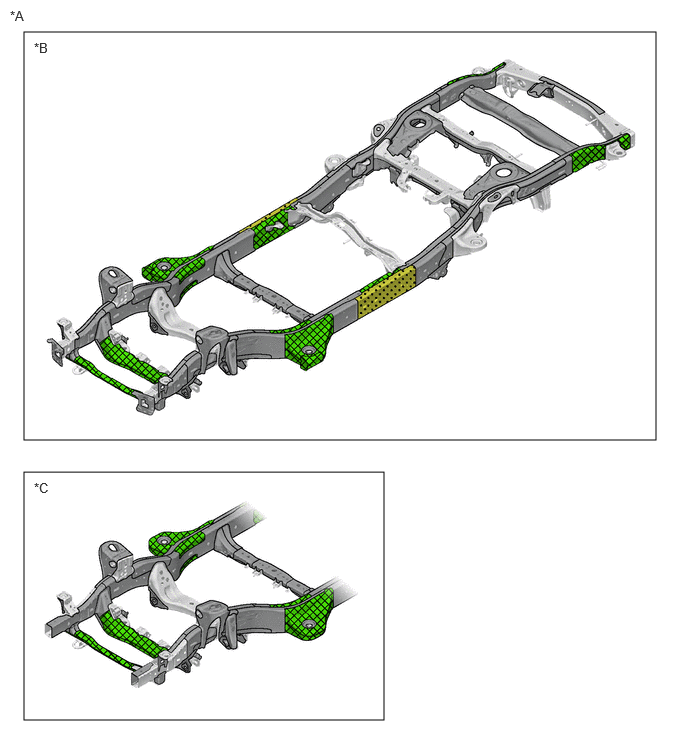
| *A | for Type A | *B | w/o Winch, w/ KDSS |
| *C | w/ Winch, w/o KDSS | - | - |
|
|
980 MPa Ultra High Strength Steel |
|
780 MPa High Strength Steel |
|
|
590 MPa High Strength Steel or less | - | - |
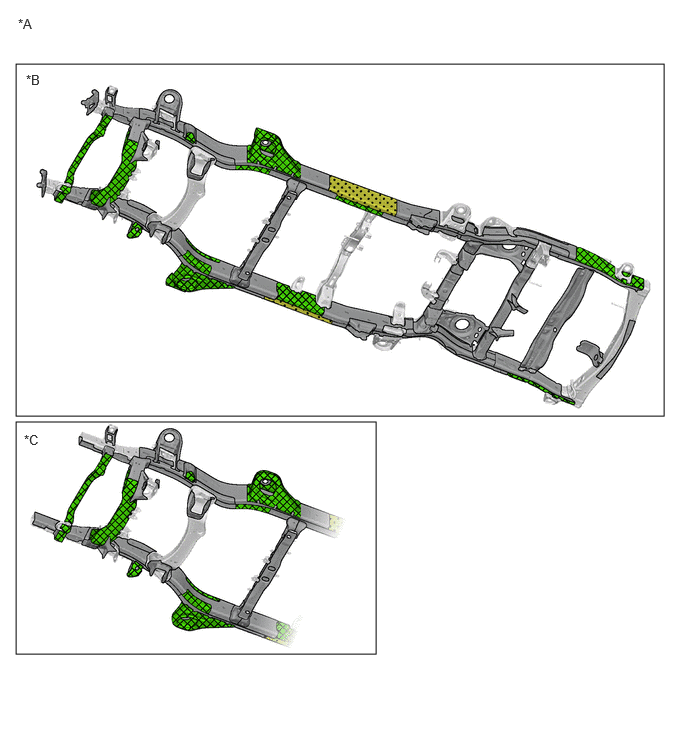
| *A | for Type A | *B | w/o Winch, w/ KDSS |
| *C | w/ Winch, w/o KDSS | - | - |
|
|
980 MPa Ultra High Strength Steel |
|
780 MPa High Strength Steel |
|
|
590 MPa High Strength Steel or less | - | - |
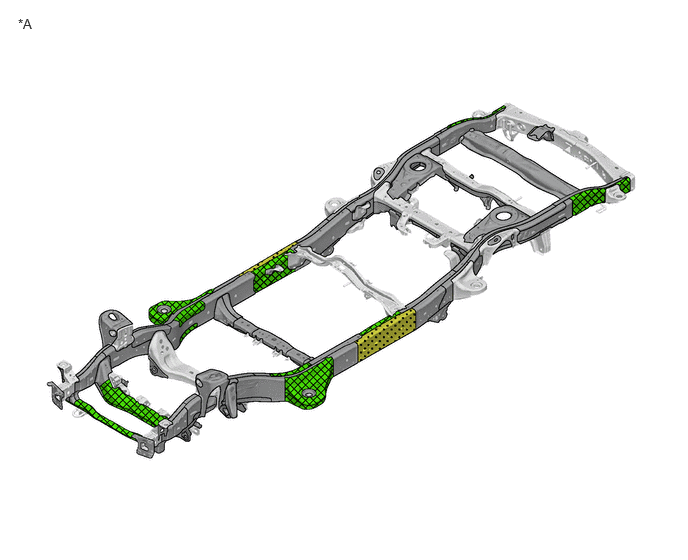
| *A | for Type B | - | - |
|
|
980 MPa Ultra High Strength Steel |
|
780 MPa High Strength Steel |
|
|
590 MPa High Strength Steel or less | - | - |
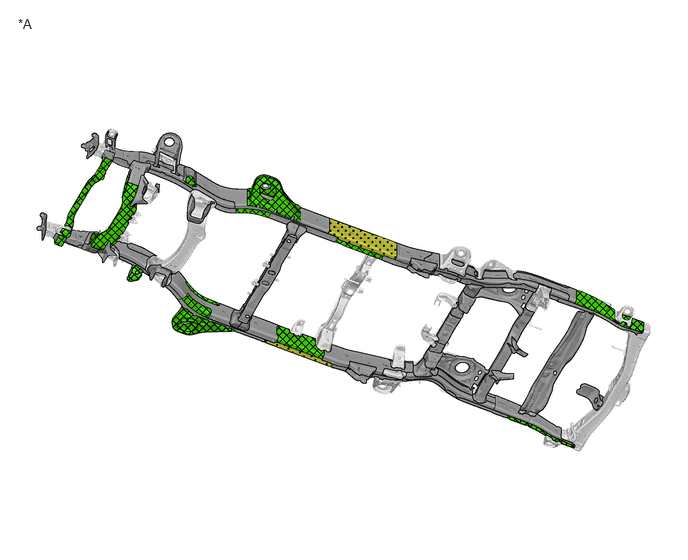
| *A | for Type B | - | - |
|
|
980 MPa Ultra High Strength Steel |
|
780 MPa High Strength Steel |
|
|
590 MPa High Strength Steel or less | - | - |
STRUCTURAL OUTLINE OF ALUMINUM ROOF PANEL
Aluminum is used for the roof panel to improve driveability (reduced weight and a lower center of gravity).
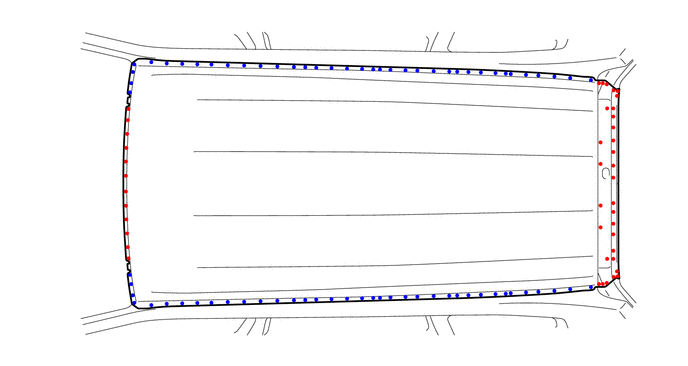

|
SPR |

|
RPW or EASW |
ALUMINUM ROOF PANEL CONNECTION METHOD (NEW VEHICLE STATUS)
- HINT:
-
Refer to the removal and installation procedures for the roof panel for information on repair/connection methods.
SPR(Self Piercing Rivet)
This is a dissimilar metal connection method that does not require first opening a pilot hole in the base material. The punches push the SPRs through the upper base material into the die, the rivets in the lower panel widened and form an interlock.
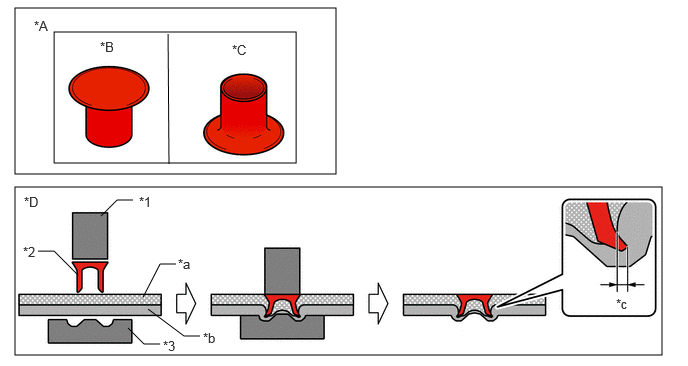
| *A | SPR External Appearance | *B | Upper Face |
| *C | Lower Face | *D | SPR Connection Process |
| *1 | Punche | *2 | SPR |
| *3 | Die | - | - |
| *a | Upper Panel | *b | Lower Panel |
| *c | Interlock Formation Area | - | - |
RPW (Resistance Pierce Welding)
This is a dissimilar metal connection method that does not require first opening a pilot hole in the base material. The aluminum in the upper panel is softened by inserting it between the rivets and the base material and then applying voltage/current using electrodes. The rivets pierce through the upper panel and then the rivets and lower steel plate are resistance welded together.
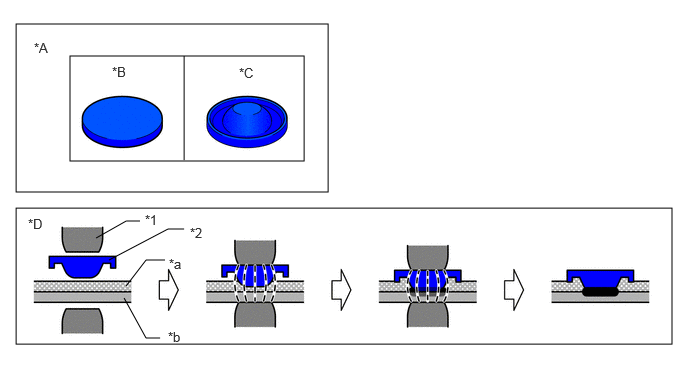
| *A | RPW Rivet External Appearance | *B | Upper Face |
| *C | Lower Face | *D | RPW Connection Process |
| *1 | Electrodes | *2 | Rivet |
| *a | Upper Panel | *b | Lower Panel |
EASW(Element Arc Spot Welding)
This is a dissimilar metal connection method in which a pilot hole is first opened in the base material upper panel. An element is inserted into the pilot hole opened in the aluminum in the upper panel, and then the hollow space in the element is arc welded to weld the element and lower steel plate together.
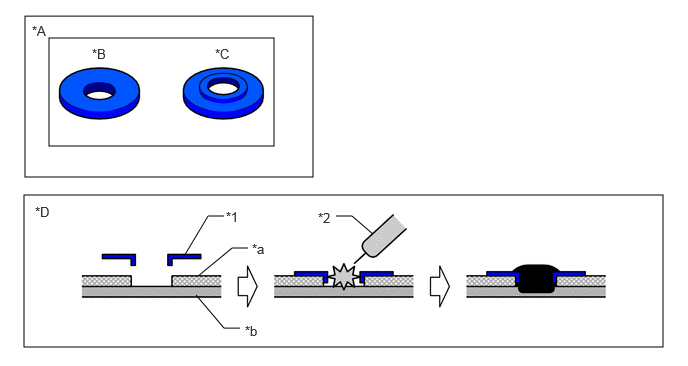
| *A | EASW Element External Appearance | *B | Upper Face |
| *C | Lower Face | *D | EASW Connection Process |
| *1 | Element | *2 | Welder Nozzle |
| *a | Upper Panel | *b | Lower Panel |