BODY WELD POINT FRONT FENDER APRON ASSEMBLY REPLACEMENT
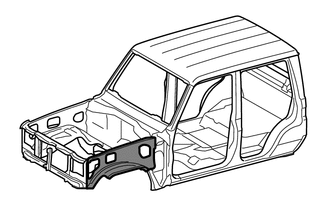
With the radiator side support assembly and radiator lower support assembly removed.
REMOVAL
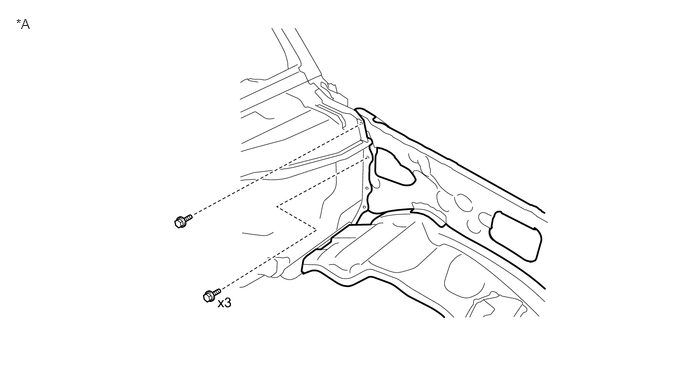
| *A | LH | - | - |
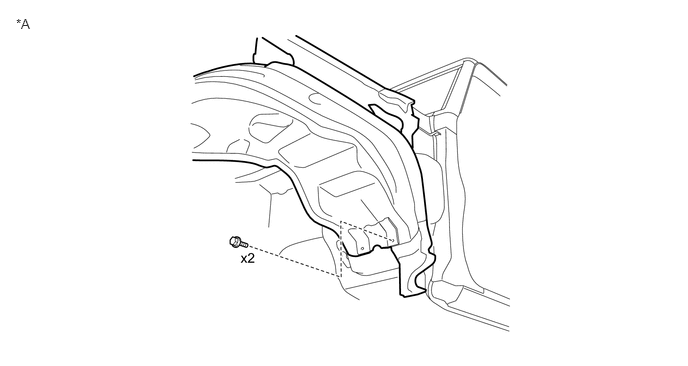
| *A | LH | - | - |
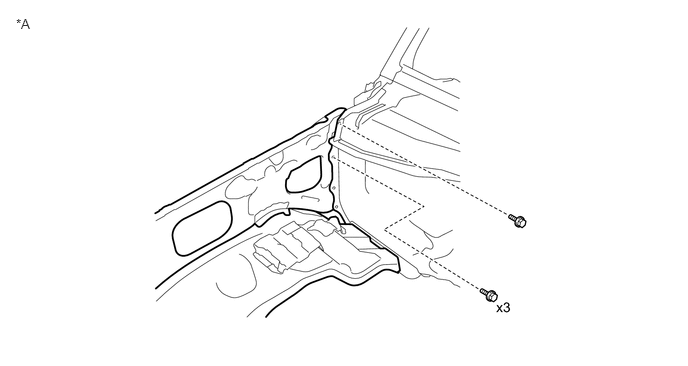
| *A | RH | - | - |
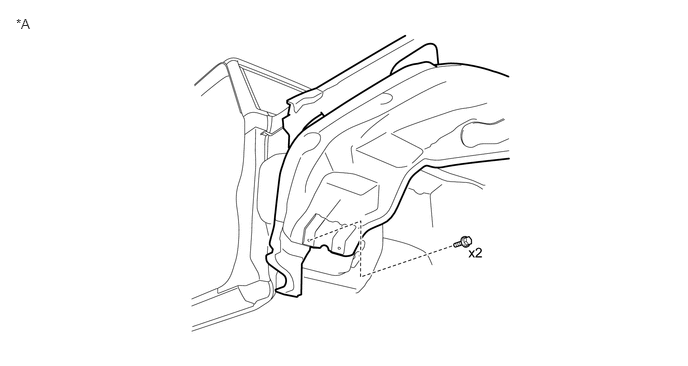
| *A | RH | - | - |
INSTALLATION
| Symbol Meaning | |
|---|---|

|
Plug Weld |
Inspect the fitting of the related parts around the new parts before welding. This affects the appearance of the finish.
Temporarily install the new parts and measure each part of the new parts in accordance with the body dimension diagram. (See the body dimensions)
Apply adhesive (3MTM AutomixTM Panel Bonding Adhesive #8115).
- HINT:
-
·
Apply a light coat of adhesive around the plug welding points.
·Apply enough adhesive to the panels.
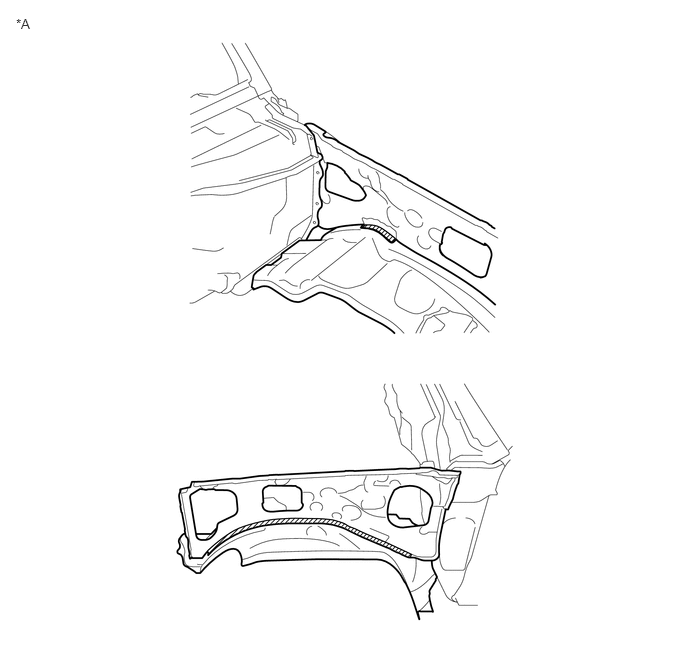
| *A | LH | - | - |

|
Adhesive | - | - |
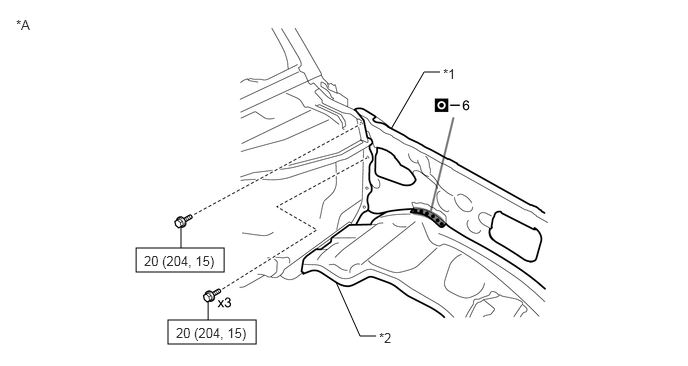
| *A | LH | - | - |
| *1 | FRONT APRON TO COWL SIDE MEMBER SUB-ASSEMBLY | *2 | FRONT FENDER APRON SUB-ASSEMBLY |

|
N*m (kgf*cm, ft.*lbf): Specified torque | - | - |
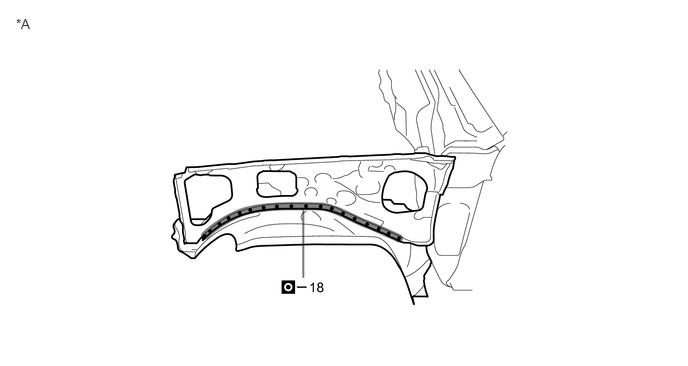
| *A | LH | - | - |
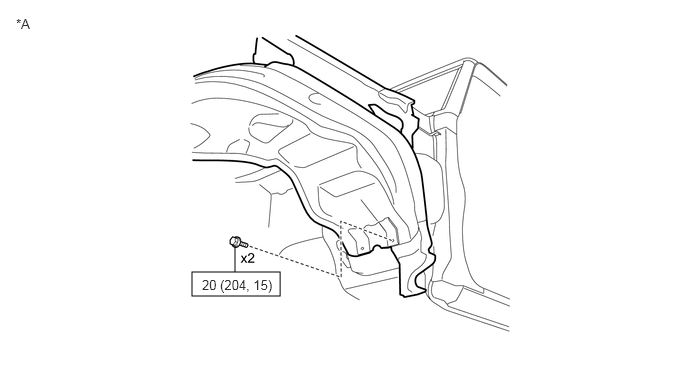
| *A | LH | - | - |
|
|
N*m (kgf*cm, ft.*lbf): Specified torque | - | - |
Apply adhesive (3MTM AutomixTM Panel Bonding Adhesive #8115).
- HINT:
-
·
Apply a light coat of adhesive around the plug welding points.
·Apply enough adhesive to the panels.
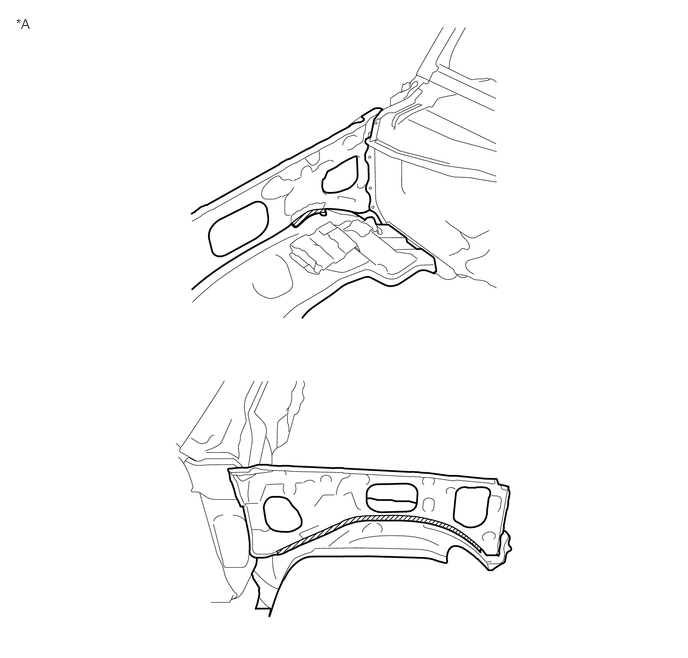
| *A | RH | - | - |
|
|
Adhesive | - | - |
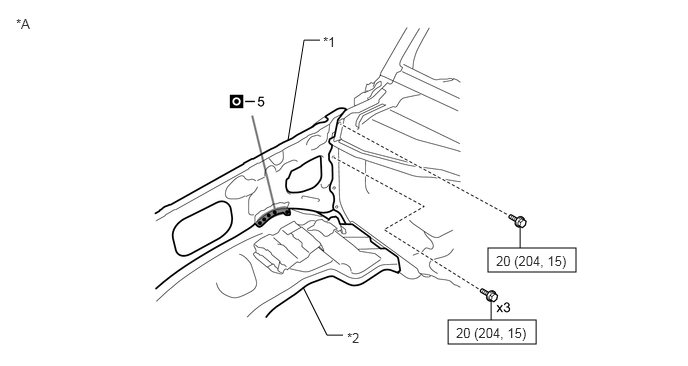
| *A | RH | - | - |
| *1 | FRONT APRON TO COWL SIDE MEMBER SUB-ASSEMBLY | *2 | FRONT FENDER APRON SUB-ASSEMBLY |
|
|
N*m (kgf*cm, ft.*lbf): Specified torque | - | - |
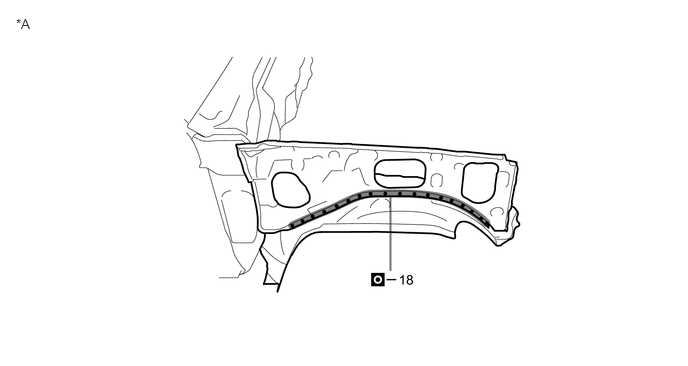
| *A | RH | - | - |
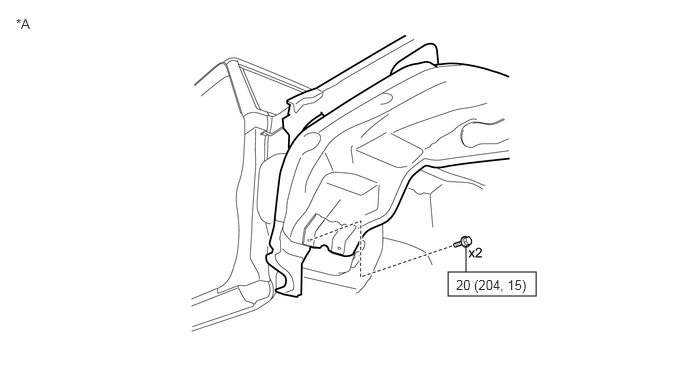
| *A | RH | - | - |
|
|
N*m (kgf*cm, ft.*lbf): Specified torque | - | - |
After welding, apply undercoating to the corresponding parts. (See the painting/coating)
After applying the top coat, apply anti-rust agent to the internal panel portion of the closed section structural weld points.