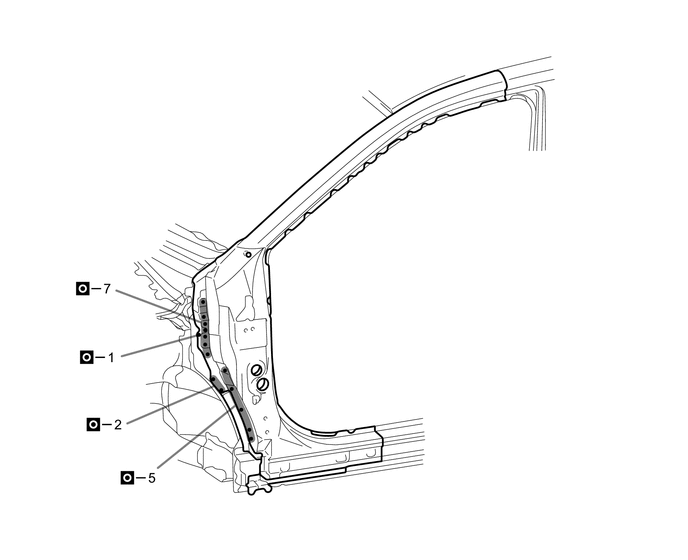
BODY PANEL FRONT BODY PILLAR CUT AND JOIN REPLACEMENT SECTIONS (PATTERN 1)
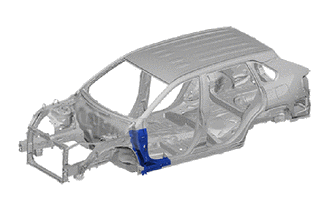
With the cowl top side upper panel assembly removed.
REMOVAL
| Symbol Meaning | |
|---|---|

|
Remove Weld Points |

|
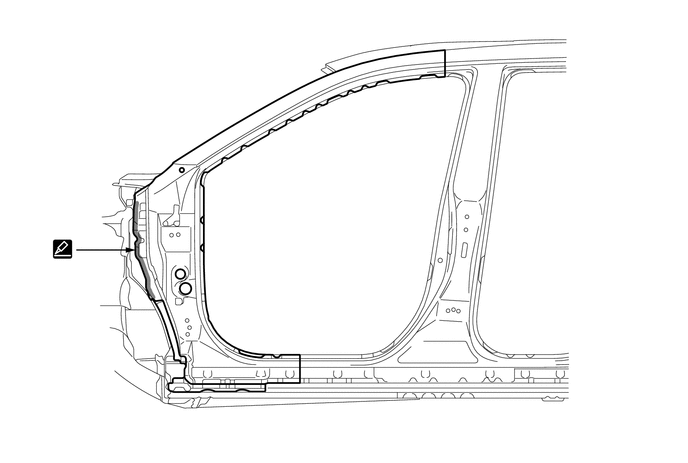
Cut and Join Location |

|
Cut Location for Supply Parts |
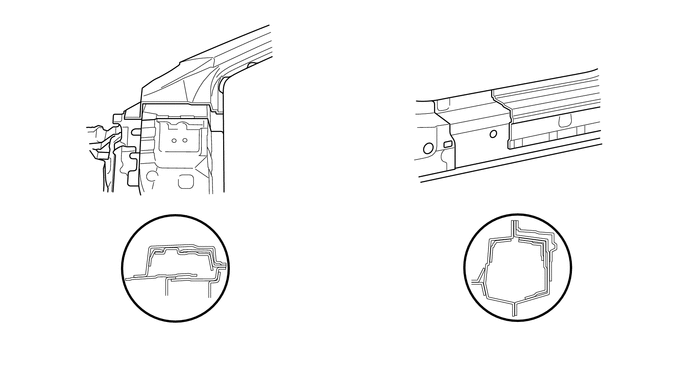
Do not butt weld or heat repair because the heat decreases the strength of areas where ultra high strength steel is used. (See the introduction)
Roughly cut open the panel so that the adhesive can be reached. Cut through the adhesive with a cut chisel to remove the panel.
- HINT:
-
In cases where the adhesive cannot be removed with a cut chisel, heat the adhesive with an industrial heater gun or gas burner taking care not to cause panel deformation by overheating.
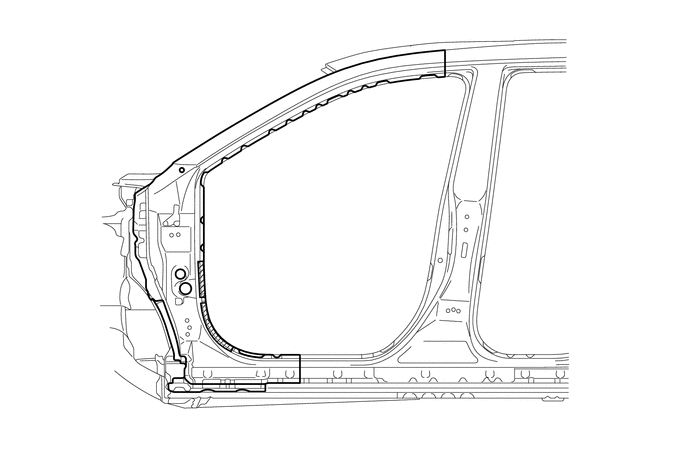

|
Adhesive | - | - |
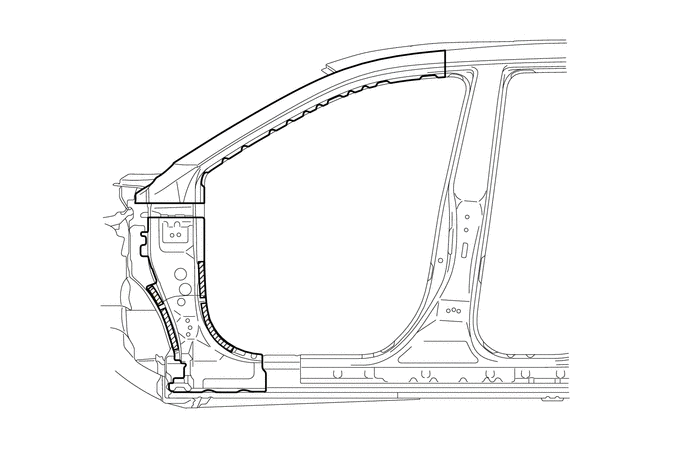
Remove the front body pillar upper outer.
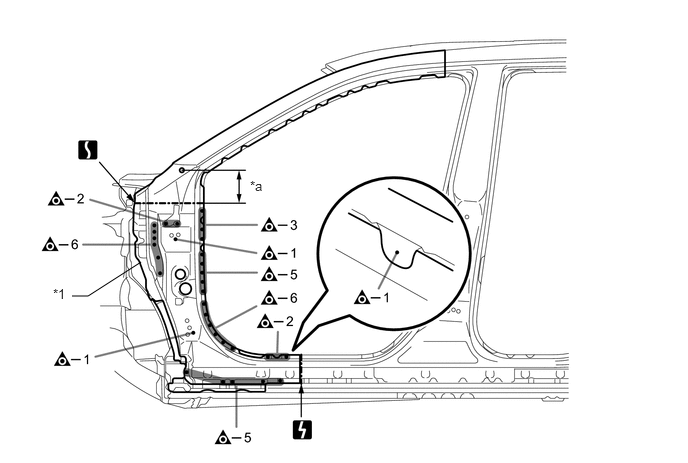
| *1 | FRONT BODY PILLAR UPPER OUTER | - | - |
| *a | 125 mm (4.92 in.) | - | - |
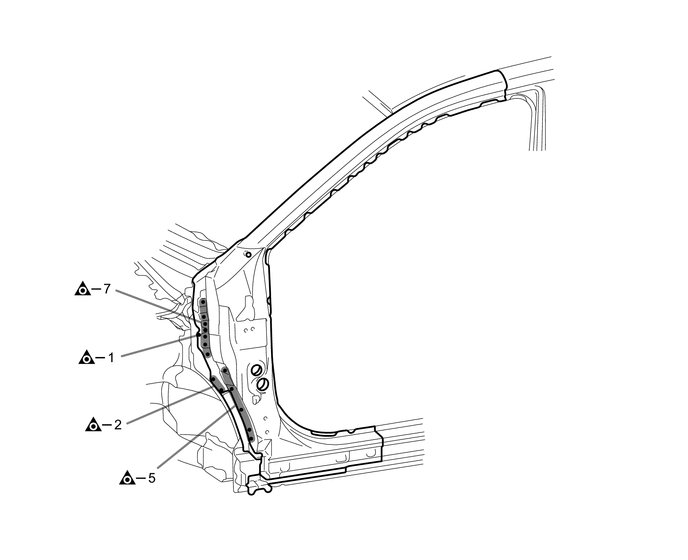
Roughly cut open the panel so that the adhesive can be reached. Cut through the adhesive with a cut chisel to remove the panel.
- HINT:
-
In cases where the adhesive cannot be removed with a cut chisel, heat the adhesive with an industrial heater gun or gas burner taking care not to cause panel deformation by overheating.
|
|
Adhesive | - | - |
Remove the front body pillar reinforce sub-assembly lower.
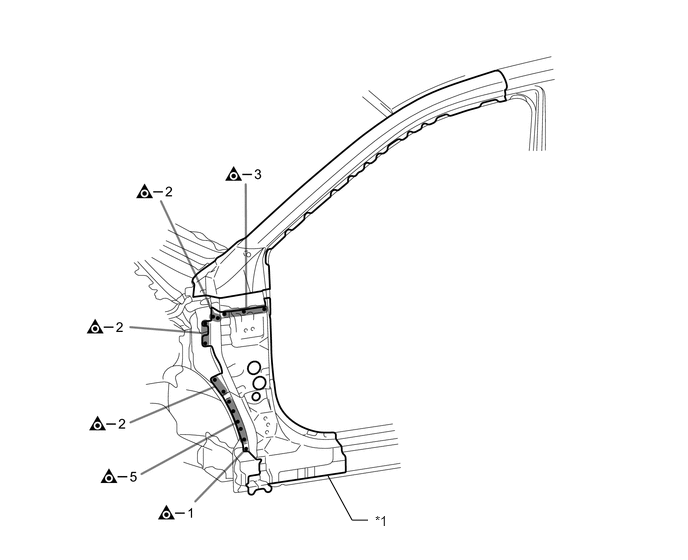
| *1 | FRONT BODY PILLAR REINFORCE SUB-ASSEMBLY LOWER | - | - |
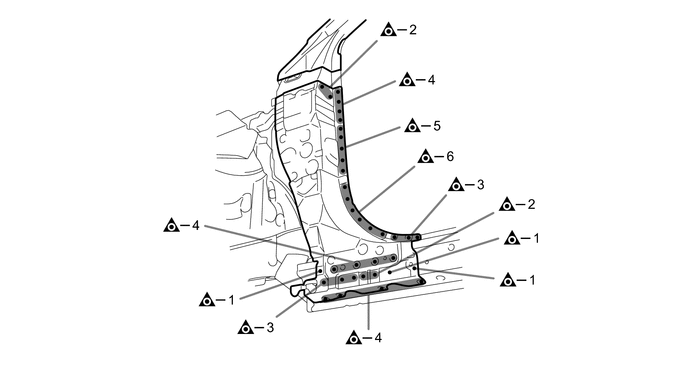
When replace only the outer panel, please cut off a necessary range depending on a damage range.
Carefully cut the outer panel so not to damage the reinforcement.
Make sure that butt welding does not heat-affect the reinforcement when welding the outer panel.
INSTALLATION
| Symbol Meaning | |
|---|---|

|
Plug Weld |

|
Butt Weld |

|
Body Sealer |
Inspect the fitting of the related parts around the new parts before welding. This affects the appearance of the finish.
Temporarily install the new parts and measure each part of the new parts in accordance with the body dimension diagram. (See the body dimensions)
Apply adhesive (3MTM AutomixTM Panel Bonding Adhesive #8115).
- HINT:
- ·
Do not apply adhesive around the plug welding points.
·Minimize squeeze out in plug welding areas.
|
|
Adhesive | - | - |
Weld the front body pillar reinforce sub-assembly lower to the vehicle side.
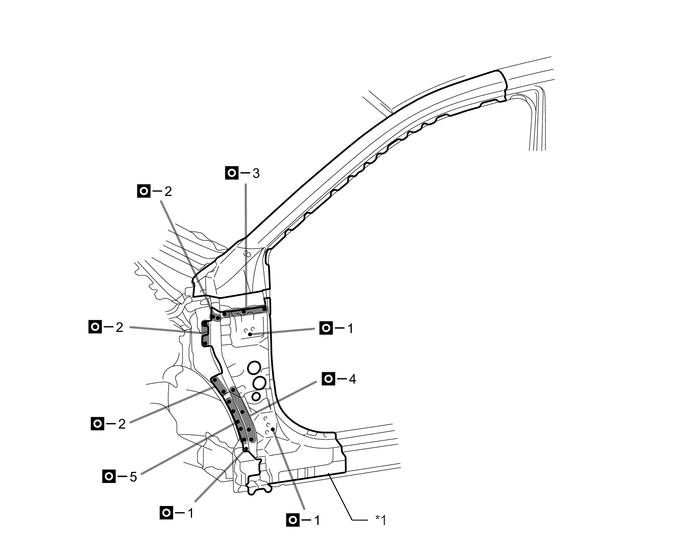
| *1 | FRONT BODY PILLAR REINFORCE SUB-ASSEMBLY LOWER | - | - |
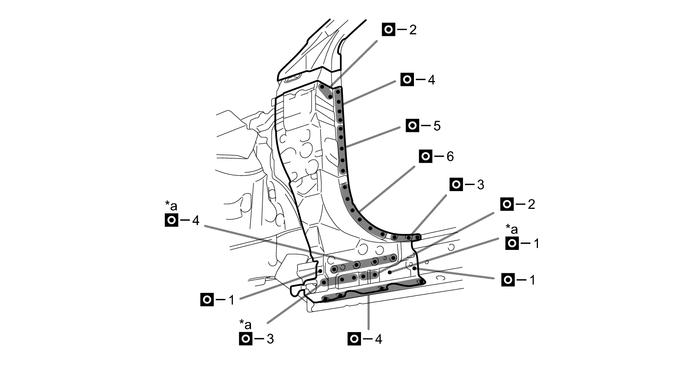
| *a | Ultra High Strength Steel Welding Point | - | - |
When welding 2 panels together including 980 MPa ultra high strength steel.
| *a: Plug weld | Plug diameter | 10 mm (0.39 in.) |
| Wire type | AWS A5.18 ER70S-3 | |
| Shield gas | Metal active gas |
- NOTICE:
-
Be sure to use Metal active gas (Ar 80% + CO2 20%) as the shield gas when plug welding.Sufficient weld strength cannot be assured when using 100% CO2 shield gas.
Before installing a new part, apply body sealer.
- HINT:
-
Apply body sealer in an even, continuous bead.
Apply adhesive (3MTM AutomixTM Panel Bonding Adhesive #8115).
- HINT:
- ·
Do not apply adhesive around the plug welding points.
·Minimize squeeze out in plug welding areas.
|
|
Adhesive | - | - |
Weld the front body pillar upper outer to the vehicle side.
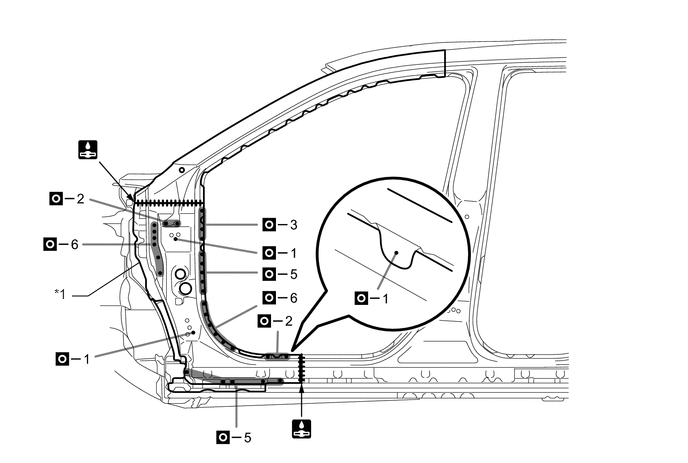
| *1 | FRONT BODY PILLAR UPPER OUTER | - | - |
After welding, apply body sealer to the corresponding parts. (See the painting/coating)
After applying the top coat, apply anti-rust agent to the internal panel portion of the closed section structural weld points.