BODY PANEL FRONT BODY PILLAR CUT AND JOIN REPLACEMENT SECTIONS (PATTERN 1)
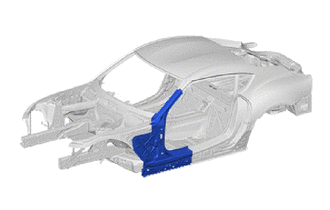
REMOVE THE ADHESIVE
Detach any mechanical connecting elements where required.
Heat the adhesive flange with a hot air blower.
- NOTICE:
-
Do not exceed the maximum object temperature of 250°C.
Use pliers or a chisel to peel off the component.
- NOTICE:
-
Do not damage adjacent components.
Remove adhesive residue from the adhesive flange.
REMOVAL
| Symbol Meaning | |
|---|---|

|
Remove Weld Points |

|
Cut with Disc Sander etc. |

|
Cut and Join Location |
Mark and perform the separating cuts to match the specified dimensions.
- NOTICE:
-
Thereby disconnect only the outer panel.
Remove the weld points in areas (1).
Remove the weld points and adhesive in area (2).
Remove the adhesive in area (3).
Remove the side panel sub-assy outer from the foamed sealing material in areas (4).
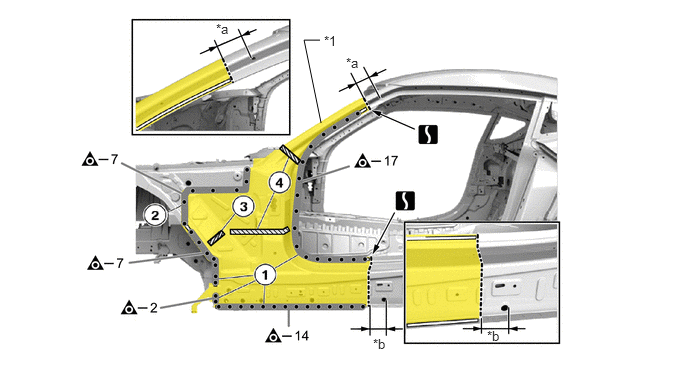
| *1 | SIDE PANEL SUB-ASSY OUTER | - | - |
| *a | 70 mm (2.76 in.) from the lower edge of the hole | *b | 80 mm (3.15 in.) from the upper edge of the hole |

|
Adhesive | 
|
Foamed Sealing Material |
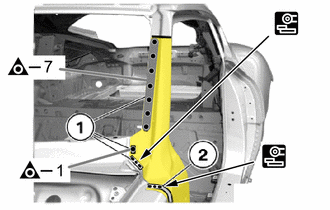
Remove the weld points in areas (1).
Remove the weld points and adhesive in area (2).
INSTALL FOAMED SEALING MATERIAL
- HINT:
- ·
Schematic diagram is for example purposes.
·Some parts may differ in certain details.
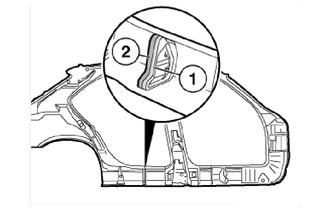
Clean the contact surface (1) with the cleaner R2.
- Expendable materials:
Cleaner R2 500ml 08879-WA010
On the contact surface (1), apply an approximately 15 mm bead (2) of brushable seam seal. If necessary apply a slightly thinner bead of brushable seam seal on each side, to prevent the sealant from running.
- Expendable materials:
Brushable Seam Seal 310ml 08826-WA230
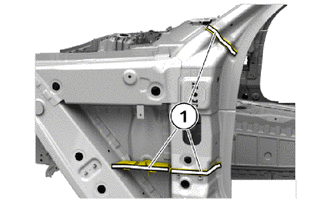
Clean contact surfaces (1) using cleaner R2.
- Expendable materials:
Cleaner R2 500ml 08879-WA010
Apply brushable seam seal to the foamed sealing material in these areas (1).
- Expendable materials:
Brushable Seam Seal 310ml 08826-WA230
INSTALLATION
| Symbol Meaning | |
|---|---|

|
Plug Weld |

|
Fillet Weld |

|
Butt Weld |
Position the side panel sub-assy outer.
Weld the side panel sub-assy outer in areas (2).
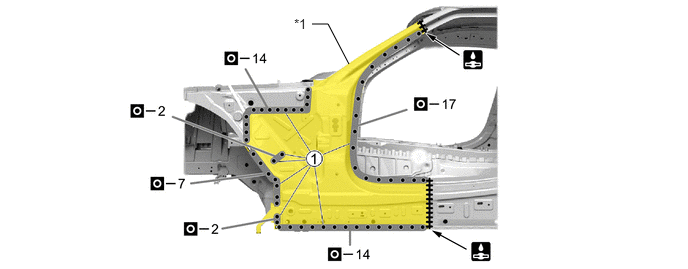
| *1 | SIDE PANEL SUB-ASSY OUTER | - | - |
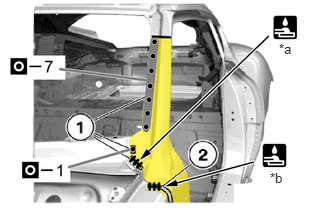
| *a | 50 mm (1.97 in.) |
| *b | 30 mm (1.18 in.) |
Weld the side panel sub-assy outer in areas (1) and (2).
Apply seam seal in these areas (1).
After welding, apply body sealer and undercoating to the corresponding parts. (See the painting/coating)
After applying the top coat, apply anti-rust agent to the internal panel portion of the closed section structural weld points.