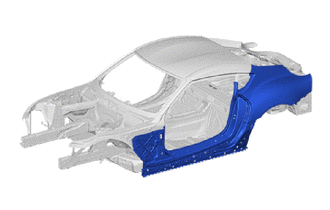
BODY PANEL ROCKER PANEL CUT AND JOIN REPLACEMENT SECTIONS
REMOVE THE HEMMING LOCATION
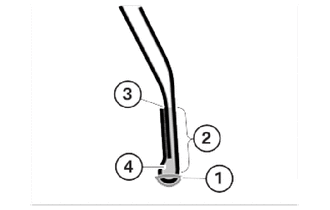
Grind down the flange edge (1) with an angle grinder with a roughing wheel.
Heat the adhesive flange (2) with a hot air blower.
- NOTICE:
-
Do not exceed the maximum object temperature of 250°C.
Use pliers or a chisel to peel off the components.
- NOTICE:
-
Do not damage adjacent components.
Remove the sealant in the area (3).
Remove adhesive residue (4) from the adhesive flange.
REMOVAL
| Symbol Meaning | |
|---|---|

|
Remove Weld Points |

|
Remove Weld Points |

|
Remove Weld Points |

|
Cut and Join Location |
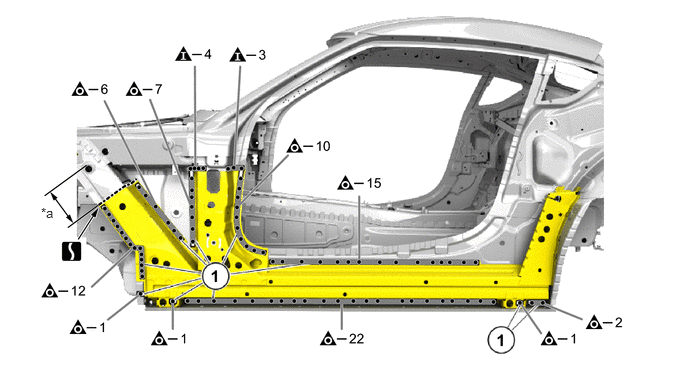
Mark and perform the separating cuts to match the specified dimensions.
- NOTICE:
-
Thereby disconnect only the outer panel.
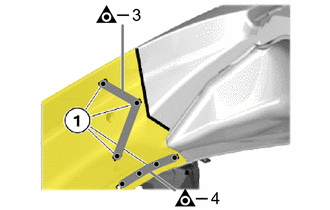
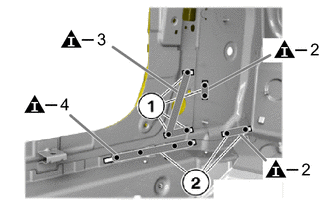
Remove the welding points in areas (1).
Remove the adhesive in area (2).
Remove the weld points and adhesive in area (3).
Remove the hemming location in area (4).
Remove the side panel sub-assy outer from the foamed sealing material in areas (5).
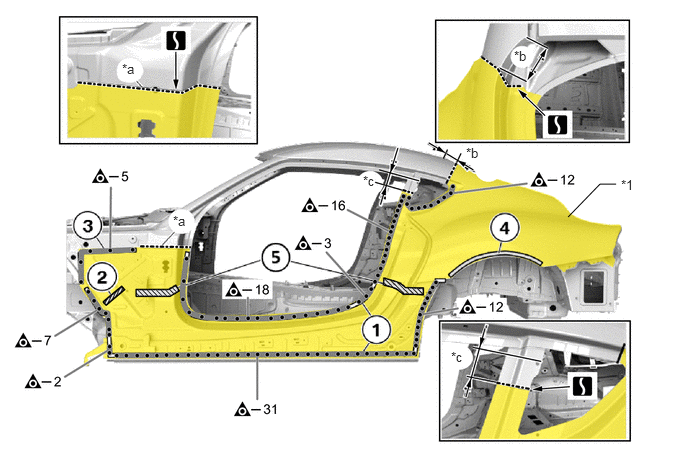
| *1 | SIDE PANEL SUB-ASSY OUTER | - | - |
| *a | centre of hole | *b | 130 mm (5.12 in.) from the corner of the outer left side frame |
| *c | 65 mm (2.56 in.) from the upper edge of the hole | - | - |

|
Adhesive | 
|
Foamed Sealing Material |
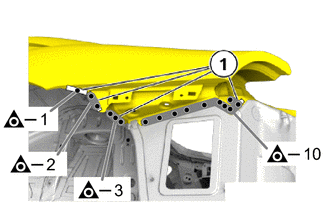
Remove the welding points in areas (1).
Remove the welding points in areas (1).
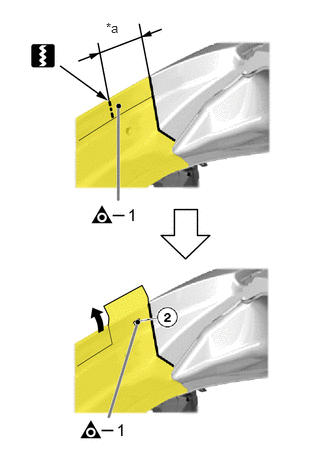
| *a | 70 mm (2.76 in.) |
Remove the welding points in areas (2).
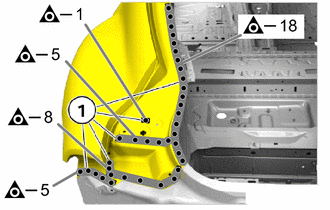
Remove the welding points in areas (1).
Remove the front side panel outer.
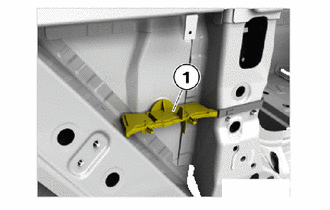
Remove the remaining foamed sealing material (1) from the vehicle side.
Remove the welding points in areas (1).
| *a | 120 mm (4.72 in.) | - | - |
Remove the welding points in areas (1) and (2).
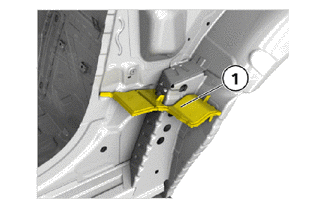
Remove the foamed sealing material (1).
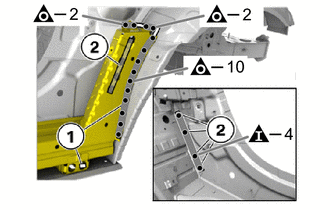
Remove the welding points in areas (1) and (2).
Prepare new part
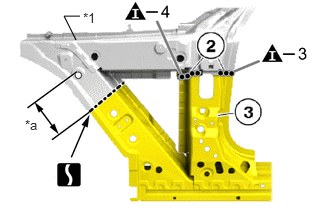
| *1 | SIDE PANEL SUB-ASSY NO.1 |
| *a | 120 mm (4.72 in.) |
Remove the welding points in areas (2).
Remove (3) from the new parts of side panel sub-assy No.1.
Prepare the new parts for the joining repair method by welding.
Adjust the new part as an assembly consisting of the side panel sub-assy No.1.
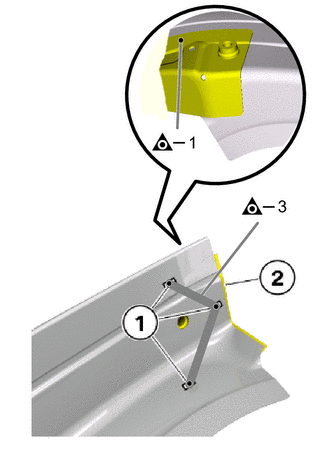
Remove the welding points in areas (1).
Remove a section of the (2).
INSTALLING THE FOAMED SEALING MATERIAL
- HINT:
- ·
Schematic diagram is for example purposes.
·Some parts may differ in certain details.
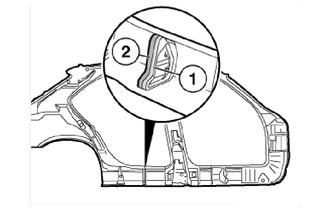
Sand the contact surface of the foamed sealing material (1) with sandpaper (#50-100).
Clean the contact surface (1) with the cleaner R2.
- Expendable materials:
Cleaner R2 500ml 08879-WA010
On the contact surface (1), apply an approximately 15 mm (0.59 in.) bead (2) of brushable seam seal. If necessary apply a slightly thinner bead of brushable seam seal on each side, to prevent the sealant from running.
- Expendable materials:
Brushable Seam Seal 310ml 08826-WA230
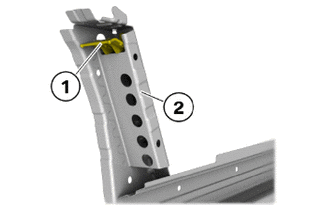
Apply brushable seam seal on the inner bottom B-pillar foamed sealing material (1).
Install foamed sealing material (1) in the B-pillar reinforcement (2).
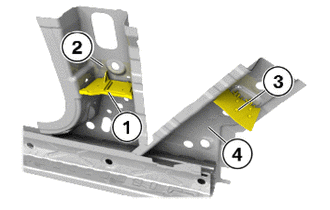
Apply brushable seam seal on the bottom rear A-pillar foamed sealing material (1).
Install bottom rear A-pillar foamed sealing material (1) in the bottom A-pillar reinforcement (2).
Install wheel arch carrier support foamed sealing material (3) in the rear wheel arch carrier support (4).
Remove existing cavity protection wax in the repair area with cavity protection wax remover.
- Expendable materials:
Cavity Wax Remover 500ml, Spray bottle 08830-WA010
INSTALLATION
| Symbol Meaning | |
|---|---|

|
Plug Weld |

|
Plug Weld |

|
Butt Weld |
Apply brushable seam seal to the foamed sealing material for the carrier support of the wheel arch(1).
Apply brushable seam seal on the bottom front A-pillar foamed sealing material (2).
Apply brushable seam seal on the inner bottom B-pillar foamed sealing material (3).
Position reinforcement of left side sill, align it and fix it with locking pliers.
Weld the cowl side panel sub-assy in the areas (4).
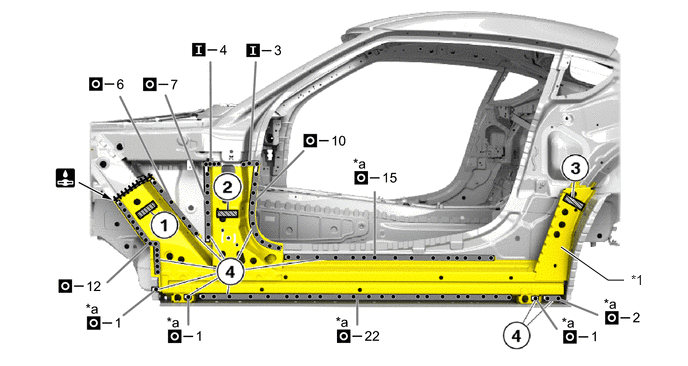
| *1 | COWL SIDE PANEL SUB-ASSY | - | - |
| *a | Ultra High Strength Steel Welding Point | - | - |
|
|
Foamed Sealing Material | - | - |
When welding 2 panels together including 980 MPa ultra high strength steel.
| *a: Plug weld | Plug diameter | 8 mm (0.31 in.) |
| Wire type | AWS A5.18 ER70S-3 | |
| Shield gas | Metal active gas |
- NOTICE:
-
Be sure to use Metal active gas (Ar 80% + CO2 20%) as the shield gas when plug welding.Sufficient weld strength cannot be assured when using 100% CO2 shield gas.
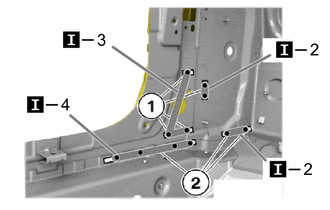
Weld the cowl side panel sub-assy in the areas (1) and (2).
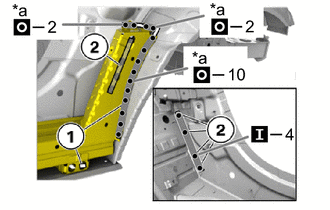
| *a | Ultra High Strength Steel Welding Point |
Weld the cowl side panel sub-assy in the areas (1) and (2).
When welding 2 panels together including 980 MPa ultra high strength steel.
| Plug weld | Plug diameter | 8 mm (0.31 in.) |
| Wire type | AWS A5.18 ER70S-3 | |
| Shield gas | Metal active gas |
- NOTICE:
-
Be sure to use Metal active gas (Ar 80% + CO2 20%) as the shield gas when plug welding.Sufficient weld strength cannot be assured when using 100% CO2 shield gas.
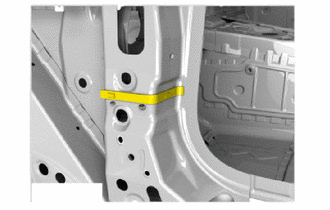
Apply brushable seam seal on the A-pillar shaped part.
Apply brushable seam seal on the outer bottom B-pillar foamed sealing material (1).
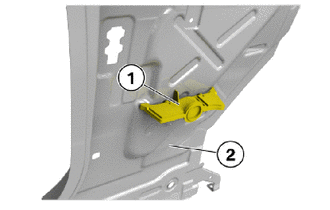
Apply brushable seam seal on the bottom front A-pillar foamed sealing material (1).
Install bottom front A-pillar foamed sealing material (1) in the outer side frame (2).
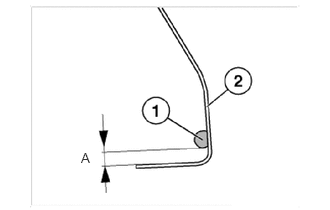
| A | 5 mm (0.20 in.) |
Apply adhesive (1) to the new part in the area (2) of the wheel arch.
- Adhesive:
K1 Bodywork Adhesive 195ml 08833-WA210
Apply adhesive (1) on the inside of the side panel at a distance (A).
Weld the side panel sub-assy outer in the areas (1), (3) and (4).
- NOTICE:
-
When using welds to attach panels that were previously attached using adhesive, it must be welded by plug welding (MAG welding), no adhesive should be applied. The number of plug welds (MAG welding) must be doubled compared to the original welding points on the adhesive applied areas.
- HINT:
- ·
Apply brushable seam seal to the foamed sealing material in the areas (2).
·Align the front side panel outer in the areas of the separating cuts (1) and (4) and secure it with vise grip.
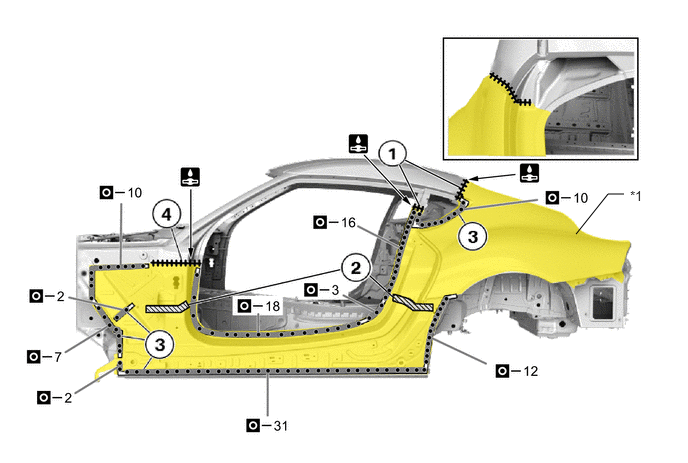
| *1 | SIDE PANEL SUB-ASSY OUTER | - | - |
|
|
Foamed Sealing Material | - | - |
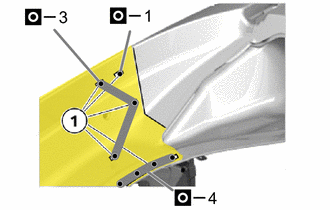
Weld the side panel sub-assy outer in the areas (1).
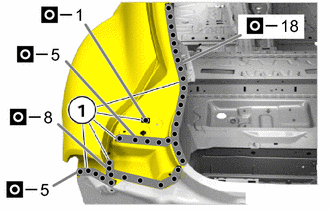
Weld the side panel sub-assy outer in the areas (1).
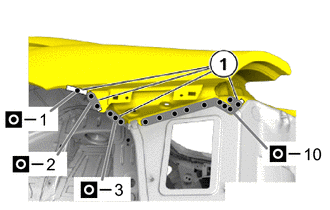
Weld the side panel sub-assy outer in the areas (1).
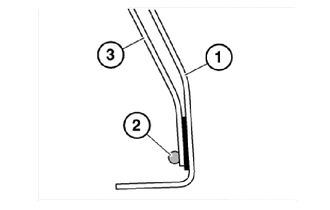
Apply adhesive (2) above the side panel (1) on the outer wheel arch section (3).
- Adhesive:
K1 Bodywork Adhesive 195ml 08833-WA210
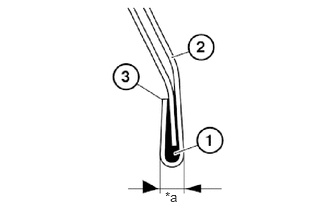
| *a | 5 mm (0.20 in.) |
Flange the edge of wheel arch (3) of the side panel (2) flush to the outer wheel arch section.
- NOTICE:
-
Do not create sharp edges when flanging as otherwise the flange edge may begin to tear.
Fully fill flange edge (1) with adhesive.
- Adhesive:
K1 Bodywork Adhesive 195ml 08833-WA210
Seal the area of the edge of wheel arch (3) with seam seal.
- Expendable materials:
Seam Seal 310ml 08826-WA220
After welding, apply body sealer and undercoating to the corresponding parts. (See the painting/coating)
After applying the top coat, apply anti-rust agent to the internal panel portion of the closed section structural weld points.