BODY PANEL REAR FLOOR SIDE MEMBER ASSEMBLY REPLACEMENT
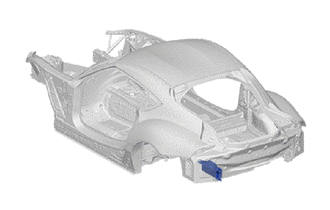
With the body lower back panel assembly removed.
REMOVAL
| Symbol Meaning | |
|---|---|

|
Remove Weld Points |

|
Remove Weld Points |

|
Remove Weld Points |

|
Cut and Join Location |

|
Cut Location |
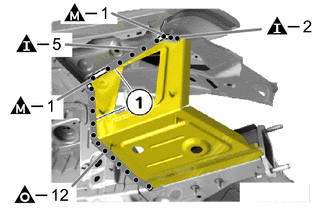
Remove the weld points in areas (1).
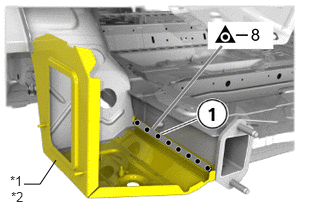
| *1 | REAR FLOOR PAN EXTENSION (LH) |
| *2 | REAR FLOOR SIDE PANEL EXTENSION (RH) |
Remove the weld points in areas (1).
Remove the rear floor pan extension or rear floor side panel extension.
- HINT:
-
To provide a better overview: Side panel omitted for clarity.
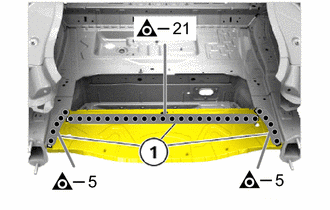
Remove the weld points in areas (1).
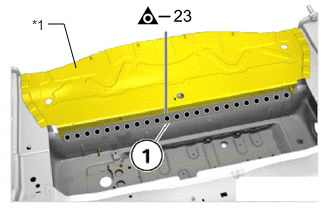
| *1 | REAR FLOOR PANEL REAR |
Remove the weld points in areas (1).
Remove the rear floor panel rear.
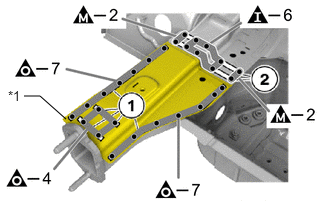
| *1 | REAR FLOOR SIDE MEMBER REAR |
Remove the weld points in areas (1) and (2).
Remove the rear floor side member rear.
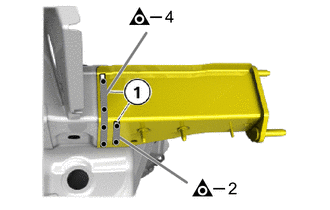
Remove the weld points in areas (1).
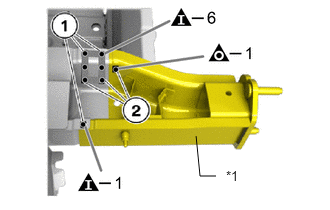
| *1 | REAR FLOOR SIDE MEMBER REINFORCE SUB-ASSY REAR |
Remove the weld points in areas (1) and (2).
Remove the rear floor side member reinforce sub-assy rear.
INSTALLATION
| Symbol Meaning | |
|---|---|

|
Plug Weld |

|
Plug Weld |

|
Plug Weld |
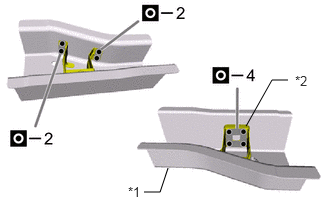
| *1 | REAR FLOOR SIDE MEMBER REINFORCE SUB-ASSY REAR |
| *2 | REAR SUSPENSION MEMBER MOUNTING BRACKET SUB-ASSY RR |
Adjust and fix rear floor side member rear in the lower section of the rear floor side member reinforce sub-assy rear.
Before temporarily installing the new parts, weld the rear floor side member reinforce sub-assy rear and rear suspension member mounting bracket sub-assy RR with the standard number of welding points.
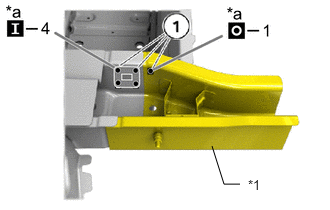
| *1 | REAR FLOOR SIDE MEMBER REINFORCE SUB-ASSY REAR |
| *a | Ultra High Strength Steel Welding Point |
Install and fix rear floor side member reinforce sub-assy rear.
Weld the rear floor side member reinforce sub-assy rear in the areas (1).
When welding 2 panels together including 780 MPa ultra high strength steel.
| Plug weld | Plug diameter | 8 mm (0.31 in.) |
| Wire type | AWS A5.18 ER70S-3 | |
| Shield gas | Metal active gas |
- NOTICE:
-
Be sure to use Metal active gas (Ar 80% + CO2 20%) as the shield gas when plug welding.Sufficient weld strength cannot be assured when using 100% CO2 shield gas.
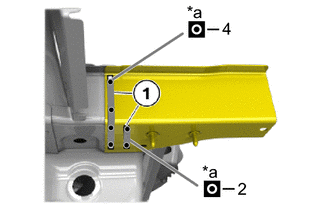
| *a | Ultra High Strength Steel Welding Point |
Weld the rear floor side member reinforce sub-assy rear in the areas (1).
When welding 2 panels together including 780 MPa ultra high strength steel.
| Plug weld | Plug diameter | 8 mm (0.31 in.) |
| Wire type | AWS A5.18 ER70S-3 | |
| Shield gas | Metal active gas |
- NOTICE:
-
Be sure to use Metal active gas (Ar 80% + CO2 20%) as the shield gas when plug welding.Sufficient weld strength cannot be assured when using 100% CO2 shield gas.
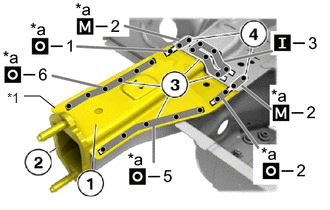
| *1 | REAR FLOOR SIDE MEMBER REAR |
| *a | Ultra High Strength Steel Welding Point |
Install, align and fix rear floor side member rear (1) and therear bumper arm support reinforce (2).
Weld the rear floor side member rear (1) in the areas (3) and (4).
When welding 2 panels together including 980 MPa ultra high strength steel.
| Plug weld | Plug diameter | 8 mm (0.31 in.) |
| Wire type | AWS A5.18 ER70S-3 | |
| Shield gas | Metal active gas |
- NOTICE:
-
Be sure to use Metal active gas (Ar 80% + CO2 20%) as the shield gas when plug welding.Sufficient weld strength cannot be assured when using 100% CO2 shield gas.
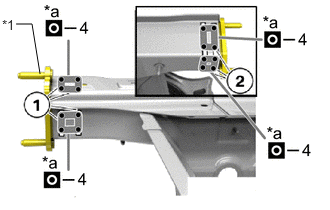
| *1 | REAR BUMPER ARM SUPPORT REINFORCE |
| *a | Ultra High Strength Steel Welding Point |
Weld the rear bumper arm support reinforce in the areas (1) and (2).
When welding 2 panels together including 980 MPa or 780 MPa ultra high strength steel.
| Plug weld | Plug diameter | 8 mm (0.31 in.) |
| Wire type | AWS A5.18 ER70S-3 | |
| Shield gas | Metal active gas |
- NOTICE:
-
Be sure to use Metal active gas (Ar 80% + CO2 20%) as the shield gas when plug welding.Sufficient weld strength cannot be assured when using 100% CO2 shield gas.
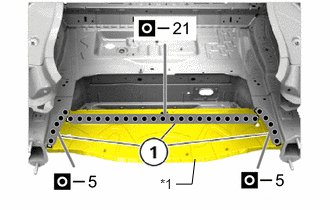
| *1 | REAR FLOOR PANEL REAR |
Install, adjust and secure the rear floor panel rear.
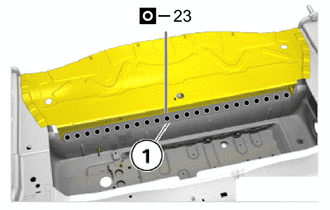
Weld the rear floor panel rear in the areas (1).
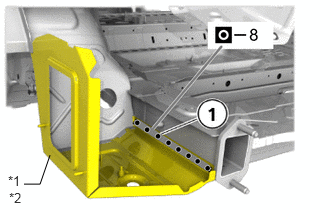
| *1 | REAR FLOOR PAN EXTENSION (LH) |
| *2 | REAR FLOOR SIDE PANEL EXTENSION (RH) |
Insert and secure rear floor pan extension or rear floor side panel extension from below.
Weld the rear floor pan extension or rear floor side panel extension in the area (1).
- HINT:
-
To provide a better overview: Shown without side panel and without tail panel.
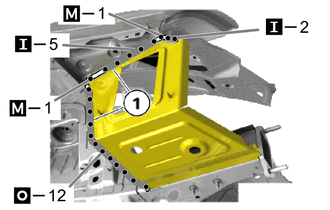
Weld the rear floor pan extension or rear floor side panel extension in the areas (1).
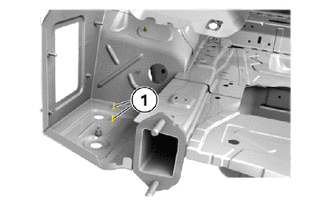
Weld coarse thread bolt (1) on the new part.
- HINT:
-
Take the quantity and position from the component to be replaced.
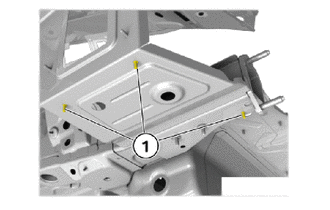
Weld coarse thread bolt (1) on the new part.
- HINT:
-
Take the quantity and position from the component to be replaced.
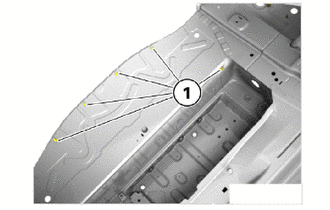
Weld coarse thread bolt (1) on the new part.
- HINT:
-
Take the quantity and position from the component to be replaced.
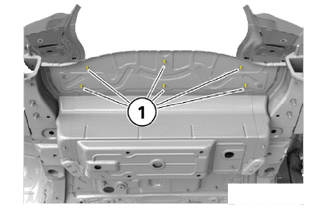
Weld coarse thread bolt (1) on the new part.
- HINT:
-
Take the quantity and position from the component to be replaced.
After welding, apply body sealer and undercoating to the corresponding parts. (See the painting/coating)
After applying the top coat, apply anti-rust agent to the internal panel portion of the closed section structural weld points.