BODY PANEL ROCKER REAR PANEL ASSEMBLY REPLACEMENT
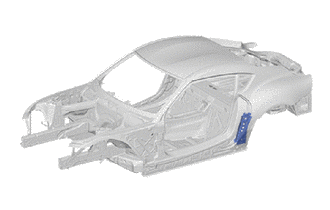
With the quarter panel cut and join replacement sections removed.
REMOVAL
| Symbol Meaning | |
|---|---|

|
Remove Weld Points |

|
Remove Weld Points |

|
Cut Location |
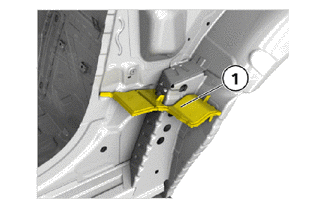
Remove the foamed sealing material (1).
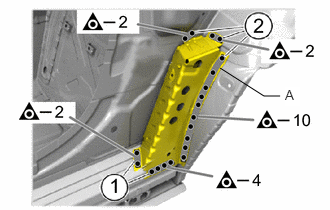
Remove the weld points in areas (1) and (2).
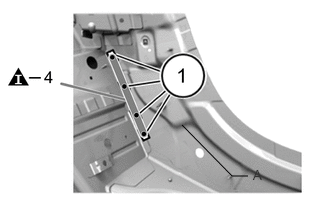
Remove the weld points in areas (1).
PREPARE NEW PART
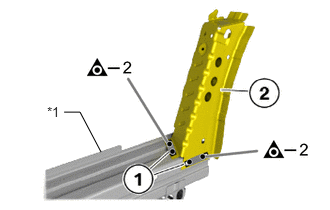
| *1 | COWL SIDE PANEL SUB-ASSY |
Remove the weld points in areas (1).
Remove (2) from the new parts of cowl side panel sub-assy.
Remove existing cavity protection wax in the repair area with cavity wax remover.
- Expendable materials:
Cavity Wax Remover 500ml, Spray bottle 08830-WA010
INSTALLING THE FOAMED SEALING MATERIAL (NOT EXPANDED)
- HINT:
- ·
Schematic diagram is for example purposes.
·Some parts may differ in certain details.
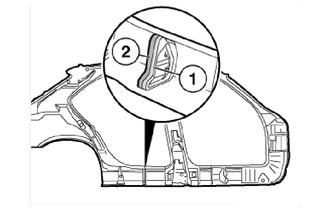
Sand the contact surface of the foamed sealing material (1) with sandpaper (#50-100).
Clean the contact surface (1) with the cleaner R2.
- Expendable materials:
Cleaner R2 500ml 08879-WA010
On the contact surface (1), apply an approximately 15 mm (0.59 in.) bead (2) of brushable seam seal. If necessary apply a slightly thinner bead of brushable seam seal on each side, to prevent the sealant from running.
- Expendable materials:
Brushable Seam Seal 310ml 08826-WA230
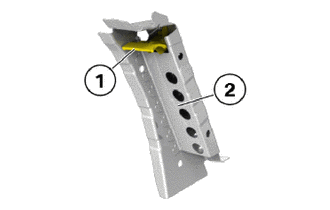
Apply brushable seam seal on the inner bottom B-pillar foamed sealing material (1).
Install inner bottom B-pillar foamed sealing material (1) in the B-pillar reinforcement (2).
INSTALLATION
| Symbol Meaning | |
|---|---|

|
Plug Weld |

|
Plug Weld |

|
Butt Weld |
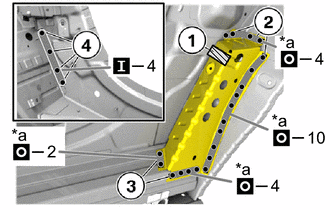
| *a | Ultra High Strength Steel Welding Point |

|
Foamed Sealing Material |
Apply brushable seam seal on the inner bottom B-pillar foamed sealing material (1).
Adjust and fix B-pillar reinforcement.
Weld B-pillar reinforcement in the areas (2), (3) and (4).
When welding 2 panels together including 980 MPa ultra high strength steel.
| Plug weld | Plug diameter | 8 mm (0.31 in.) |
| Wire type | AWS A5.18 ER70S-3 | |
| Shield gas | Metal active gas |
- NOTICE:
-
Be sure to use Metal active gas (Ar 80% + CO2 20%) as the shield gas when plug welding.Sufficient weld strength cannot be assured when using 100% CO2 shield gas.
Apply brushable seam seal on the foamed sealing material (1).
Install the foamed sealing material (1).