 |
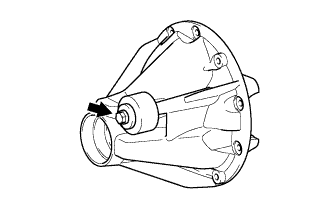
Install the dynamic damper and washer with the bolt.
- Torque:
- 17 N*m{ 168 kgf*cm , 12 ft.*lbf }
DIFFERENTIAL CARRIER ASSEMBLY (for 3UR-FE, 3UR-FBE) > REASSEMBLY |
| 1. INSTALL REAR DIFFERENTIAL DYNAMIC DAMPER (for Regular Cab Standard Deck) |
|
Install the dynamic damper and washer with the bolt.
| 2. INSTALL REAR DIFFERENTIAL DUST DEFLECTOR |
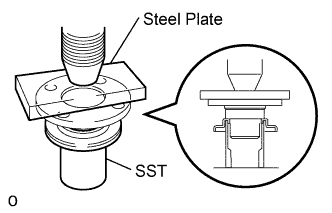 |
Using SST, a press and steel plate, press in the dust deflector.
| 3. INSTALL DIFFERENTIAL CASE ASSEMBLY |
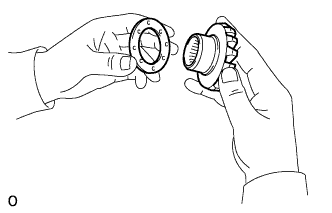 |
Install the 2 side gear thrust washers to the side gears.
Install the 2 side gears with the thrust washers, 2 pinion gears, 2 pinion gear thrust washers and pinion shaft.
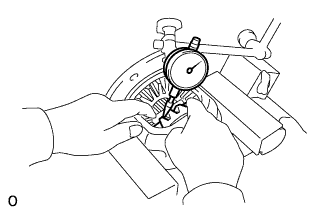 |
Using a dial indicator, measure the side gear backlash while holding one pinion gear toward the differential case.
| Thickness | Thickness |
| 1.53 to 1.57 mm (0.0602 to 0.0618 in.) | 1.78 to 1.82 mm (0.0701 to 0.0171 in.) |
| 1.58 to 1.62 mm (0.0622 to 0.0638 in.) | 1.83 to 1.87 mm (0.0720 to 0.0736 in.) |
| 1.63 to 1.67 mm (0.0642 to 0.0657 in.) | 1.88 to 1.92 mm (0.0740 to 0.0756 in.) |
| 1.68 to 1.72 mm (0.0661 to 0.0677 in.) | 1.93 to 1.97 mm (0.0760 to 0.0776 in.) |
| 1.73 to 1.77 mm (0.0681 to 0.0697 in.) | - |
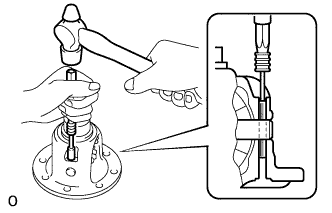 |
Using a pin punch and hammer, tap the straight pin through the holes in the differential case and pinion shaft.
Using a chisel and hammer, stake the outside of the differential case pin hole.
| 4. INSTALL REAR DIFFERENTIAL CASE BEARING |
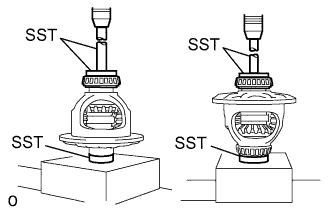 |
Using SST and a press, press in the 2 bearings.
| 5. INSTALL DIFFERENTIAL RING GEAR |
 |
Clean the contact surfaces of the differential case and ring gear.
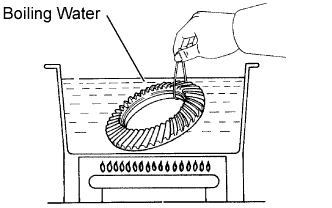
Heat the ring gear to approximately 100°C (212°F) in boiling water.
Carefully take the ring gear out of the boiling water.
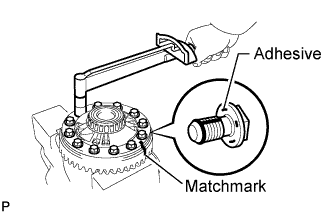 |
After the moisture on the ring gear has completely evaporated, quickly set the ring gear onto the differential case.
After the ring gear cools down sufficiently, apply adhesive to the bolts and install them.
| 6. INSTALL DIFFERENTIAL OIL STORAGE RING |
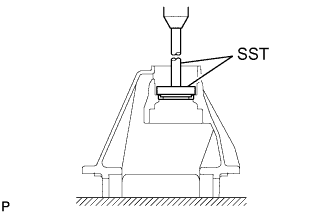 |
Using SST and a press, press in the oil storage ring to the differential carrier.
| 7. INSTALL REAR DRIVE PINION FRONT TAPERED ROLLER BEARING |
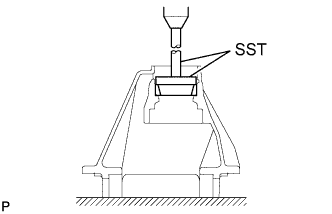 |
Using SST and a press, press in the bearing (outer race).
| 8. INSTALL REAR DRIVE PINION REAR TAPERED ROLLER BEARING |
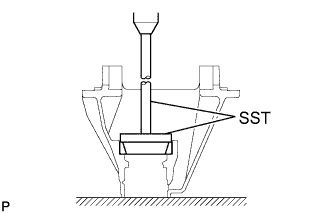 |
Using SST and a press, press in the bearing (outer race).
| 9. INSTALL REAR DRIVE PINION REAR TAPERED ROLLER BEARING |
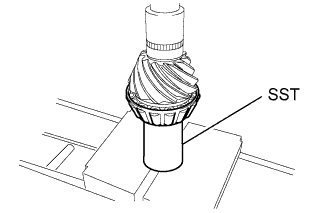 |
Install the plate washer onto the drive pinion.
Using SST and a press, press in the bearing.
| 10. INSPECT DIFFERENTIAL DRIVE PINION PRELOAD (with Shim Pairing Table) |
Install the bearing spacer onto the drive pinion.
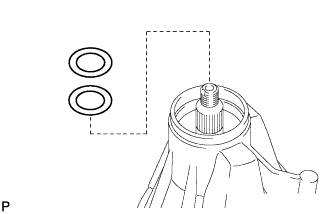 |
Install the 2 preload adjusting shims.
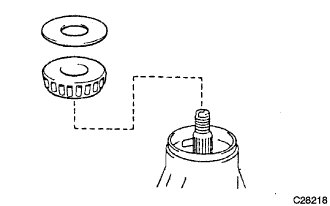 |
Install the front bearing (inner race) and oil slinger.
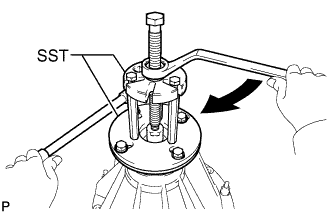 |
Using SST, install the companion flange.
Coat the threads of the nut with hypoid gear oil.
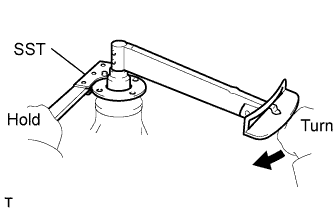 |
Using SST to hold the companion flange, install the nut by tightening it until the standard preload is reached.
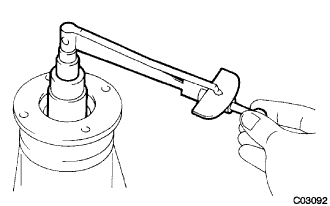 |
Using a torque wrench, measure the preload.
| Bearing | Specified Condition |
| New | 1.80 to 3.17 N*m (19 to 32 kgf*cm, 16 to 28 in.*lbf) |
| Reused | 1.62 to 2.25 N*m (17 to 22 kgf*cm, 15 to 19 in.*lbf) |
Refer to the table below and choose a combination of 2 shims.
| Shim A Thickness | Shim B Thickness |
| 1.89 to 1.91 mm (0.0745 to 0.0753 in.) | 1.792 to 1.808 mm (0.0706 to 0.0712 in.) |
| 1.99 to 2.01 mm (0.0784 to 0.0792 in.) | 1.802 to 1.818 mm (0.0710 to 0.0716 in.) |
| 2.09 to 2.11 mm (0.0823 to 0.0831 in.) | 1.812 to 1.828 mm (0.0714 to 0.0720 in.) |
| 2.19 to 2.21 mm (0.0863 to 0.0871 in.) | 1.822 to 1.838 mm (0.0718 to 0.0724 in.) |
| 2.29 to 2.31 mm (0.0902 to 0.0910 in.) | 1.832 to 1.848 mm (0.0722 to 0.0728 in.) |
| 2.39 to 2.41 mm (0.0942 to 0.0950 in.) | 1.842 to 1.858 mm (0.0726 to 0.0732 in.) |
| 2.49 to 2.51 mm (0.0981 to 0.0989 in.) | 1.852 to 1.868 mm (0.0730 to 0.0736 in.) |
| 2.59 to 2.61 mm (0.1020 to 0.1028 in.) | 1.862 to 1.878 mm (0.0734 to 0.0740 in.) |
| 2.69 to 2.71 mm (0.1060 to 0.1068 in.) | 1.872 to 1.888 mm (0.0738 to 0.0744 in.) |
| 2.79 to 2.81 mm (0.1099 to 0.1107 in.) | 1.882 to 1.898 mm (0.0742 to 0.0748 in.) |
| 2.89 to 2.91 mm (0.1139 to 0.1147 in.) | - |
| 2.99 to 3.01 mm (0.1178 to 0.1186 in.) | - |
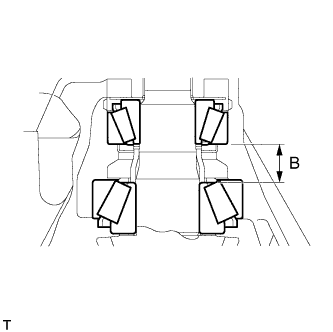 |
Calculate the B measurement.
| Measurement |
| 24.15 to 24.20 mm (0.9515 to 0.9535 in.) |
| Shim A Thickness | Shim B Thickness | B Measurement |
| 1.89 to 1.91 mm (0.0745 to 0.0753 in.) | 1.792 to 1.808 mm (0.0706 to 0.0712 in.) | 27.832 to 27.918 mm (1.0966 to 1.1000 in.) |
| ↑ | 1.802 to 1.818 mm (0.0710 to 0.0716 in.) | 27.842 to 27.928 mm (1.0970 to 1.1004 in.) |
| ↑ | 1.812 to 1.828 mm (0.0714 to 0.0720 in.) | 27.852 to 27.938 mm (1.0974 to 1.1008 in.) |
| ↑ | 1.822 to 1.838 mm (0.0718 to 0.0724 in.) | 27.862 to 27.948 mm (1.0978 to 1.1012 in.) |
| ↑ | 1.832 to 1.848 mm (0.0722 to 0.0728 in.) | 27.872 to 27.958 mm (1.0982 to 1.1015 in.) |
| ↑ | 1.842 to 1.858 mm (0.0726 to 0.0732 in.) | 27.882 to 27.968 mm (1.0986 to 1.1019 in.) |
| ↑ | 1.852 to 1.868 mm (0.0730 to 0.0736 in.) | 27.892 to 27.978 mm (1.0989 to 1.1023 in.) |
| ↑ | 1.862 to 1.878 mm (0.0734 to 0.0740 in.) | 27.902 to 27.988 mm (1.0993 to 1.1027 in.) |
| ↑ | 1.872 to 1.888 mm (0.0738 to 0.0744 in.) | 27.912 to 27.998 mm (1.0997 to 1.1031 in.) |
| ↑ | 1.882 to 1.898 mm (0.0742 to 0.0748 in.) | 27.922 to 28.008 mm (1.1001 to 1.1035 in.) |
| 1.99 to 2.01 mm (0.0784 to 0.0792 in.) | 1.792 to 1.808 mm (0.0706 to 0.0712 in.) | 27.932 to 28.018 mm (1.1005 to 1.1039 in.) |
| ↑ | 1.802 to 1.818 mm (0.0710 to 0.0716 in.) | 27.942 to 28.028 mm (1.1009 to 1.1043 in.) |
| ↑ | 1.812 to 1.828 mm (0.0714 to 0.0720 in.) | 27.952 to 28.038 mm (1.1013 to 1.1047 in.) |
| For these in-between values, combine shim A, B and the spacer as above so that the B measurement changes at 0.01 mm (0.000394 in.) intervals. | 27.962 to 28.048 mm (1.1017 to 1.1051 in.) to 29.012 to 29.098 mm (1.1431 to 1.1465 in.) | |
| 2.99 to 3.01 mm (0.1178 to 0.1186 in.) | 1.882 to 1.898 mm (0.0742 to 0.0748 in.) | 29.022 to 29.108 mm (1.1435 to 1.1469 in.) |
Measure the preload.
Change the shims so that the B measurement changes by 0.01 mm (0.000394 in.), and measure the preload.
| Bearing | Specified Condition |
| New | 1.80 to 3.17 N*m (19 to 32 kgf*cm, 16 to 28 in.*lbf) |
| Reused | 1.62 to 2.25 N*m (17 to 22 kgf*cm, 15 to 19 in.*lbf) |
| 11. INSTALL REAR DIFFERENTIAL CASE ASSEMBLY |
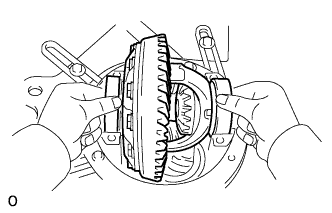 |
Place the 2 bearing outer races on their corresponding bearings.
Install the differential case assembly in the differential carrier assembly.
| 12. ADJUST RING GEAR BACKLASH |
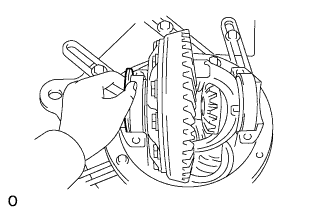 |
Install the plate washer on the ring gear back side.
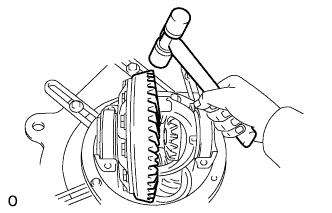 |
Tap on the ring gear with a plastic-faced hammer so that the washer fits to the bearing.
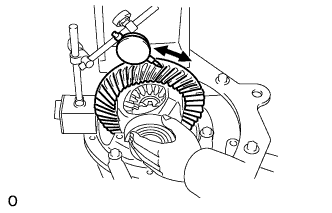 |
Using a dial indicator, while holding the companion flange, measure the ring gear backlash.
|
Select a ring gear back side plate washer using the backlash as a reference.
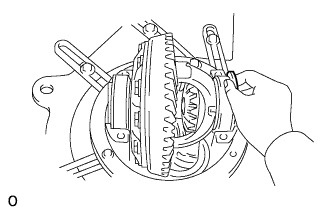 |
Select a ring gear teeth side plate washer so that there is no clearance between the outer race and case.
Remove the 2 plate washers and differential case.
Install the plate washer on the ring gear back side.
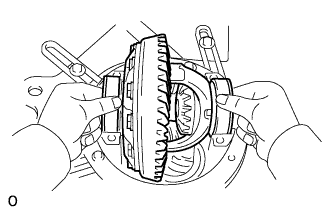 |
Place the other plate washer onto the differential case together with the outer race, and install the differential case with the outer race into the carrier.
Tap on the ring gear with a plastic-faced hammer so that the washers fit to the bearing.
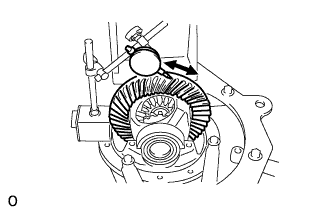 |
Using a dial indicator, while holding the companion flange, measure the ring gear backlash.
| 13. ADJUST SIDE BEARING PRELOAD |
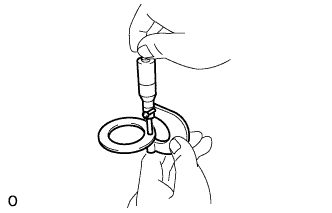 |
Remove the ring gear teeth side plate washer and using a micrometer, measure the thickness.
Install the selected plate washer.
Using the backlash as a reference, tap a new washer that is 0.05 to 0.20 mm (0.00197 to 0.00787 in.) thicker than the removed washer so that it fits to the bearing.
Using a plastic-faced hammer, install the plate washer.
|
Recheck the ring gear backlash.
| Mark | Thickness | Mark | Thickness |
| 66 | 1.65 to 1.67 mm (0.0650 to 0.0658 in.) | 08 | 2.07 to 2.09 mm (0.0816 to 0.0823 in.) |
| 68 | 1.67 to 1.69 mm (0.0658 to 0.0666 in.) | 10 | 2.09 to 2.11 mm (0.0823 to 0.0831 in.) |
| 70 | 1.69 to 1.71 mm (0.0666 to 0.0674 in.) | 12 | 2.11 to 2.13 mm (0.0831 to 0.0839 in.) |
| 72 | 1.71 to 1.73 mm (0.0674 to 0.0682 in.) | 14 | 2.13 to 2.15 mm (0.0839 to 0.0847 in.) |
| 74 | 1.73 to 1.75 mm (0.0682 to 0.0690 in.) | 16 | 2.15 to 2.17 mm (0.0847 to 0.0855 in.) |
| 76 | 1.75 to 1.77 mm (0.0690 to 0.0697 in.) | 18 | 2.17 to 2.19 mm (0.0855 to 0.0863 in.) |
| 78 | 1.77 to 1.79 mm (0.0697 to 0.0705 in.) | 20 | 2.19 to 2.21 mm (0.0863 to 0.0871 in.) |
| 80 | 1.79 to 1.81 mm (0.0705 to 0.0713 in.) | 22 | 2.21 to 2.23 mm (0.0871 to 0.0879 in.) |
| 82 | 1.81 to 1.83 mm (0.0713 to 0.0721 in.) | 24 | 2.23 to 2.25 mm (0.0879 to 0.0887 in.) |
| 84 | 1.83 to 1.85 mm (0.0721 to 0.0729 in.) | 26 | 2.25 to 2.27 mm (0.0887 to 0.0894 in.) |
| 86 | 1.85 to 1.87 mm (0.0729 to 0.0737 in.) | 28 | 2.27 to 2.29 mm (0.0894 to 0.0902 in.) |
| 88 | 1.87 to 1.89 mm (0.0737 to 0.0745 in.) | 30 | 2.29 to 2.31 mm (0.0902 to 0.0891 in.) |
| 90 | 1.89 to 1.91 mm (0.0745 to 0.0753 in.) | 32 | 2.31 to 2.33 mm (0.0910 to 0.0918 in.) |
| 92 | 1.91 to 1.93 mm (0.0753 to 0.0760 in.) | 34 | 2.33 to 2.35 mm (0.0918 to 0.0926 in.) |
| 94 | 1.93 to 1.95 mm (0.0760 to 0.0768 in.) | 36 | 2.35 to 2.37 mm (0.0926 to 0.0934 in.) |
| 96 | 1.95 to 1.97 mm (0.0768 to 0.0776 in.) | 38 | 2.37 to 2.39 mm (0.0934 to 0.0942 in.) |
| 98 | 1.97 to 1.99 mm (0.0776 to 0.0784 in.) | 40 | 2.39 to 2.41 mm (0.0942 to 0.0950 in.) |
| 00 | 1.99 to 2.01 mm (0.0784 to 0.0792 in.) | 42 | 2.41 to 2.43 mm (0.0950 to 0.0957 in.) |
| 02 | 2.01 to 2.03 mm (0.0792 to 0.0800 in.) | 44 | 2.43 to 2.45 mm (0.0957 to 0.0965 in.) |
| 04 | 2.03 to 2.05 mm (0.0800 to 0.0808 in.) | 46 | 2.45 to 2.47 mm (0.0965 to 0.0973 in.) |
| 06 | 2.05 to 2.07 mm (0.0808 to 0.0816 in.) | - | - |
| 14. INSTALL BEARING CAP |
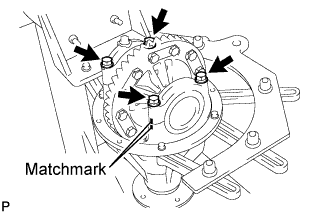 |
Align the matchmarks on the cap and carrier.
Install the 4 bolts.
| 15. INSPECT DIFFERENTIAL RING GEAR RUNOUT |
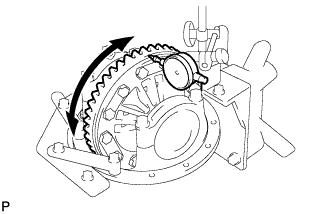 |
Using a dial indicator, measure the runout of the ring gear.
| 16. INSPECT TOTAL PRELOAD |
|
Using a torque wrench, measure the preload with the teeth of the drive pinion and ring gear in contact.
| Bearing | Specified Condition |
| New | Standard drive pinion preload plus 0.22 to 0.41 N*m (3 to 4 kgf*cm, 2 to 3 in.*lbf) |
| Reused | Standard drive pinion preload plus 0.19 to 0.38 N*m (2 to 3 kgf*cm, 2 to 3 in.*lbf) |
| 17. INSPECT TOOTH CONTACT BETWEEN RING GEAR AND DRIVE PINION |
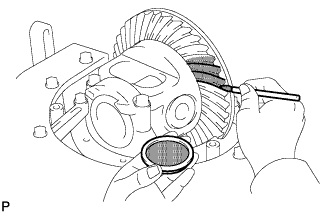 |
Coat 3 or 4 teeth at 3 different positions on the ring gear with Prussian blue.
Turn the companion flange in both directions to inspect the ring gear for proper tooth contact.
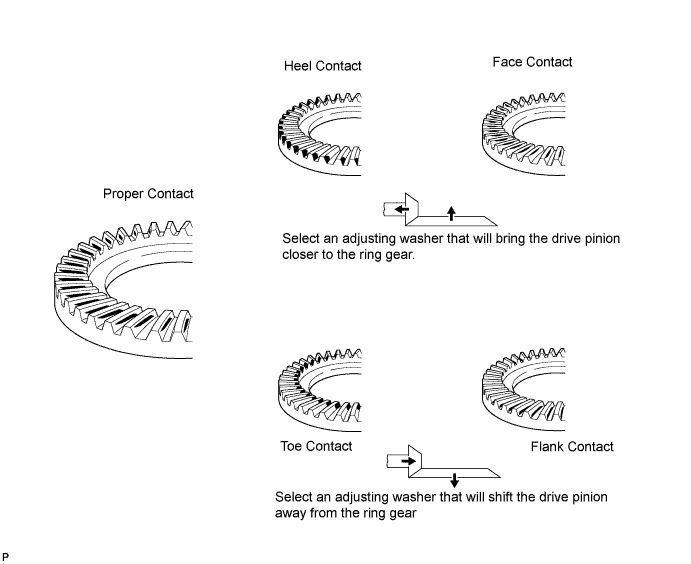
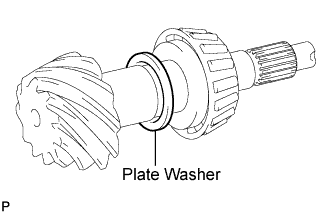 |
| Thickness | Thickness |
| 0.99 to 1.01 mm (0.0390 to 0.398 in.) | 1.265 to 1.285 mm (0.0498 to 0.0506 in.) |
| 1.015 to 1.035 mm (0.0399 to 0.0408 in.) | 1.29 to 1.31 mm (0.0508 to 0.0516 in.) |
| 1.04 to 1.06 mm (0.0410 to 0.0418 in.) | 1.315 to 1.335 mm (0.0518 to 0.0526 in.) |
| 1.065 to 1.085 mm (0.0409 to 0.0427 in.) | 1.34 to 1.36 mm (0.0528 to 0.0536 in.) |
| 1.09 to 1.11 mm (0.0420 to 0.0437 in.) | 1.365 to 1.385 mm (0.0538 to 0.0546 in.) |
| 1.115 to 1.135 mm (0.0429 to 0.0447 in.) | 1.39 to 1.41 mm (0.0548 to 0.0556 in.) |
| 1.14 to 1.16 mm (0.0439 to 0.0457 in.) | 1.415 to 1.435 mm (0.0558 to 0.0565 in.) |
| 1.165 to 1.185 mm (0.0449 to 0.0467 in.) | 1.44 to 1.46 mm (0.0567 to 0.0575 in.) |
| 1.19 to 1.21 mm (0.0469 to 0.0477 in.) | 1.465 to 1.485 mm (0.0577 to 0.0585 in.) |
| 1.215 to 1.235 mm (0.0479 to 0.0487 in.) | 1.49 to 1.51 mm (0.0587 to 0.0595 in.) |
| 1.24 to 1.26 mm (0.0489 to 0.0496 in.) | - |
| 18. REMOVE REAR DRIVE PINION NUT |
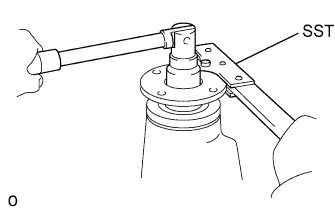 |
Using SST to hold the companion flange, remove the nut.
| 19. REMOVE REAR DRIVE PINION COMPANION FLANGE SUB-ASSEMBLY |
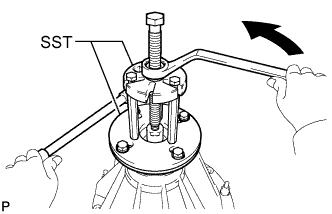 |
Using SST, remove the companion flange.
| 20. INSTALL REAR DIFFERENTIAL CARRIER OIL SEAL |
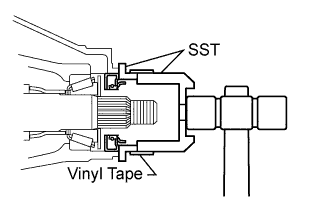 |
Using SST and a plastic-faced hammer, tap in a new oil seal until its surface is flush with the differential carrier end.
Coat the lip of the oil seal with MP grease.
| 21. INSTALL REAR DRIVE PINION COMPANION FLANGE SUB-ASSEMBLY |
|
Using SST, install the companion flange.
Coat the threads of a new nut with hypoid gear oil.
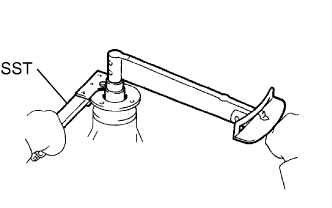 |
Using SST to hold the flange, install the nut.
| 22. INSPECT DIFFERENTIAL DRIVE PINION PRELOAD |
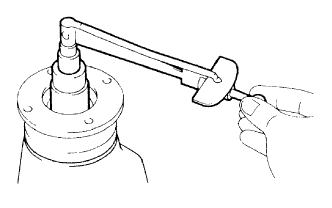 |
Using a torque wrench, measure the preload of the backlash between the drive pinion and ring gear.
| Bearing | Specified Condition |
| New | 1.80 to 3.17 N*m (19 to 32 kgf*cm, 16 to 28 in.*lbf) |
| Reused | 1.62 to 2.25 N*m (17 to 22 kgf*cm, 15 to 20 in.*lbf) |
| 23. INSPECT TOTAL PRELOAD |
|
Using a torque wrench, measure the preload with the teeth of the drive pinion and ring gear in contact.
| Bearing | Specified Condition |
| New | Standard drive pinion preload plus 0.22 to 0.41 N*m (3 to 4 kgf*cm, 2 to 3 in.*lbf) |
| Reused | Standard drive pinion preload plus 0.19 to 0.38 N*m (2 to 3 kgf*cm, 2 to 3 in.*lbf) |
| 24. INSPECT DIFFERENTIAL RING GEAR BACKLASH |
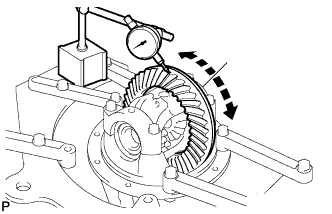 |
Using a dial indicator, check the backlash of the ring gear.
| 25. INSPECT RUNOUT OF REAR DRIVE PINION COMPANION FLANGE SUB-ASSEMBLY |
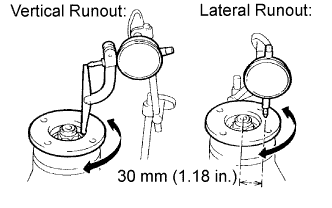 |
Using a dial indicator, measure the runout of the companion flange vertically and laterally.
| Runout | Specified Condition |
| Vertical runout | 0.1 mm (0.00394 in.) |
| Lateral runout | 0.1 mm (0.00394 in.) |
| 26. STAKE REAR DRIVE PINION NUT |
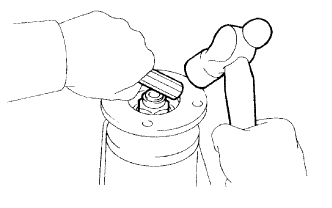 |
Using a chisel and hammer, stake the nut.