GEAR-PINION/RING
REMOVAL
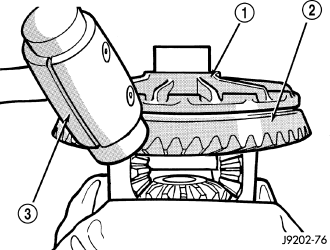
NOTE: The ring gear and pinion are serviced as a matched set. Never replace ring gear without replacing the matched pinion gear.
1. Remove differential from axle housing.
2. Place differential case (1) in a vise with soft jaws.
3. Remove bolts holding ring gear to differential case.
4. Driver ring gear (2) off the differential case (1) with a dead-blow hammer (3).
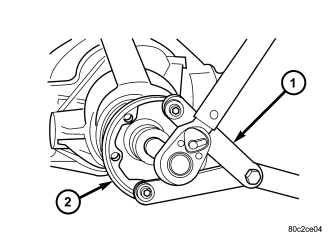
5. With Spanner Wrench 6958 (1) and a short length of 1 in. pipe, hold pinion companion flange (2) and remove pinion nut.
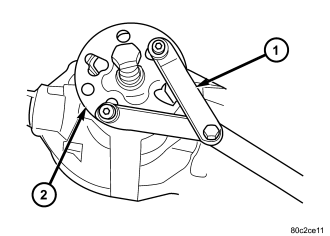
6. Remove pinion companion flange from pinion shaft with Spanner Wrench 6958 (1) and Puller C-452 (2).
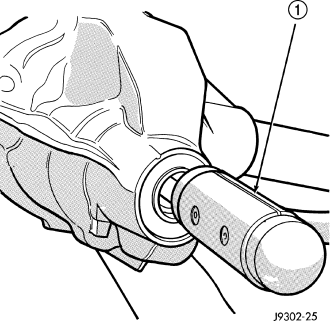
7. Remove pinion gear from housing with dead-blow hammer (1)..
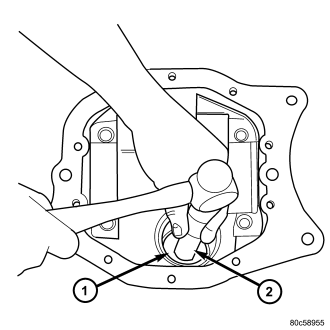
8. Remove front pinion bearing cup, bearing, oil slinger and pinion seal with Remover D-149 (1) and Handle C-4171 (2).
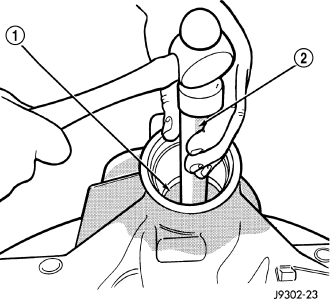
9. Remove rear pinion bearing cup with Remover C-4307 (1) and Handle C-4171 (2).
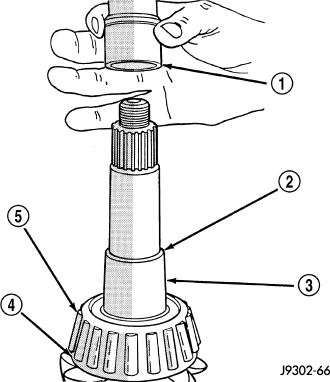
10. Remove collapsible spacer (1) from pinion gear (3).
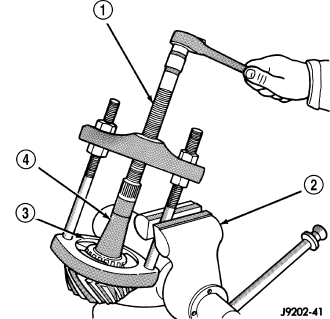
11. Remove rear pinion bearing from the pinion (4) with Puller/Press C-293-PA (1) and Adapters C-293-42 (3). Remove oil slinger/pinion depth shim from the pinion shaft and record thickness.
INSTALLATION
NOTE: Pinion depth shims are located under the rear pinion bearing. If ring and pinion gears are reused, the pinion oil slinger/depth shim should not require replacement. Refer to Adjustments (Pinion Gear Depth) to select the proper thickness shim before installing pinion gear.
1. Install front pinion bearing, and oil slinger if equipped.
2. Apply a light coating of gear lubricant on the lip of pinion seal and install seal with Installer 8681.
3. Apply Mopar Door Ease or equivalent lubricant to outside surface of pinion bearing cups.
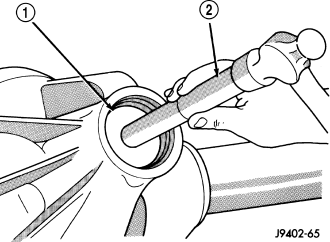
4. Install rear bearing cup with Installer C-4308 and Handle C-4171.
5. Install front bearing cup with Installer D-146 (1) and Handle C-4171 (1).
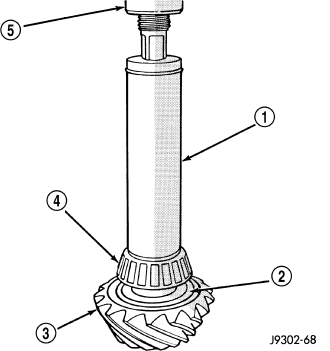
6. Install oil slinger/depth shim (2) and rear pinion bearing (4) on pinion shaft (3) with Installer 6448A (1) and a press (1).
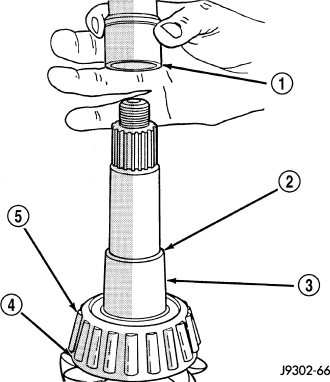
7. Install a new collapsible spacer (1) on pinion shaft (3) and install pinion into the housing.
8. Install pinion companion flange, with Installer W-162-D, Cup 8109 and Spanner Wrench 6958.
9. Install pinion a new nut onto the pinion gear and tighten the nut to 217 N·m (160 ft. lbs.). Do not over-tighten.
CAUTION: Never loosen pinion gear nut to decrease pinion rotating torque and never exceed specified preload torque. Failure to follow these instructions will result in damage.
10. Use Spanner Wrench 6958 (1), a length of 1 in. pipe and a torque wrench set at 678 N·m (500 ft. lbs.) and crush collapsible spacer until bearing end play is taken up.
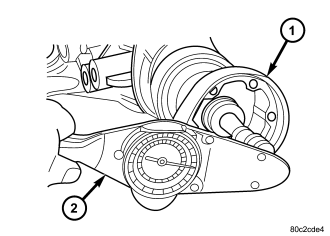
11. Slowly tighten the nut in 6.8 N·m (5 ft. lbs.) increments until the required rotating torque is achieved. Measure rotating torque frequently to avoid over crushing the collapsible spacer.
12. Rotate the pinion a minimum of ten times. Verify pinion (1) rotates smoothly and check rotating torque with an inch pound torque wrench (2). Pinion gear rotating torque is:
- Original Bearings: 1 - 2.2 N·m (10 - 20 in. lbs.).
- New Bearings: 1.7 - 2.8 N·m (15 - 25 in. lbs.).
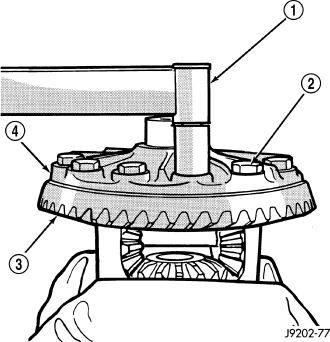
13. Invert differential case and start two ring gear bolts. This will provide case-to-ring gear bolt hole alignment.
14. Invert differential case (4) in the vise. Install new ring gear (3) bolts (2) and alternately tighten to 108 N·m (80 ft. lbs.).
CAUTION: Never reuse the ring gear bolts. Failure to follow these instructions will result in damage.
15. Install differential in housing.
16. Measure Total Torque to Rotate (TTR) with an inch pound torque wrench. This will verify the correct differential bearing preload.
Total Torque to Rotate is, pinion torque to rotate plus:
- Gear Ratio 3.55: 0.48 - 0.78 N·m (4.2 - 6.9 in. lbs.)
- Gear Ratio 3.73: 0.45 - 0.75 N·m (3.9 - 6.6 in. lbs.)
If TTR is high, decrease shim thickness equally on both sides of the differential and check TTR again. If TTR is low, increase shim thickness equally on both sides of the differential and check TTR again.
17. Verify differential gear contact pattern.