14B ENGINE MECHANICAL CYLINDER BLOCK CRANKSHAFT INSPECTION AND REPAIR
PROCEDURE

 1.INSPECT CRANKSHAFT FOR RUNOUT
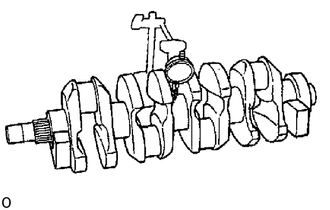
Place the crankshaft on V-blocks.
Using a dial indicator, measure the circle runout at the center journal.
- Maximum circle runout:
0.08 mm (0.0031 in.)
If the circle runout is greater than maximum, replace the crankshaft.
2.INSPECT MAIN JOURNALS AND CRANK PINS
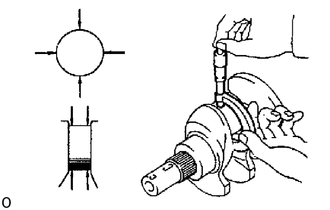
Using a micrometer, measure the diameter of each main journal and crank pin.
- Main journal diameter:
STD No.3 69.950 - 69.970 mm (2.7539 - 2.7547 in.) Others 69.980 - 70.000 mm (2.7551 - 2.7559 in.) U/S 0.25 No.3 69.710 - 69.720 mm (2.7445 - 2.7449 in.) Others 69.740 - 69.750 mm (2.7457 - 2.7461 in.) U/S 0.50 No.3 69.460 - 69,470 mm (2.7346 - 2.7350 in.) Others 69.490 - 69.500 mm (2.7358 - 2.7362 in.) U/S 1.00 No.3 68.960 - 68.970 mm (2.7150 - 2.7153 in.) Others 68.990 - 69.000 mm (2.7161 - 2.7165 in.)
- Crank pin diameter:
STD 60.980 - 61.000 mm (2.4008 - 2.4016 in.) U/S 0.25 60.740 - 60.750 mm (2.3913 - 2.3917 in.) U/S 0.50 60.490 - 60.500 mm (2.3815 - 2.3819 in.) U/S 1.00 59.990 - 60.000 mm (2.3618 - 2.3622 in.)
If the diameter is not as specified, check the oil clearance.
Click hereEngine / Hybrid System>14B (ENGINE MECHANICAL)>CYLINDER BLOCK>CYLINDER BLOCK ASSEMBLY
If necessary, grind or replace the crankshaft.
Check each main journal and crank pin for taper and out-of-round as shown.
- Maximum taper and out-of-round:
0.020 mm (0.0008 in.)
If the taper and out-of-round is greater than maximum, replace the crankshaft.
3. IF NECESSARY, GRIND AND HONE MAIN JOURNALS AND/OR CRANK PINS
Grind and hone the main journals and/or crank pins to the finished undersized diameter.
Install new main journal and/or crankshaft pin undersized bearing.