REASSEMBLY
Removal / installation · Vehicles built from Aug 2009
Versions by build date: Jul 2007 – Jul 2009 from Aug 2009
| 1. ASSEMBLE DIFFERENTIAL CASE |

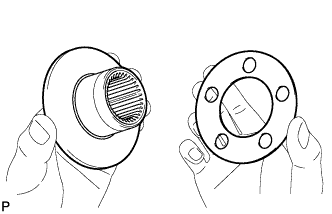  |
Install the rear differential side gear thrust washer onto the rear differential side gear.
Install the rear differential pinion thrust washer and rear differential pinion onto the rear differential spider.
Fix the differential case RH.
Install the rear differential side gear and rear differential spider onto the differential case RH.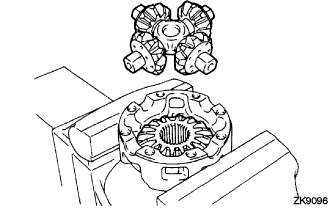
Using a dial indicator, measure the differential case RH side backlash while holding the pinion toward the case.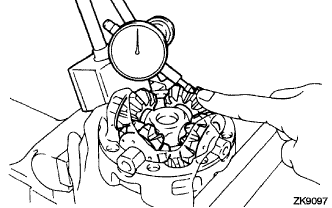
- Backlash:
- 0.05 to 0.20 mm (0.002 to 0.008 in.)
Remove the rear differential spider from the differential case RH.
Install the rear differential side gear and rear differential spider onto the differential case LH.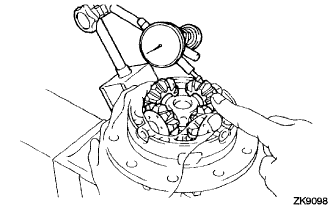
Using a dial indicator, measure the differential case LH side backlash while holding the pinion toward the case.
- Backlash:
- 0.05 to 0.20 mm (0.002 to 0.008 in.)
- Thrust Washer Thickness:
Thickness
Thickness
0.87 to 0.93 mm (0.0343 to 0.0366 in.)
1.17 to 1.23 mm (0.0461 to 0.0484 in.)
0.97 to 1.03 mm (0.0382 to 0.0406 in.)
1.27 to 1.33 mm (0.0500 to 0.0524 in.)
1.07 to 1.13 mm (0.0421 to 0.0445 in.)
-
Align the matchmarks and assemble the RH and LH cases.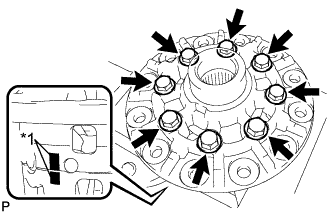
Text in Illustration *1
Matchmark
Using a plastic hammer, install the differential case.
Install the 8 bolts.
- Torque:
- 47 N*m{ 480 kgf*cm , 35 ft.*lbf }
| 2. INSTALL DIFFERENTIAL RING GEAR |
 |
| *1 |
Boiling Water |
Clean the contact surfaces of the differential case and ring gear.
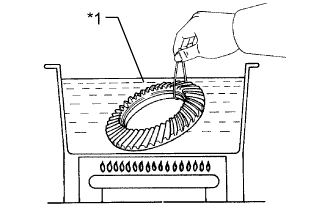
Heat the ring gear in water that is approximately 100°C (212°F).
Carefully remove the ring gear from the boiling water.
After the moisture on the ring gear has completely evaporated, quickly install the ring gear onto the differential case.
Align the matchmarks on the ring gear with those of the differential case.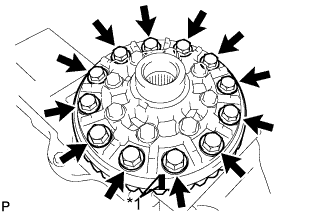
Text in Illustration *1
Matchmark
After the ring gear cools down sufficiently, apply adhesive to the 12 bolts and install them.
- Adhesive:
- Toyota Genuine Adhesive 1360K, Three Bond 1360K or equivalent
- Torque:
- 97 N*m{ 985 kgf*cm , 71 ft.*lbf }
| 3. INSTALL REAR DIFFERENTIAL CASE BEARING |
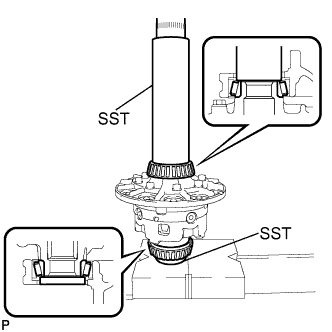 |
Using SST and a press, press the bearing onto the differential case.
- SST
- 09308-14010
09950-60010 (09951-00490)
| 4. INSPECT DIFFERENTIAL RING GEAR RUNOUT |
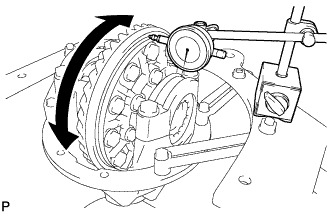 |
Install the differential case on the carrier, and install the 2 plate washers so that there is no play in the bearing.
Install the 2 bearing caps with the 4 bolts.
- Torque:
- 103 N*m{ 1049 kgf*cm , 76 ft.*lbf }
Using a dial indicator, measure the runout of the ring gear.
- Maximum runout:
- 0.07 mm (0.0028 in.)
Remove the 2 bearing caps, 2 plate washers and the differential case.
| 5. INSTALL REAR DRIVE PINION FRONT TAPERED ROLLER BEARING |
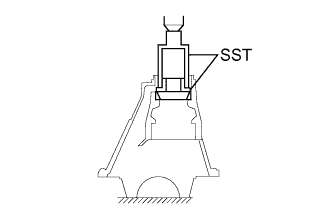 |
Using SST and a press, press in the roller bearing (outer) to the carrier.
- SST
- 09308-14010
09309-14040
| 6. INSTALL REAR DRIVE PINION REAR TAPERED ROLLER BEARING |
Install the plate washer onto the carrier.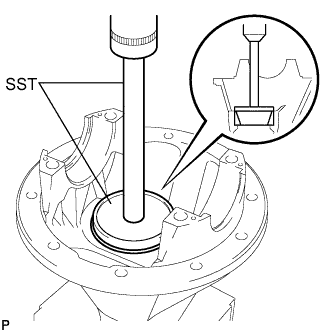
- HINT:
- First fit a washer with the same thickness as the removed washer, and then check the tooth contact pattern. Replace the washer with one of a different thickness if necessary.
Using SST and a press, press the roller bearing (outer) into the carrier.
- SST
- 09950-70010
(09951-07200)
09255-10012
| 7. INSTALL REAR DRIVE PINION REAR TAPERED ROLLER BEARING |
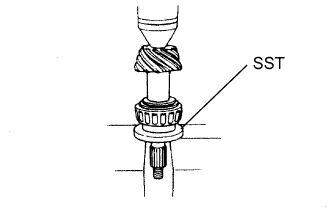 |
Using SST and a press, press the roller bearing (inner) onto the drive pinion.
- SST
- 09309-14040
| 8. ADJUST DIFFERENTIAL DRIVE PINION PRELOAD |
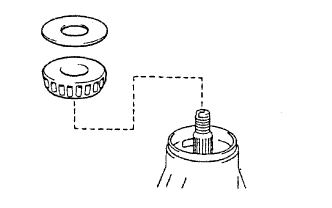 |
Install the drive pinion, rear drive pinion tapered roller bearing and rear differential drive pinion oil slinger.
- HINT:
- Assemble the spacer and oil seal after adjusting the gear contact pattern.
Using SST, install the companion flange.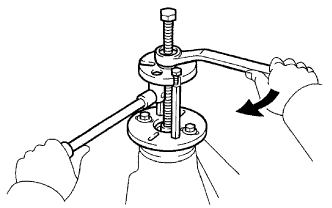
- SST
- 09950-30012
(09951-03010, 09953-03010, 09954-03010, 09955-03030, 09956-03040)
- NOTICE:
- Before using SST (center bolt), apply hypoid gear oil to its threads and tip.
Using a socket wrench (30 mm), adjust the drive pinion preload by tightening the companion flange nut.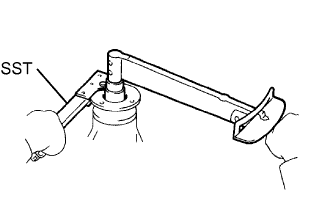
Using SST to hold the companion flange in place, torque the nut.
- SST
- 09330-00021
- Torque:
- 457 N*m{ 4660 kgf*cm , 337 ft.*lbf } or less
- NOTICE:
- As there is no spacer, torque a little at a time. Be careful not to overtighten the nut.
- As there is no spacer, torque a little at a time. Be careful not to overtighten the nut.
- Apply hypoid gear oil to the nut.
- Apply hypoid gear oil to the nut.
Using a torque wrench, measure the preload.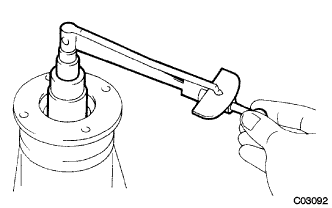
- Preload (at starting):
Bearing
Standard
New bearing
0.83 to 2.18 N*m (8.64 to 22.2 kgf*cm, 7.35 to 19.3 in.*lbf)
Used bearing
0.88 to 1.98 N*m (8.97 to 20.2 kgf*cm, 7.79 to 17.5 in.*lbf)
- NOTICE:
- For a more accurate measurement, rotate the bearing forward and backward several times before measuring.
| 9. INSTALL DIFFERENTIAL CASE ASSEMBLY |
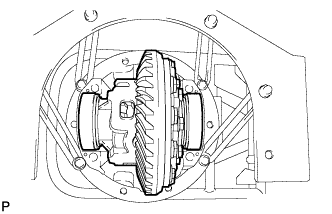 |
Place the 2 bearing outer races on their respective bearings.
- HINT:
- Do not interchange the right and left races.
| 10. ADJUST RING GEAR BACKLASH |
Install the plate washer on the ring gear back side.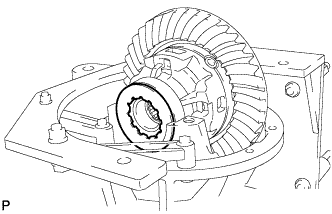
- NOTICE:
- Make sure that ring gear has backlash.
Using a dial indicator, while housing the companion flange, measure the ring gear backlash.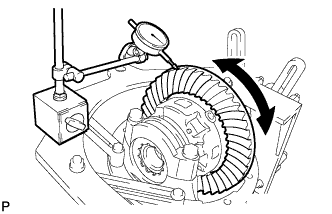
- Standard backlash (reference) :
- 0.10 to 0.20 mm (0.00394 to 0.00787 in.)
Select a ring gear back side plate washer using the backlash as reference.
Select a ring gear teeth side plate washer so that there is no clearance between the outer race and case.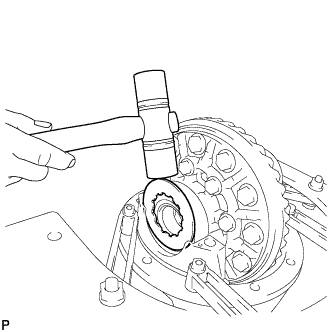
Using a plastic-faced hammer, install the ring gear teeth side plate washer.
Using a dial indicator, while holding the companion flange, measure the ring gear backlash.
- Standard backlash:
- 0.10 to 0.20 mm (0.00394 to 0.00787 in.)
- HINT:
- There should be no clearance between the plate washer and the case. Make sure that there is ring gear backlash.
| 11. ADJUST SIDE BEARING PRELOAD |
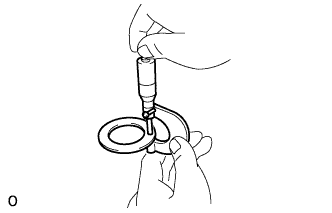 |
Remove the ring gear teeth side plate washer and using a micrometer, measure the thickness.
Install the selected plate washer.
Using the backlash as a reference, tap a new washer that is 0.05 to 0.20 mm (0.00197 to 0.00787 in.) thicker than the removed washer so that it fits to the bearing.
- HINT:
- Select a washer which can be pressed in 2/3 of the full amount with your finger.
Using a plastic-faced hammer, install the plate washer.
Recheck the ring gear backlash.
- Standard backlash:
- 0.10 to 0.20 mm (0.00394 to 0.00787 in.)
- HINT:
- The backlash will change by about 0.02 mm (0.000787 in.), corresponding to a 0.03 mm (0.00118 in.) change in the plate washer.
Washer thickness Mark
Thickness
Mark
Thickness
70
2.05 to 2.07 mm (0.0808 to 0.0816 in.)
62
2.41 to 2.43 mm (0.0950 to 0.0957 in.)
71
2.07 to 2.09 mm (0.0816 to 0.0823 in.)
63
2.43 to 2.45 mm (0.0957 to 0.0965 in.)
72
2.09 to 2.11 mm (0.0823 to 0.0831 in.)
64
2.45 to 2.47 mm (0.0965 to 0.0973 in.)
73
2.11 to 2.13 mm (0.0831 to 0.0839 in.)
65
2.47 to 2.49 mm (0.0972 to 0.0980 in.)
74
2.13 to 2.15 mm (0.0839 to 0.0847 in.)
66
2.49 to 2.51 mm (0.0980 to 0.0988 in.)
75
2.15 to 2.17 mm (0.0847 to 0.0855 in.)
67
2.51 to 2.53 mm (0.0988 to 0.0996 in.)
76
2.17 to 2.19 mm (0.0855 to 0.0863 in.)
68
2.53 to 2.55 mm (0.0996 to 0.1000 in.)
77
2.19 to 2.21 mm (0.0863 to 0.0871 in.)
69
2.55 to 2.57 mm (0.1000 to 0.1012 in.)
78
2.21 to 2.23 mm (0.0871 to 0.0879 in.)
01
2.57 to 2.59 mm (0.1012 to 0.1020 in.)
79
2.23 to 2.25 mm (0.0879 to 0.0887 in.)
32
2.59 to 2.61 mm (0.1020 to 0.1028 in.)
80
2.25 to 2.27 mm (0.0887 to 0.0894 in.)
33
2.61 to 2.63 mm (0.1028 to 0.1035 in.)
81
2.27 to 2.29 mm (0.0894 to 0.0902 in.)
03
2.63 to 2.65 mm (0.1035 to 0.1043 in.)
82
2.27 to 2.31 mm (0.0902 to 0.0891 in.)
34
2.65 to 2.67 mm (0.1043 to 0.1051in.)
83
2.31 to 2.33 mm (0.0910 to 0.0918 in.)
35
2.67 to 2.69 mm (0.1051 to 0.1059 in.)
84
2.33 to 2.35 mm (0.0918 to 0.0926 in.)
05
2.69 to 2.71 mm (0.1059 to 0.1067 in.)
85
2.35 to 2.37 mm (0.0926 to 0.0934 in.)
36
2.71 to 2.73 mm (0.1067 to 0.1075 in.)
86
2.37 to 2.39 mm (0.0934 to 0.0942 in.)
37
2.73 to 2.75 mm (0.1075 to 0.1082 in.)
87
2.39 to 2.41 mm (0.0942 to 0.0950 in.)
07
2.75 to 2.77 mm (0.1082 to 0.1091 in.)
| 12. INSTALL BEARING CAP |
Align the matchmarks on the cap and carrier.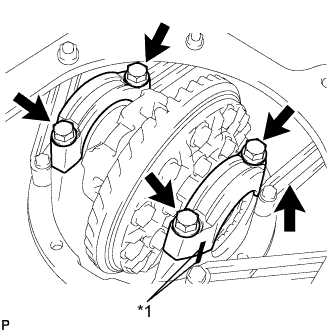
Text in Illustration *1
Matchmark
Install the 4 bolts.
- Torque:
- 103 N*m{ 1049 kgf*cm , 76 ft.*lbf }
- HINT:
- After rotating the ring gear 5 times or more, recheck the backlash.
| 13. INSPECT DIFFERENTIAL RING GEAR RUNOUT |
Using a dial indicator, measure the runout of the ring gear.
- Standard runout:
- 0.07 mm (0.0028 in.)
| 14. INSPECT TOTAL PRELOAD |
|
|
Using a torque wrench, measure the preload with the teeth of the drive pinion and ring gear in contact.
- Total preload (at starting):
- Drive pinion preload plus 0.20 to 0.40 N*m (2.0 to 4.1 kgf*cm, 1.8 to 3.5 in.*lbf)
| 15. INSPECT TOOTH CONTACT BETWEEN RING GEAR AND DRIVE PINION |
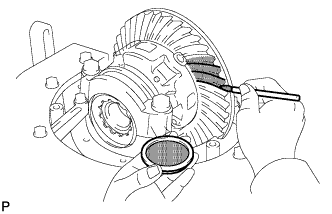 |
Coat 3 or 4 teeth at 3 different positions on the ring gear with Prussian blue.
Hold the companion flange firmly in place and rotate the ring gear in both directions.
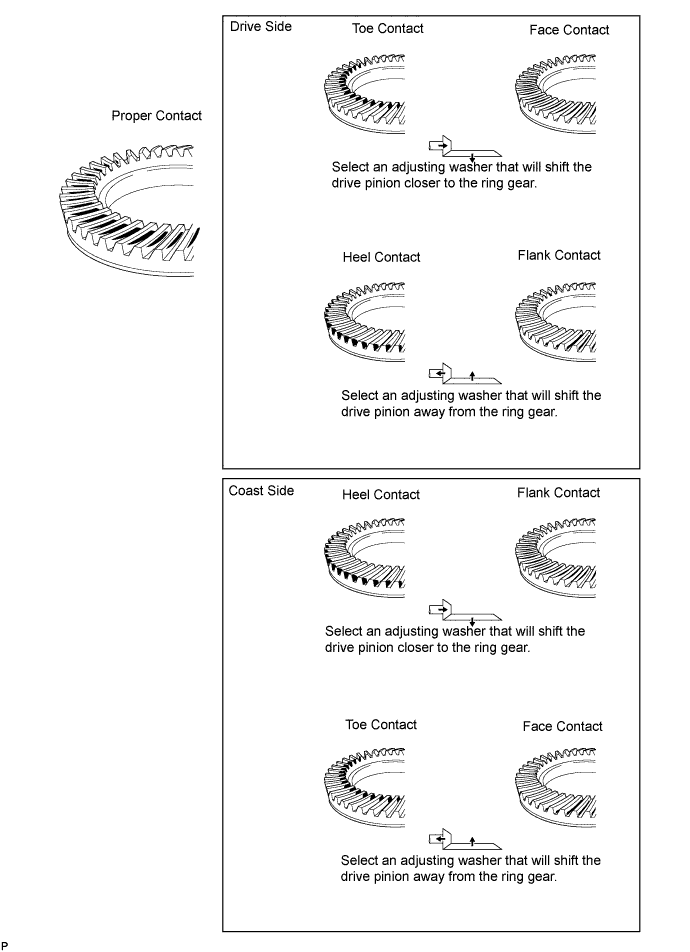
Inspect the tooth contact pattern.
-
-
If the teeth are not engaged properly, use the following chart to select a proper washer.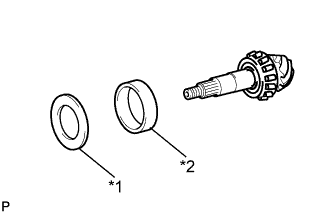
Text in Illustration *1
Plate Washer
*2
Rear Drive Pinion Rear Tapered Roller Bearing (Outer)
Plate Washer Thickness Thickness mm (in.)
Thickness mm (in.)
1.845 to 1.855 (0.0726 to 0.0730)
2.085 to 2.095 (0.0821 to 0.0825)
1.855 to 1.865 (0.0730 to 0.0734)
2.095 to 2.105 (0.0825 to 0.0829)
1.865 to 1.875 (0.0734 to 0.0738)
2.105 to 2.115 (0.0829 to 0.0833)
1.875 to 1.885 (0.0738 to 0.0742)
2.115 to 2.125 (0.0833 to 0.0837)
1.885 to 1.895 (0.0742 to 0.0746)
2.125 to 2.135 (0.0837 to 0.0841)
1.895 to 1.905 (0.0746 to 0.0750)
2.135 to 2.145 (0.0841 to 0.0844)
1.905 to 1.915 (0.0750 to 0.0754)
2.145 to 2.155 (0.0844 to 0.0848)
1.915 to 1.925 (0.0754 to 0.0758)
2.155 to 2.165 (0.0848 to 0.0852)
1.925 to 1.935 (0.0758 to 0.0762)
2.165 to 2.175 (0.0852 to 0.0856)
1.935 to 1.945 (0.0762 to 0.0766)
2.175 to 2.185 (0.0856 to 0.0860)
1.945 to 1.955 (0.0766 to 0.0770)
2.185 to 2.195 (0.0860 to 0.0864)
1.955 to 1.965 (0.0770 to 0.0774)
2.195 to 2.205 (0.0864 to 0.0868)
1.965 to 1.975 (0.0774 to 0.0778)
2.205 to 2.215 (0.0868 to 0.0872)
1.975 to 1.985 (0.0778 to 0.0781)
2.215 to 2.225 (0.0872 to 0.0876)
1.985 to 1.995 (0.0781 to 0.0785)
2.225 to 2.235 (0.0876 to 0.0880)
1.995 to 2.005 (0.0785 to 0.0789)
2.235 to 2.245 (0.0880 to 0.0884)
2.005 to 2.015 (0.0789 to 0.0793)
2.245 to 2.255 (0.0884 to 0.0888)
2.015 to 2.025 (0.0793 to 0.0797)
2.255 to 2.265 (0.0888 to 0.0892)
2.025 to 2.035 (0.0797 to 0.0801)
2.265 to 2.275 (0.0892 to 0.0896)
2.035 to 2.045 (0.0801 to 0.0805)
2.275 to 2.285 (0.0896 to 0.0900)
2.045 to 2.055 (0.0805 to 0.0809)
2.285 to 2.295 (0.0900 to 0.0904)
2.055 to 5.065 (0.0809 to 0.0813)
2.295 to 2.305 (0.0904 to 0.0907)
2.065 to 2.075 (0.0813 to 0.0817)
2.305 to 2.315 (0.0907 to 0.0911)
2.075 to 2.085 (0.0817 to 0.0821)
-
-
| 16. REMOVE REAR DRIVE PINION NUT |
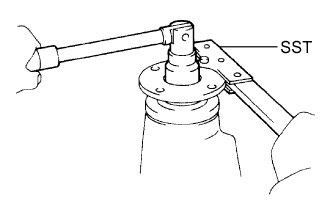 |
Using SST to hold the companion flange in place, remove the nut.
- SST
- 09330-00021
| 17. REMOVE REAR DRIVE PINION COMPANION FLANGE SUB-ASSEMBLY |
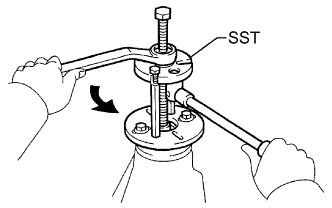 |
Using SST, remove the rear drive pinion companion flange sub-assembly.
- SST
- 09950-30012
(09951-03010, 09953-03010, 09954-03010, 09955-03030, 09956-03040)
- NOTICE:
- Before using SST (center bolt), apply hypoid gear oil to its threads and tip.
| 18. REMOVE REAR DIFFERENTIAL DRIVE PINION OIL SLINGER |
| 19. REMOVE REAR DRIVE PINION FRONT TAPERED ROLLER BEARING |
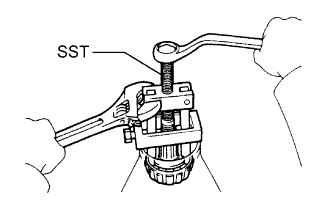 |
Using SST, remove the rear drive pinion front tapered roller bearing (inner) from the drive pinion.
- SST
- 09556-22010
| 20. REMOVE REAR DRIVE PINION FRONT TAPERED ROLLER BEARING |
| 21. INSTALL REAR DIFFERENTIAL DRIVE PINION BEARING SPACER |
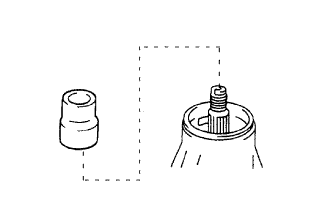 |
Install a new bearing spacer onto the drive pinion.
| 22. INSTALL DIFFERENTIAL OIL STORAGE RING |
Using SST, tap in a new oil storage ring.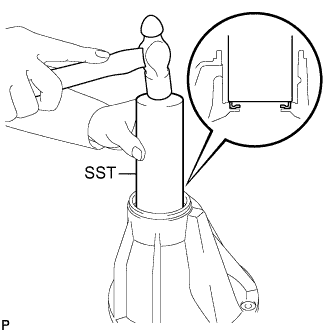
- SST
- 09308-14010
| 23. INSTALL REAR DRIVE PINION FRONT TAPERED ROLLER BEARING |
| 24. INSTALL REAR DIFFERENTIAL DRIVE PINION OIL SLINGER |
| 25. INSTALL REAR DIFFERENTIAL CARRIER OIL SEAL |
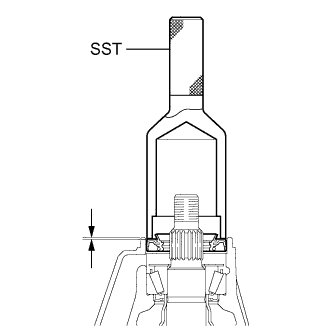 |
Apply MP grease to a new oil seal.
Using SST and a hammer, tap in the oil seal.
- SST
- 09214-76011
- Oil seal depth:
- -0.3 to 0.3 mm(-0.012 to 0.012)
| 26. INSTALL REAR DRIVE PINION COMPANION FLANGE SUB-ASSEMBLY |
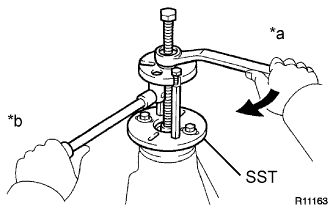 |
| *a |
Turn |
| *b |
Hold |
Using SST, install the companion flange onto the drive pinion.
- SST
- 09950-30012
(09951-03010, 09953-03010, 09954-03010, 09955-03030, 09956-03040)
- NOTICE:
- Before using SST (center bolt), apply hypoid gear oil to its threads and tip.
Coat the threads of a new nut with hypoid gear oil.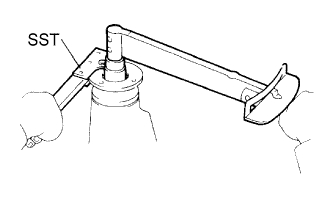
Using SST to hold the flange, torque the nut.
- SST
- 09330-00021
- Torque:
- 457 N*m{ 4660 kgf*cm , 337 ft.*lbf } or less
| 27. INSPECT DRIVE PINION PRELOAD |
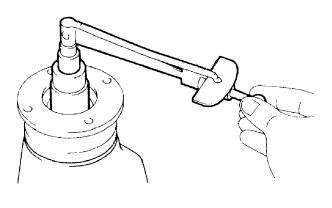 |
Using a torque wrench, measure the preload of the backlash between the drive pinion and ring gear.
- Preload (at starting):
Bearing
Standard
New bearing
0.83 to 2.18 N*m (8.64 to 22.2 kgf*cm, 7.35 to 19.3 in.*lbf)
Used bearing
0.88 to 1.98 N*m (8.97 to 20.2 kgf*cm, 7.79 to 17.5 in.*lbf)
- If the preload is greater than the maximum, replace the bearing spacer.
- If the preload is less than the minimum, retighten the nut with 13 N*m (130 kgf*cm, 9 ft.*lbf) of torque at a time until the specified preload is reached.
- Torque:
- 457 N*m{ 4660 kgf*cm , 337 ft.*lbf } or less
- If the maximum torque is exceeded while retightening the nut, replace the bearing spacer and repeat the preload adjusting procedure.
- HINT:
- Do not loosen the pinion nut to reduce the preload.
| 28. INSPECT TOTAL PRELOAD |
|
|
Using a torque wrench, measure the preload.
- HINT:
- Bolt without torque specifications are shown in the service data (Click here).
- If necessary, disassemble and inspect the differential.
| 29. INSPECT DIFFERENTIAL RING GEAR BACKLASH |
|
|
Using a dial indicator, check the backlash of the ring gear.
- Standard backlash:
- 0.10 to 0.20 mm (0.00394 to 0.00787 in.)
- If the backlash is not as specified, adjust the side bearing preload or repair as necessary.
- HINT:
- Perform the measurements at 3 or more positions around the circumference of the ring gear.
| 30. INSPECT RUNOUT OF REAR DRIVE PINION COMPANION FLANGE SUB-ASSEMBLY |
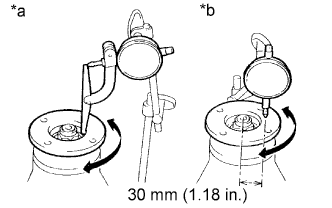 |
| *a |
Vertical Runout |
| *b |
Lateral Runout |
Using a dial indicator, measure the runout of the drive pinion companion flange vertically and laterally.
- Maximum Runout:
Runout
Maximum
Vertical runout
0.14 mm (0.0055 in.)
Lateral runout
0.14 mm (0.0055 in.)
- If the runout is greater than the maximum, replace the companion flange.
| 31. STAKE DRIVE PINION NUT |
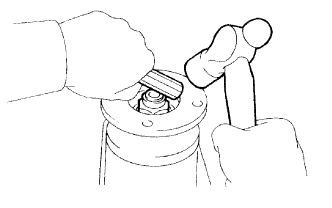 |
Using a chisel and hammer, stake the nut.