BODY WELD POINT FRAME AUXILIARY CROSSMEMBER ASSEMBLY REPLACEMENT
w/o Winch
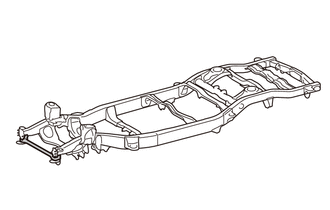
With the frame side rail plate removed.
REMOVAL
| Symbol Meaning | |
|---|---|

|
Cut with Disc Sander etc. |
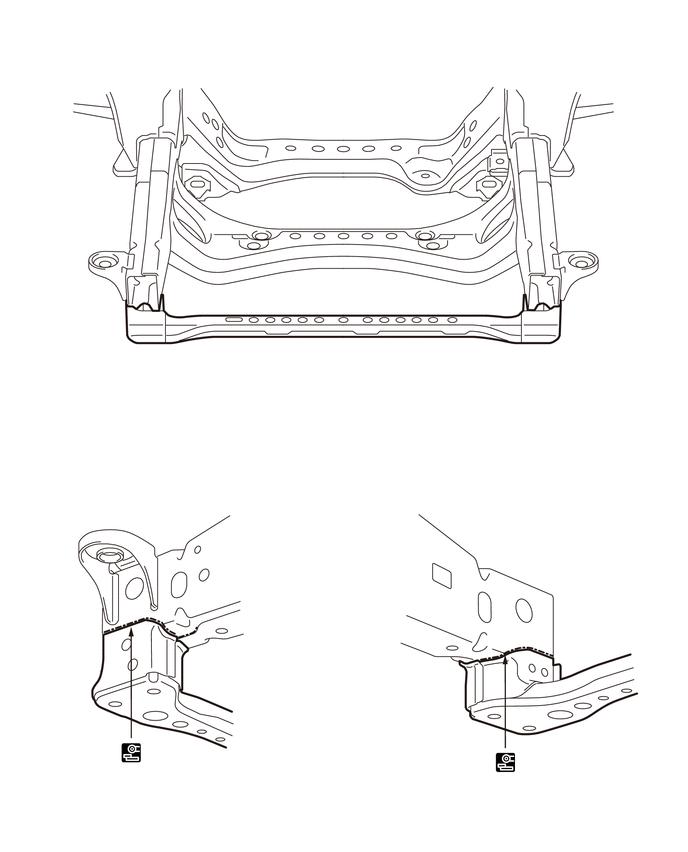
INSTALLATION
| Symbol Meaning | |
|---|---|

|
Fillet Weld |
Make sure that proper welding can be performed by setting up the welding conditions as necessary before performing work.
Make sure that the welding bead at *a is overlapped.
To prevent heat deformation, weld the right and left side of each part before continuing to the next part.
After applying the top coat, apply anti-rust agent to the internal panel portion of the closed section structural weld points.
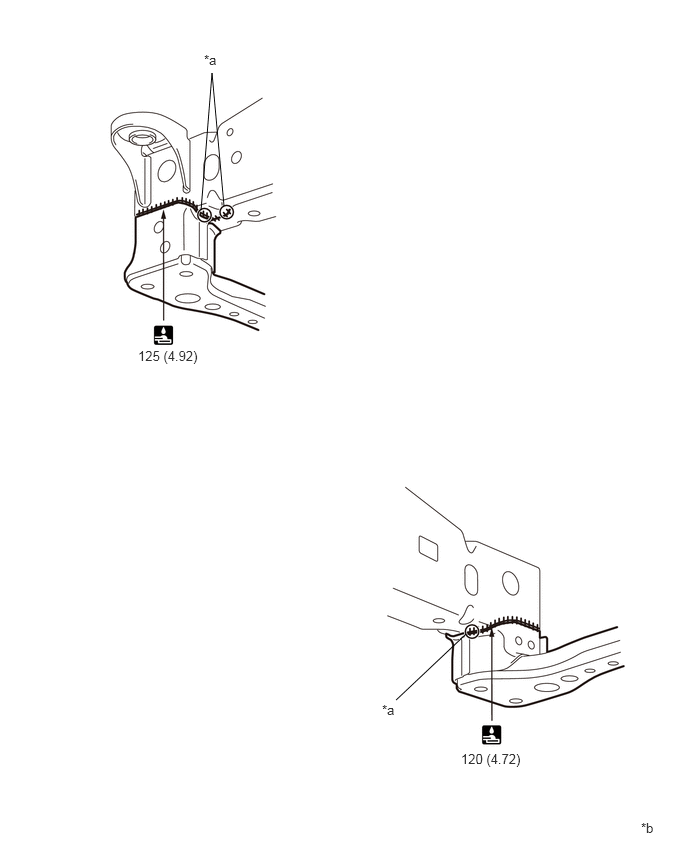
| *b | mm (in.) | - | - |
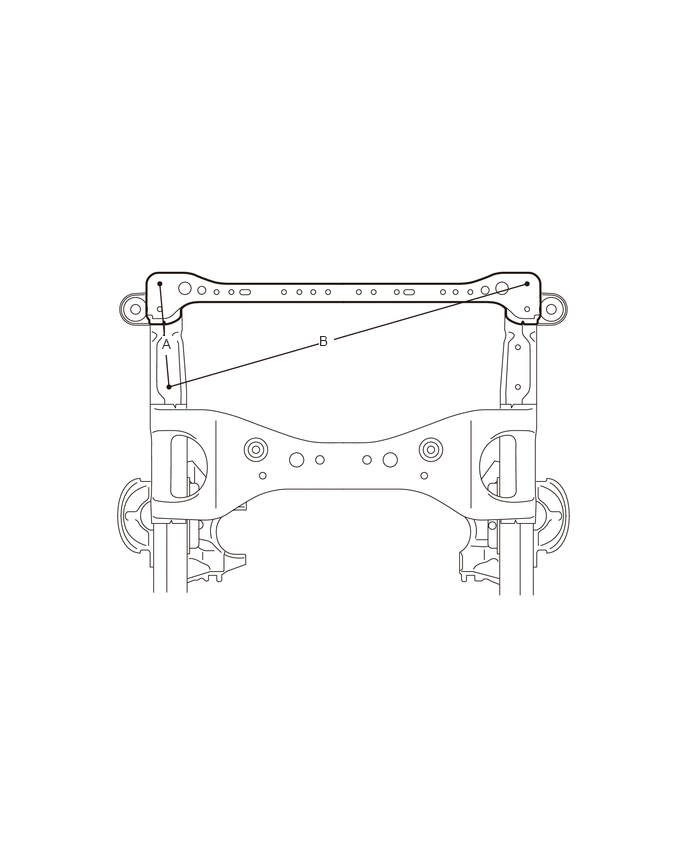
- Reference Value:
Area Measurement Area Measurement A 240 mm (9.45 in.) B 880 mm (34.65 in.)
w/ Winch
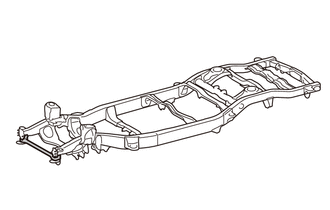
With the frame side rail plate removed.
REMOVAL
| Symbol Meaning | |
|---|---|
|
|
Cut with Disc Sander etc. |
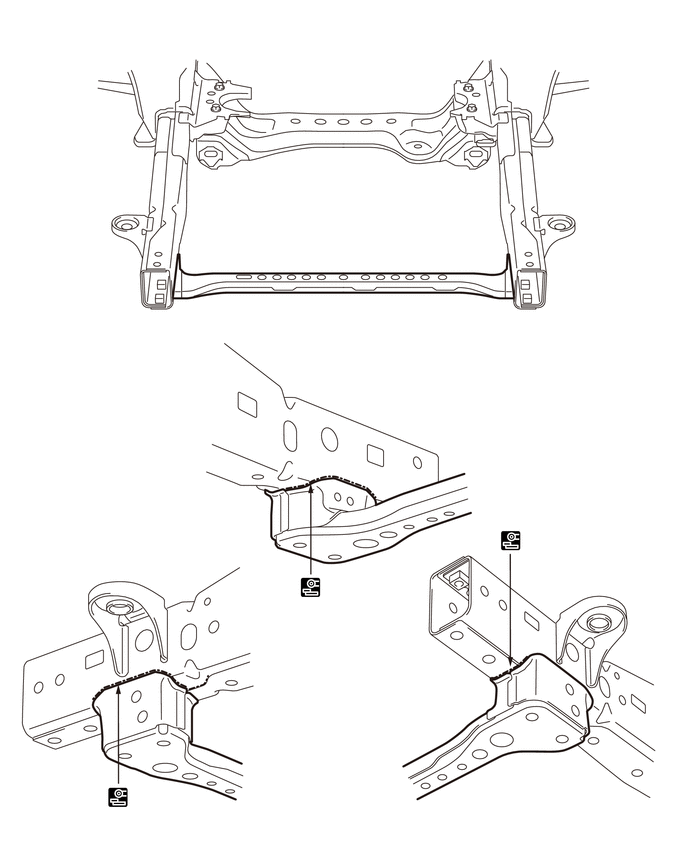
INSTALLATION
| Symbol Meaning | |
|---|---|
|
|
Fillet Weld |
Make sure that proper welding can be performed by setting up the welding conditions as necessary before performing work.
Make sure that the welding bead at *a is overlapped.
To prevent heat deformation, weld the right and left side of each part before continuing to the next part.
After applying the top coat, apply anti-rust agent to the internal panel portion of the closed section structural weld points.
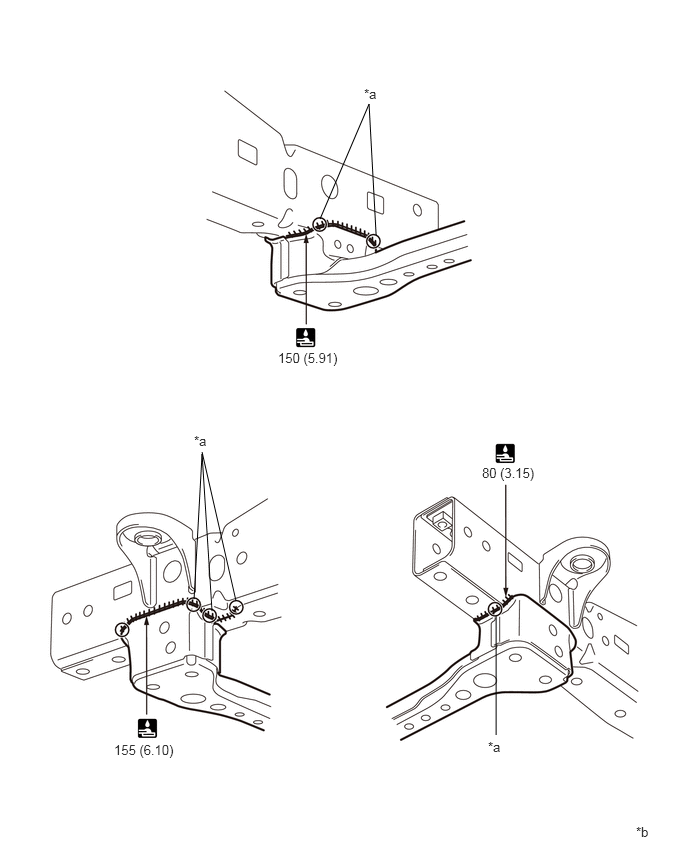
| *b | mm (in.) | - | - |
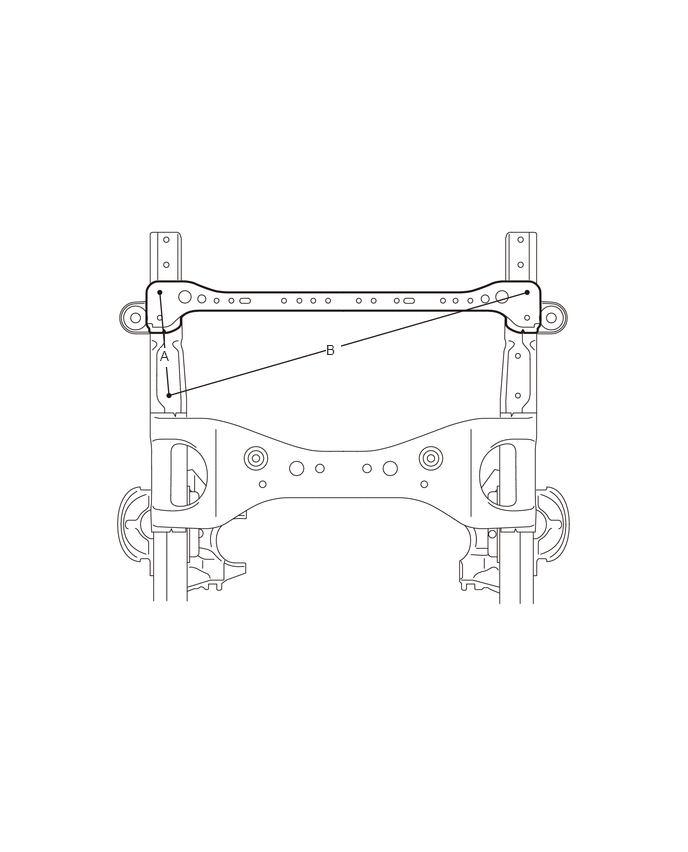
- Reference Value:
Area Measurement Area Measurement A 240 mm (9.45 in.) B 880 mm (34.65 in.)