1NZ-FE ENGINE MECHANICAL CYLINDER BLOCK INSPECTION
PROCEDURE

 1.INSPECT CYLINDER BLOCK FOR WARPAGE
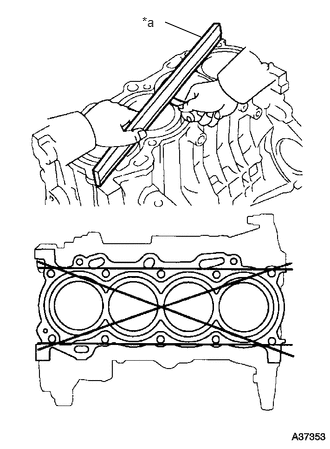
| *a | Straightedge |
Using a precision straightedge and feeler gauge, measure the warpage of the surface which is in contact with the cylinder head gasket.
- Maximum warpage:
0.05 mm (0.0020 in.)
If the warpage is greater than the maximum, replace the cylinder block sub-assembly.
2.INSPECT CYLINDER BORE
Visually inspect the surface of the cylinder walls to make sure there are no scratches, etc.
If there are scratches, etc. on the cylinder walls, replace the cylinder block sub-assembly.
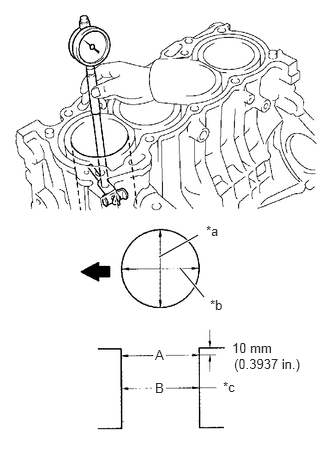
| *a | Thrust Direction |
| *b | Axial Direction |
| *c | Center |

|
Engine Front |
Using a cylinder gauge, measure the cylinder bore diameter at positions A and B in the thrust and axial directions.
- Reference value (New parts) inside diameter:
75.000 to 75.013 mm (2.9528 to 2.9533 in.)
- Maximum inside diameter:
75.133 mm (2.9580 in.)
If the inside diameter is greater than the maximum, replace the cylinder block sub-assembly
13101
3.INSPECT PISTON WITH PIN SUB-ASSEMBLY
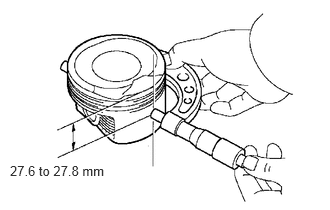
Using a micrometer, measure the piston diameter at a right angle to the piston pin center line, and at the position 27.6 to 27.8 mm (1.0866 to 1.0945 in.) from top of the piston head.
- Reference value (New parts) piston diameter:
74.935 to 74.945 mm (2.9502 to 2.9506 in.)
Using a caliper gauge, measure the piston pin hole diameter.
- Reference value (New parts) piston pin hole diameter:
18.013 to 18.016 mm (0.7092 to 0.7093 in.) at 20°C (68°F)
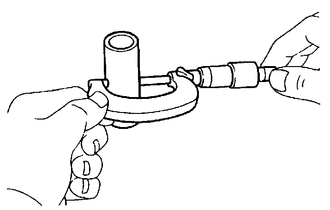
Using a micrometer, measure the piston pin diameter.
- Reference value (New parts) piston pin diameter:
18.001 to 18.004 mm (0.7087 to 0.7088 in.)
Subtract the piston pin diameter measurement from the piston pin hole diameter measurement to calculate the oil clearance.
- Reference value (New parts) oil clearance:
0.009 to 0.015 mm (0.0004 to 0.0006 in.)
- Maximum oil clearance:
0.050 mm (0.0020 in.)
If necessary, replace the piston with pin sub-assembly.
4.INSPECT PISTON CLEARANCE
Subtract the piston diameter measurement from the cylinder bore diameter measurement to calculate the oil clearance.
- Reference value (New parts) oil clearance:
0.055 to 0.078 mm (0.0022 to 0.0031 in.)
- Maximum oil clearance:
0.08 mm (0.0032 in.)
If the piston oil clearance is greater than the maximum, calculate the oil clearance using the measured cylinder internal diameter and piston external diameter as well as the reference diameters (for new parts), and replace the piston with pin sub-assembly or cylinder block sub-assembly.
5.INSPECT RING GROOVE CLEARANCE
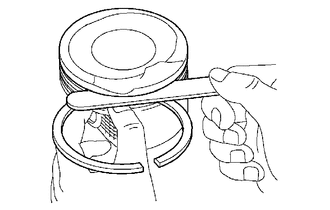
Using a feeler gauge, measure the clearance between the piston ring set and wall of the ring groove.
- Ring groove clearance:
- No. 1 compression ring:
0.03 to 0.07 mm (0.0012 to 0.0028 in.)
- No. 2 compression ring:
0.02 to 0.06 mm (0.0008 to 0.0024 in.)
- Oil ring:
0.07 to 0.13 mm (0.0028 to 0.0052 in.)
If the ring groove clearance is not as specified, replace the piston ring set. If the ring groove clearance is still not as specified even with a new piston ring set, replace the piston with pin sub-assembly.
6.INSPECT PISTON RING END GAP
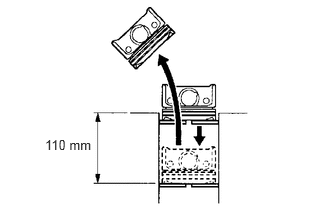
Using a piston, push the piston ring, a little beyond the bottom of the ring travel, 110 mm (4.33 in.) from the top of the cylinder block sub-assembly.
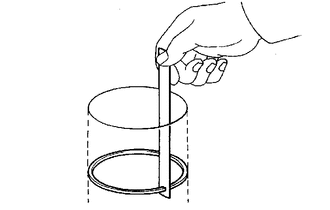
Using a feeler gauge, measure the end gap.
- Standard end gap:
- No. 1 compression ring:
0.18 to 0.23 mm (0.0071 to 0.0091 in.)
- No. 2 compression ring:
0.37 to 0.47 mm (0.0146 to 0.0185 in.)
- Oil ring (Side rail):
0.10 to 0.35 mm (0.0039 to 0.0138 in.)
- Maximum end gap:
- No. 1 compression ring:
0.86 mm (0.0339 in.)
- No. 2 compression ring:
1.03 mm (0.0406 in.)
- Oil ring (Side rail):
0.82 mm (0.0323 in.)
If the piston ring end gap is greater than the maximum, replace the piston ring set. If the piston ring end gap is greater than the maximum, even with a new piston ring set, replace the cylinder block sub-assembly.
13411
7.INSPECT CRANKSHAFT
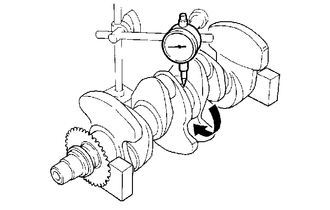
Using a dial indicator and V-blocks, measure the circle runout as shown in the illustration.
- Maximum circle runout:
0.03 mm (0.0012 in.)
If the circle runout is greater than the maximum, replace the crankshaft.
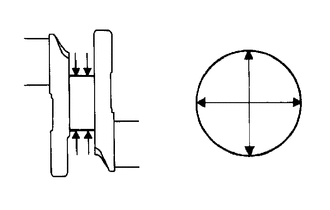
Using a micrometer, measure the diameter of each main journal.
- Outside diameter:
45.988 to 46.000 mm (1.8106 to 1.8110 in.)
If the diameter is not as specified, check the crankshaft oil clearance.
Check each main journal for taper and out-of-roundness as shown.
- Maximum taper and out-of-roundness:
0.02 mm (0.0008 in.)
If the taper and out-of-roundness are greater than the maximum, replace the crankshaft.
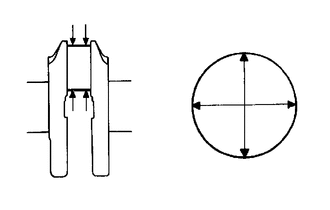
Using a micrometer, measure the diameter of each crank pin.
- Outside diameter:
39.992 to 40.000 mm (1.5745 to 1.5748 in.)
If the diameter is not as specified, check the connecting rod oil clearance.
Check each crank pin for taper and out-of-roundness as shown.
- Maximum taper and out-of-roundness:
0.02 mm (0.0008 in.)
If the taper and out-of-roundness are greater than the maximum, replace the crankshaft.
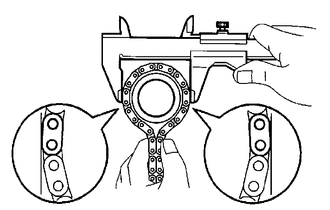
Wrap the chain sub-assembly around the timing sprocket.
Using a vernier caliper, measure the timing sprocket diameter with the chain sub-assembly.
- Standard sprocket diameter (with chain):
51.72 mm (2.0362 in.)
- Minimum sprocket diameter (with chain):
50.5 mm (1.988 in.)
- NOTICE:
-
Make sure that the vernier caliper is in contact with the chain rollers when measuring.
If the diameter is less than the minimum, replace the chain sub-assembly and crankshaft.
13265
8.INSPECT CONNECTING ROD BOLT
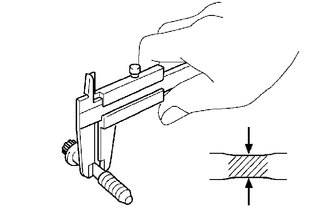
Using a vernier caliper, measure the diameter of the connecting rod bolt at the elongated portion.
- Standard diameter:
6.6 to 6.7 mm (0.260 to 0.264 in.)
- Minimum diameter:
6.4 mm (0.252 in.)
If the diameter is less than the minimum, replace the connecting rod bolt.
11416
9.INSPECT CRANKSHAFT BEARING CAP SET BOLT
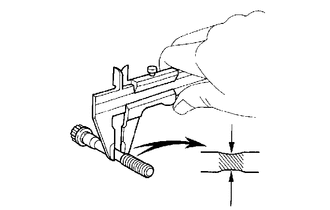
Using a vernier caliper, measure the tension portion diameter at the elongated portion.
- Standard diameter:
7.3 to 7.5 mm (0.287 to 0.295 in.)
- Minimum diameter:
7.2 mm (0.283 in.)
If the diameter is less than minimum, replace the crankshaft bearing cap set bolt.
10.INSPECT CONNECTING ROD THRUST CLEARANCE
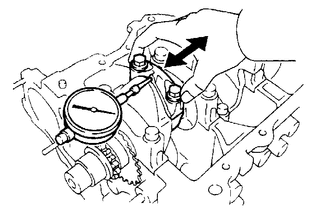
Using a dial indicator, measure the thrust clearance while moving the connecting rod back and forth.
- Standard thrust clearance:
0.16 to 0.36 mm (0.0063 to 0.0142 in.)
- Maximum thrust clearance:
0.36 mm (0.0142 in.)
If the thrust clearance is greater than the maximum, replace the connecting rod sub-assembly as necessary. If necessary, replace the crankshaft.
11.INSPECT CONNECTING ROD OIL CLEARANCE
Check that the matchmarks on the connecting rod and connecting rod cap are aligned to ensure correct reassembly.
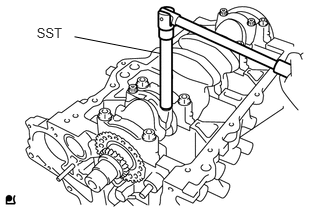
Using SST, remove the 2 connecting rod bolts.
- SST
- 09205-16011
Clean the crank pin and connecting rod bearing.
Check the crank pin and connecting rod bearing for pitting and scratches.
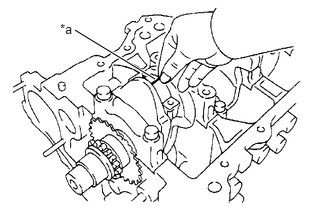
| *a | Plastigage |
Lay a strip of Plastigage across the crank pin.
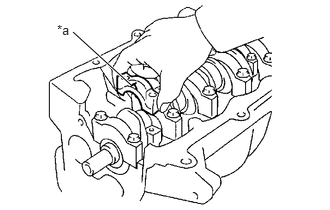
| *a | Front Mark |
Make sure that the connecting rod and connecting rod cap are in the correct combination and that the front mark on the connecting rod cap is facing in the correct mounting orientation, then install the connecting rod cap to the connecting rod.
Apply a light coat of engine oil to the threads of the connecting rod bolts.
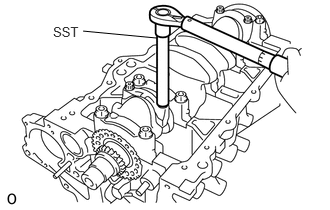
Using SST, tighten the 2 connecting rod bolts in several steps to the specified torque.
- SST
- 09205-16011
- Torque:
- 15 N*m (153 kgf*cm, 11 ft.*lbf)
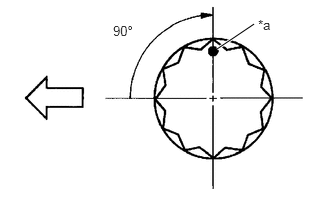
| *a | Paint Mark |

|
Engine Front |
Mark the front of the connecting rod bolts with paint.
Further tighten the connecting rod bolts by 90° as shown in the illustration.
- NOTICE:
-
Do not turn the crankshaft.
Remove the 2 connecting rod bolts, connecting rod cap and connecting rod bearing.
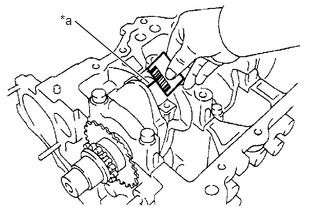
| *a | Plastigage |
Measure the Plastigage at its widest point.
- Standard oil clearance:
0.012 to 0.038 mm (0.00047 to 0.0015 in.)
- NOTICE:
-
Completely remove the Plastigage after the measurement.
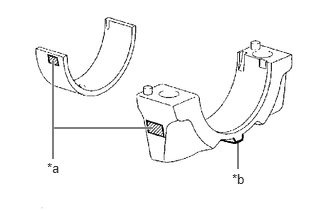
| *a | Mark 1, 2 or 3 |
| *b | Front Mark |
When replacing a connecting rod bearing, replace it with one with the same number as marked on the connecting rod. There are 3 sizes of standard connecting rod bearings, marked 1, 2 and 3 accordingly.
| Mark | mm (in.) |
|---|---|
| 1 | 1.491 to 1.494 (0.0587 to 0.0588) |
| 2 | 1.494 to 1.497 (0.0588 to 0.0589) |
| 3 | 1.497 to 1.500 (0.0589 to 0.0591) |
12.INSPECT CRANKSHAFT THRUST CLEARANCE
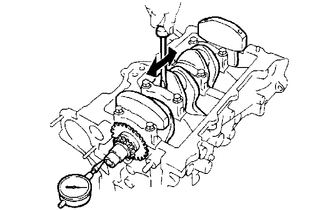
Using a dial indicator, measure the thrust clearance while moving the crankshaft back and forth with a screwdriver.
- Standard thrust clearance:
0.09 to 0.19 mm (0.0035 to 0.0075 in.)
- Maximum thrust clearance:
0.30 mm (0.0118 in.)
- HINT:
-
Upper crankshaft thrust washer thickness: 2.43 to 2.48 mm (0.0957 to 0.976 in.)
If the thrust clearance is greater than the maximum, replace the upper crankshaft thrust washers as a set. Check the crankshaft and cylinder block sub-assembly for wear. Repair or replace the parts if necessary.
13.INSPECT CRANKSHAFT OIL CLEARANCE
Clean each main journal and crankshaft bearing.
Install the crankshaft bearing to the cylinder block sub-assembly and crankshaft bearing cap.
Click hereEngine / Hybrid System>1NZ-FE ENGINE MECHANICAL>CYLINDER BLOCK>REASSEMBLY
Place the crankshaft to the cylinder block sub-assembly.
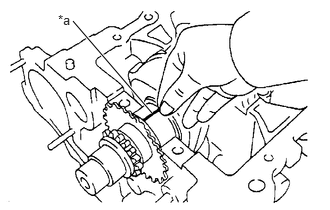
| *a | Plastigage |
Lay a strip of Plastigage across each journal.
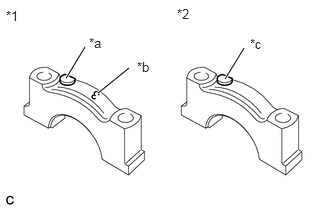
| *1 | No. 3 Crankshaft Bearing Cap |
| *2 | No. 1, 2, 4, 5 Crankshaft Bearing Cap |
| *a | Front Mark |
| *b | Number |
| *c | Front Mark and Number |
Examine the front marks and numbers and install the crankshaft bearing cap to the cylinder block sub-assembly.
Apply a light coat of engine oil to the threads of the crankshaft bearing cap set bolts.
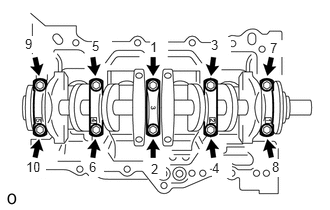
Using a 12 mm socket wrench, tighten the crankshaft bearing cap set bolts in several steps to the specified torque in the sequence shown in the illustration. (*1)
- Torque:
- 22 N*m (224 kgf*cm, 16 ft.*lbf)
| *a | Paint Mark |
|
|
Engine Front |
Mark the front of the crankshaft bearing cap set bolts with paint.
Further tighten the crankshaft bearing cap set bolts by 90° in the same sequence as step (*1).
Check that the painted mark is now at a 90° angle from the front.
- NOTICE:
-
Do not turn the crankshaft.
Remove the crankshaft bearing caps.
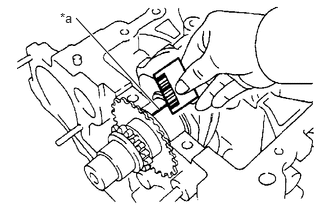
| *a | Plastigage |
Measure the Plastigage at its widest point.
- Standard oil clearance:
0.01 to 0.023 mm (0.0004 to 0.0009 in.)
- Maximum oil clearance:
0.07 mm (0.0028 in.)
- NOTICE:
-
Completely remove the Plastigage after the measurement.
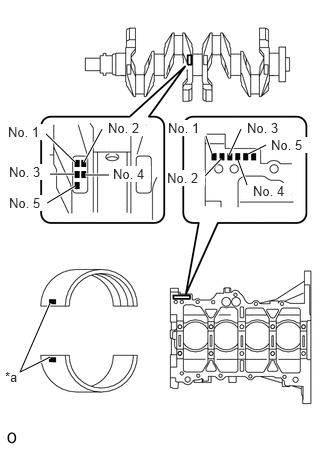
| *a | Mark |
When replacing a standard bearing, replace it with one with the same number. If the number of the bearing cannot be found, select the correct bearing by adding together the numbers imprinted on the cylinder block sub-assembly and crankshaft, then select the bearing with the same number as the total. There are 4 sizes of standard bearings, marked 1, 2, 3 and 4 accordingly.
| Cylinder Block (A)
+ Crankshaft (B) |
0 to 2 | 3 to 5 | 6 to 8 | 9 to 11 |
| Use Bearing | 1 | 2 | 3 | 4 |
| Item | Mark | mm (in.) |
|---|---|---|
| Cylinder block main journal bore diameter (A) | 0
1 2 3 4 5 6 |
50.000 to 50.003 (1.96850 to 1.96862)
50.003 to 50.005 (1.96862 to 1.96870) 50.005 to 50.007 (1.96870 to 1.96878) 50.007 to 50.010 (1.96878 to 1.96890) 50.010 to 50.012 (1.96890 to 1.96898) 50.012 to 50.014 (1.96898 to 1.96906) 50.014 to 50.016 (1.96906 to 1.96913) |
| Crankshaft main journal diameter (B) | 0
1 2 3 4 5 |
45.998 to 46.000 (1.81094 to 1.81102)
45.996 to 45.998 (1.81087 to 1.81094) 45.994 to 45.996 (1.81079 to 1.81087) 45.992 to 45.994 (1.81071 to 1.81079) 45.990 to 45.992 (1.81063 to 1.81071) 45.988 to 45.990 (1.81055 to 1.81063) |
| Standard bearing center wall thickness | 1
2 3 4 |
1.992 to 1.995 (0.07843 to 0.07854)
1.995 to 1.998 (0.07854 to 0.07866) 1.998 to 2.001 (0.07866 to 0.07878) 2.001 to 2.004 (0.07878 to 0.07890) |