Home › Engine / Hybrid System › 1GR-FE (ENGINE MECHANICAL) › CYLINDER BLOCK
RM38G0E _51 Engine / Hybrid System _101207 1GR-FE ENGINE MECHANICAL _0469490 CYLINDER BLOCK A

1GR-FE ENGINE MECHANICAL  CYLINDER BLOCK  REASSEMBLY  


CAUTION / NOTICE / HINT
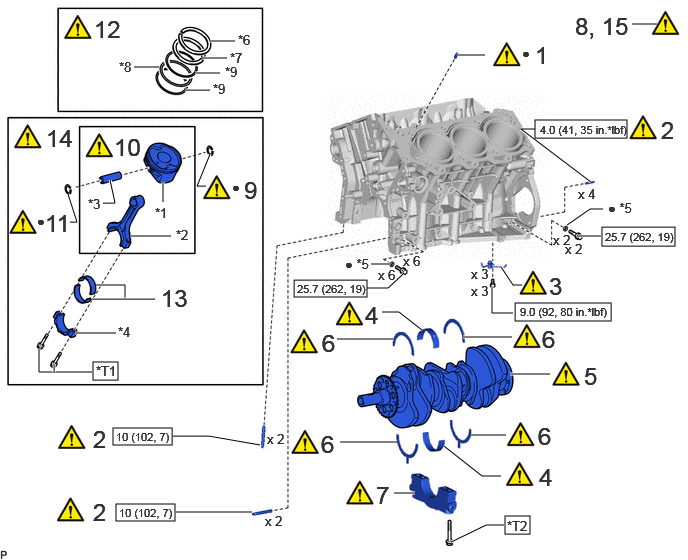
COMPONENTS (REASSEMBLY)
A488532N01
0.969,3.771 1.229,3.958 0.26,0.188 3.063,2.917 3.823,3.094 0.76,0.177 5.365,3.156 6.365,3.344 1,0.188 6.271,2.365 7.031,2.563 0.76,0.198 5.26,5.375 5.521,5.563 0.26,0.188 5.573,1.25 6.531,1.438 0.958,0.188 1.208,5.25 1.823,5.427 0.615,0.177 1.177,4.458 1.792,4.635 0.615,0.177 5.313,3.896 5.729,3.896 true 4.625,4.646 5.021,4.958 5.021,4.958 5.219,4.958 true 4.396,3.438 4.156,3.25 4.156,3.25 3.979,3.25 true 5.219,2.781 5.344,2.969 5.344,2.969 5.438,2.969 true 4.906,4.531 5.271,4.531 true 3.542,4.604 4.135,4.604 true 3.51,3.531 4.104,3.531 true 4.823,3.51 5.333,3.51 true 4.104,5.135 4.323,5.135 true 6.583,0.25 6.844,0.25 true 1,2.969 1.302,2.969 1.302,2.969 1.302,3.104 true 0.948,3.115 1.615,3.115 true 1.802,4.542 2.177,4.542 2.177,4.542 2.708,4.635 true 1.833,5.333 2.625,5.333 true 5.573,1.344 5.427,1.344 5.427,1.344 6.156,1.896 true 4.76,0.573 5.052,0.573 true 0.729,2.313 0.802,2.313 0.802,2.313 0.708,2.021 true 2.146,1.938 2.052,1.938 2.052,1.938 2.188,1.604 true 1.354,2.458 1.781,2.458 true 1.698,1.896 1.698,2.104 true 1.146,1.875 1.198,2.115 1.198,2.115 1.073,2.115 true 0.781,3.469 1.208,3.469 true 5.906,2.344 6.146,2.177 6.146,2.177 6.281,2.177 true 0.406,3.625 0.406,3.875 0.406,3.875 0.958,3.875 true 0.563,3.792 0.563,3.875 true 3.865,2.75 4.063,2.75 true 3.823,3 4.042,3 4.042,3 4.198,2.854 true 5.344,3.26 5.125,3.26 5.125,3.26 5.125,2.99 true 6.031,2.458 6.26,2.458 true 4.698,5.646 5.063,5.469 5.063,5.469 5.25,5.469 true 2.188,0.427 2.448,0.427 true 2.104,0.604 2.365,0.604 true 1.396,0.698 1.656,0.698 true 2.031,0.76 2.292,0.76 true 1.927,0.938 2.188,0.938 true 5.99,0.125 6.635,0.438 0.646,0.313 18 false 8, 15 0.479,1.292 0.823,1.688 0.344,0.396 18 false 14 6.083,3.771 6.51,4.198 0.427,0.427 18 false 5 5.615,4.823 6.052,5.188 0.438,0.365 18 false 4 3.802,3.135 4.24,3.5 0.438,0.365 18 false 4 5.719,2.833 6.156,3.198 0.438,0.365 18 false 3 5.604,4.396 6.052,4.771 0.448,0.375 18 false 6 3.344,4.479 3.781,4.844 0.438,0.365 18 false 6 3.354,3.427 3.792,3.792 0.438,0.365 18 false 6 5.646,3.385 6.083,3.75 0.438,0.365 18 false 6 1.677,2.958 2.021,3.354 0.344,0.396 18 false 13 0.979,0.156 1.323,0.552 0.344,0.396 18 false 12 1.188,1.385 1.531,1.781 0.344,0.396 18 false 10 0.969,4.427 1.406,4.792 0.438,0.365 18 false 2 0.469,2.177 0.813,2.573 0.344,0.396 18 false 11 3.917,5.01 4.26,5.406 0.344,0.396 18 false 7 0.969,5.188 1.406,5.552 0.438,0.365 18 false 2 6.885,1.208 7.063,1.573 0.177,0.365 18 false 2 2.542,1.833 2.948,2.229 0.406,0.396 18 false 9 1.615,2.135 1.958,2.531 0.344,0.396 10 false *1 1.833,2.365 2.177,2.76 0.344,0.396 10 false *2 0.917,2.042 1.26,2.438 0.344,0.396 10 false *3 1.229,3.375 1.573,3.771 0.344,0.396 10 false *4 3.938,2.781 4.281,3.177 0.344,0.396 10 false x 6 4.198,2.635 4.542,3.031 0.344,0.396 10 false x 6 5.76,2.417 6.104,2.813 0.344,0.396 10 false x 2 5.885,2.51 6.229,2.906 0.344,0.396 10 false x 2 6.333,2.083 6.677,2.479 0.344,0.396 10 false ● *5 3.594,2.667 3.938,3.063 0.344,0.396 10 false ● *5 1,3.781 1.344,4.177 0.344,0.396 10 false *T1 3.094,2.938 3.917,3.146 0.823,0.208 8 false 25.7 (262, 19) 5.417,3.177 6.375,3.438 0.958,0.26 8 false 9.0 (92, 80 in.*lbf) 6.302,2.396 7.083,2.604 0.781,0.208 8 false 25.7 (262, 19) 5.281,5.396 5.594,5.74 0.313,0.344 10 false *T2 6.021,1.938 6.365,2.333 0.344,0.396 10 false x 4 5.625,1.281 6.583,1.542 0.958,0.26 8 false 4.0 (41, 35 in.*lbf) 2.781,4.49 3.125,4.885 0.344,0.396 10 false x 2 2.76,5.344 3.104,5.74 0.344,0.396 10 false x 2 1.24,5.271 1.948,5.458 0.708,0.188 8 false 10 (102, 7) 1.208,4.479 1.917,4.667 0.708,0.188 8 false 10 (102, 7) 2.479,0.333 2.688,0.573 0.208,0.24 10 false *6 2.396,0.521 2.604,0.76 0.208,0.24 10 false *7 1.24,0.615 1.448,0.854 0.208,0.24 10 false *8 2.344,0.667 2.552,0.906 0.208,0.24 10 false *9 2.219,0.844 2.427,1.083 0.208,0.24 10 false *9 0.385,2.219 0.729,2.615 0.344,0.396 10 false ● 2.417,1.865 2.76,2.26 0.344,0.396 10 false ● 5.438,0.469 5.781,0.865 0.344,0.396 10 false ● 5.573,0.427 5.875,0.792 0.302,0.365 18 false 1 4.906,2.771 5.25,3.167 0.344,0.396 10 false x 3 4.906,2.948 5.25,3.344 0.344,0.396 10 false x 3

Procedure Part Name Code
Z101186

Z101188

Z101187

1 STRAIGHT PIN - (Click here) - -
2 STUD BOLT - (Click here) - -
3 NO. 1 OIL NOZZLE SUB-ASSEMBLY 15708 (Click here) - -
4 CRANKSHAFT BEARING 11702 (Click here) - -
5 CRANKSHAFT 13411 (Click here) - -
6 CRANKSHAFT THRUST WASHER 11011 (Click here) - -
7 CRANKSHAFT BEARING CAP - (Click here) - -
8 INSPECT CRANKSHAFT THRUST CLEARANCE - (Click here) - -
9 PISTON PIN HOLE SNAP RING 13101A (Click here) - -
10 PISTON WITH PIN SUB-ASSEMBLY 13101 (Click here) - -
11 PISTON PIN HOLE SNAP RING 13101A (Click here) - -
12 PISTON RING SET 13011 (Click here) - -
13 CONNECTING ROD BEARING 13041 (Click here) - -
14 PISTON WITH CONNECTING ROD - (Click here) - -
15 INSPECT CONNECTING ROD THRUST CLEARANCE - (Click here) - -

*1 PISTON *2 CONNECTING ROD SUB-ASSEMBLY
*3 PISTON PIN *4 CONNECTING ROD CAP
*5 SEAL WASHER *6 NO. 1 COMPRESSION RING
*7 NO. 2 COMPRESSION RING *8 OIL RING (EXPANDER)
*9 OIL RING (SIDE RAIL) - -
V100146

N*m (kgf*cm, ft.*lbf): Specified torque ● Non-reusable part
*T1 1st: 24.5 (250, 18)
2nd: Turn 90°
*T2 1st: 61 (622, 45)
2nd: Turn 90°

PROCEDURE

Hide 1.INSTALL STRAIGHT PIN

Z101186

NOTICE:

It is not necessary to remove a straight pin unless it is being replaced.


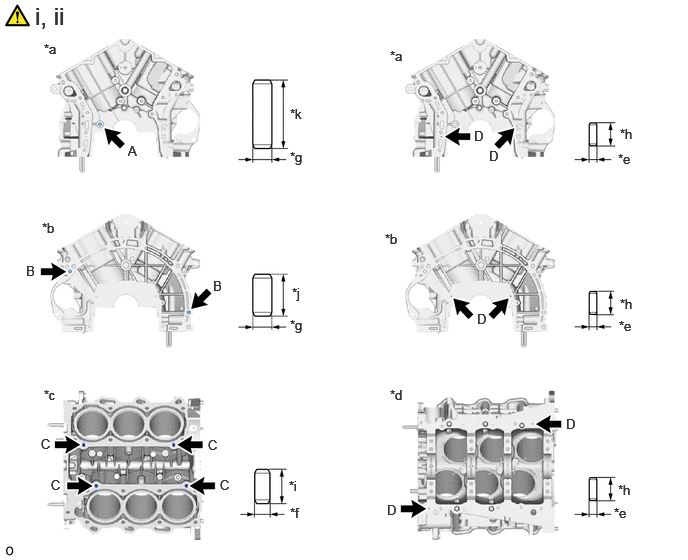
a.
A487739C01
0.458,0.427 0.719,0.625 0.26,0.198 10 false *a 0.438,2.292 0.75,2.49 0.313,0.198 10 false *b 0.458,4.031 0.677,4.25 0.219,0.219 10 false *c 4.063,4.031 4.323,4.24 0.26,0.208 10 false *d 6.438,1.573 6.729,1.854 0.292,0.281 10 false *e 3.021,5.26 3.26,5.448 0.24,0.188 10 false *f 3.021,1.552 3.344,1.792 0.323,0.24 10 false *g 6.458,1.313 6.75,1.5 0.292,0.188 10 false *h 3.01,4.979 3.281,5.208 0.271,0.229 10 false *i 3.042,2.969 3.365,3.219 0.323,0.25 10 false *j 3.021,1.104 3.302,1.292 0.281,0.188 10 false *k 4.063,0.5 4.323,0.698 0.26,0.198 10 false *a 4.01,2.406 4.323,2.604 0.313,0.198 10 false *b 3.021,3.302 3.344,3.542 0.323,0.24 10 false *g 6.458,3.083 6.75,3.271 0.292,0.188 10 false *h 6.448,3.313 6.74,3.594 0.292,0.281 10 false *e 6.438,5.021 6.729,5.208 0.292,0.188 10 false *h 6.396,5.26 6.688,5.542 0.292,0.281 10 false *e 0.365,0.021 0.896,0.354 0.531,0.333 18 false i, ii 1.333,1.49 1.542,1.698 0.208,0.208 10 false A 2.219,2.896 2.406,3.104 0.188,0.208 10 false B 0.271,2.74 0.458,2.948 0.188,0.208 10 false B 2.167,4.552 2.354,4.729 0.188,0.177 10 false C 2.292,4.969 2.479,5.146 0.188,0.177 10 false C 0.531,4.969 0.698,5.167 0.167,0.198 10 false C 0.427,4.542 0.594,4.74 0.167,0.198 10 false C 4.938,1.333 5.146,1.542 0.208,0.208 10 false D 5.094,1.542 5.302,1.75 0.208,0.208 10 false D 4.969,3.24 5.177,3.448 0.208,0.208 10 false D 5.896,4.333 6.104,4.542 0.208,0.208 10 false D 4.031,5.229 4.24,5.438 0.208,0.208 10 false D
*a Front Side *b Rear Side
*c Upper Side *d Lower Side
*e 4.0 mm (0.157 in.) *f 8.0 mm (0.315 in.)
*g 10 mm (0.394 in.) *h 12 mm (0.472 in.)
*i 18 mm (0.709 in.) *j 22 mm (0.866 in.)
*k 36 mm (1.41 in.) - -


i.

Using a plastic-faced hammer, tap in new straight pins to the cylinder block.

Standard Protrusion Height:
Item Specified Condition
Pin A 22.5 to 23.5 mm (0.886 to 0.925 in.)
Pin B 10.5 to 11.5 mm (0.413 to 0.453 in.)
Pin C 8.5 to 9.5 mm (0.335 to 0.374 in.)
Pin D 5.5 to 6.5 mm (0.217 to 0.256 in.)


Hide 2.INSTALL STUD BOLT

Z101186

NOTICE:

If a stud bolt is deformed or its threads are damaged, replace it.


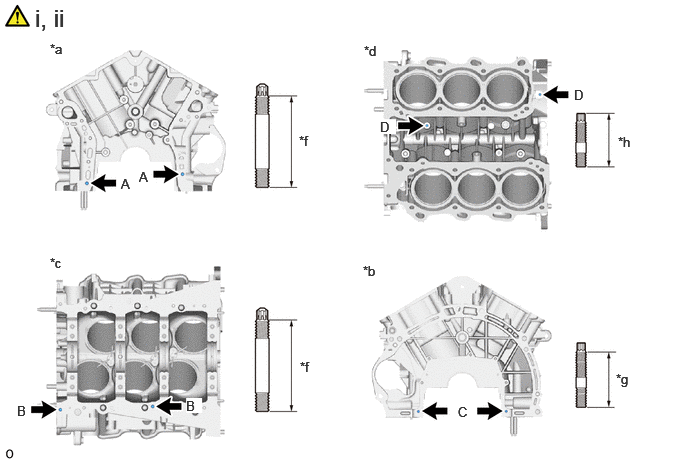
a.
A487741C01
0.521,0.427 0.76,0.625 0.24,0.198 10 false *a 3.781,2.74 4,2.927 0.219,0.188 10 false *b 0.521,2.656 0.75,2.865 0.229,0.208 10 false *c 3.792,0.448 4.031,0.667 0.24,0.219 10 false *d 3.115,1.385 3.438,1.615 0.323,0.229 10 false *f 6.417,3.865 6.688,4.115 0.271,0.25 10 false *g 3.125,3.74 3.438,3.979 0.313,0.24 10 false *f 6.438,1.396 6.729,1.677 0.292,0.281 10 false *h 1.26,1.833 1.5,2.031 0.24,0.198 10 false A 1.448,1.76 1.688,1.958 0.24,0.198 10 false A 4.771,4.208 5.01,4.406 0.24,0.198 10 false C 0.177,4.198 0.417,4.396 0.24,0.198 10 false B 1.938,4.146 2.104,4.302 0.167,0.156 10 true B 3.958,1.24 4.125,1.396 0.167,0.156 10 true D 5.979,0.906 6.146,1.063 0.167,0.156 10 true D 0.365,0.042 0.875,0.333 0.51,0.292 18 false i, ii
*a Front Side *b Rear Side
*c Lower Side *d Upper Side
*f 52 mm (2.05 in.) *g 23 mm (0.906 in.)
*h 19 mm (0.748 in.) - -


i.

Using E5, E7 and E8 "TORX" wrenches, install new stud bolts.

Torque:
for stud bolt A and B : 10 N*m (102 kgf*cm, 7 ft.*lbf)
for stud bolt C and D : 4.0 N*m (41 kgf*cm, 35 in.*lbf)


Hide 15708 3.INSTALL NO. 1 OIL NOZZLE SUB-ASSEMBLY
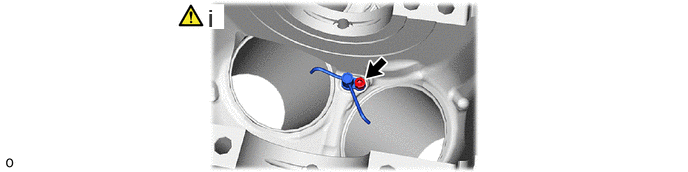
a.
A487735N01
2.167,0.042 2.333,0.302 0.167,0.26 18 true i

i.

Using a 5 mm hexagon socket wrench, install the 3 No. 1 oil nozzle sub-assemblies with the 3 bolts.

Torque:
9.0 N*m (92 kgf*cm, 80 in.*lbf)


Hide 11702 4.INSTALL CRANKSHAFT BEARING

a.
A488506C01
5.698,2.219 5.969,2.438 0.271,0.219 10 false *a 6.542,2.219 6.833,2.417 0.292,0.198 10 false *b 1.375,1.021 1.677,1.229 0.302,0.208 10 false *c 0.948,2.573 1.26,2.76 0.313,0.188 10 false *d 2.208,2.198 2.458,2.417 0.25,0.219 10 false A 3.427,2.208 3.677,2.427 0.25,0.219 10 false B 0.385,0.031 0.729,0.354 0.344,0.323 18 false i 4.542,0.021 4.885,0.344 0.344,0.323 18 false ii 0.365,1.135 1.031,1.531 0.667,0.396 18 false iii, iv
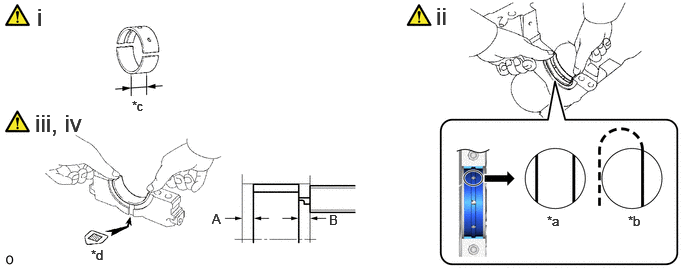
*a CORRECT *b INCORRECT
*c Width *d Journal Number


i.

Clean each main journal and bearing.

HINT:

Be sure to check the crankshaft bearings since the width differ according to the installation position.

Item Width
No. 1 and No. 2 journal bearings 20.0 mm (0.787 in.)
No. 3 and No. 4 journal bearings 17.4 mm (0.685 in.)


ii.

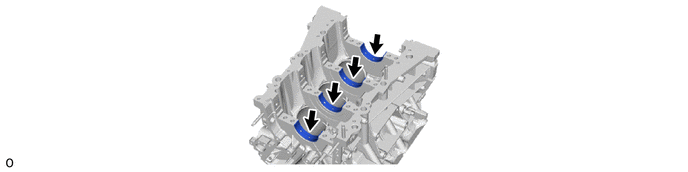
Install the upper crankshaft bearing to the cylinder block sub-assembly as shown in the illustration.

NOTICE:
·

Do not apply engine oil to the upper crankshaft bearings or the contact surface.

·

Make sure both sides of the oil groove in the cylinder block sub-assembly are visible through the oil feed holes in the upper crankshaft bearing. Make sure the amount visible on each side of the holes is equal.

·

Do not allow coolant to come into contact with the upper crankshaft bearing inner surface.

·

If any coolant comes into contact with the upper crankshaft bearing inner surface, replace the upper crankshaft bearing with a new one.


iii.

Install the lower crankshaft bearings to the crankshaft bearing caps.


iv.

Using a vernier caliper, measure the distance between the edge of the crankshaft bearing cap and the edge of the lower crankshaft bearing.

Dimension A - B or B - A:

0 to 0.7 mm (0 to 0.0276 in.)


NOTICE:
·

Do not apply engine oil to the lower crankshaft bearings or the contact surfaces.

·

Do not allow coolant to come into contact with the lower crankshaft bearing inner surface.

·

If any coolant comes into contact with the lower crankshaft bearing inner surface, replace the lower crankshaft bearing with a new one.


Hide 13411 5.INSTALL CRANKSHAFT

Z101186

NOTICE:

Clean the contact surface of each main journal and crank pin.


a.
A488512

i.

Apply new engine oil to the upper crankshaft bearing and install the crankshaft to the cylinder block sub-assembly.


Hide 11011 6.INSTALL CRANKSHAFT THRUST WASHER
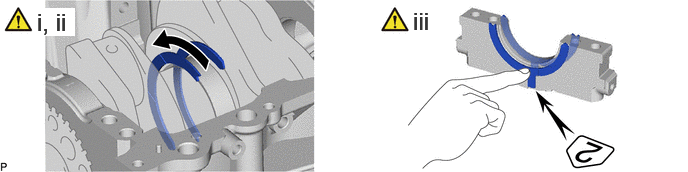
a.
A488503N01
0.385,0.083 0.781,0.375 0.396,0.292 18 true i, ii 4.302,0.073 4.604,0.354 0.302,0.281 18 true iii

i.

Push the crankshaft in the rear thrust direction to create clearance and install the upper crankshaft thrust washer to the No. 2 journal position with the oil groove facing the front of the engine.


ii.

Push the crankshaft in the forward thrust direction to create clearance and install the upper crankshaft thrust washer to the No. 2 journal position with the oil groove facing the rear of the engine.


iii.

Install the 2 lower crankshaft thrust washers to the No. 2 crankshaft bearing cap with the grooves facing outward.


Hide 7.INSTALL CRANKSHAFT BEARING CAP

a.
A488504C01
0.677,0.083 1.083,0.448 0.406,0.365 18 false i, ii 4.104,0.083 4.698,0.49 0.594,0.406 18 false iii, iv 0.677,2.083 1.031,2.438 0.354,0.354 18 false v 4.083,2.083 4.438,2.438 0.354,0.354 18 false vi 4.354,1.469 4.615,1.729 0.26,0.26 10 false *a
*a Less than 6 mm - -


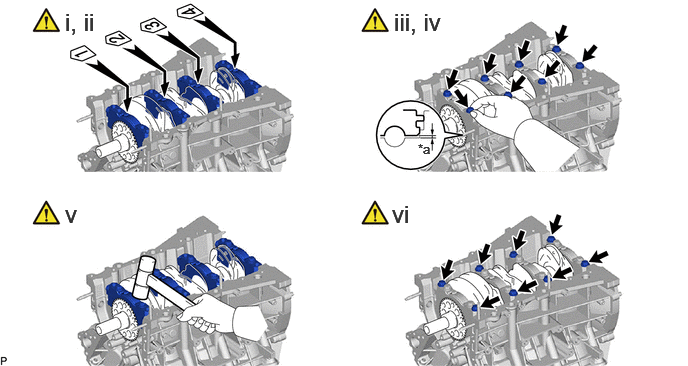
i.

Examine the front marks and numbers and set the crankshaft bearing caps on the cylinder block sub-assembly.


ii.

Apply a light coat of engine oil to the threads and under the heads of the crankshaft bearing cap set bolts.


iii.

Temporarily install the 8 crankshaft bearing cap set bolts to the inside positions.


iv.

Temporarily the 2 crankshaft bearing cap set bolts for each crankshaft bearing cap until the clearance between the crankshaft bearing cap and the cylinder block sub-assembly is less than 6 mm (0.236 in.).


v.

Using a plastic-faced hammer, lightly tap the crankshaft bearing cap to ensure a proper fit.


vi.

Apply a light coat of engine oil to the threads and under the heads of the crankshaft bearing cap set bolts and temporarily install the 8 crankshaft bearing cap set bolts to the outside positions.
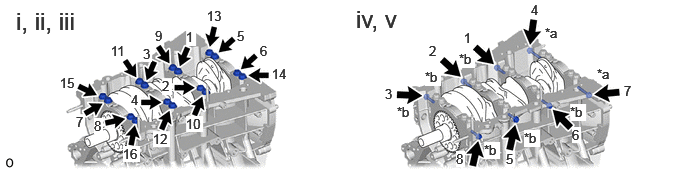


b.
A488508C01
0.167,0.073 1.01,0.427 0.844,0.354 18 false i, ii, iii 3.708,0.052 4.552,0.406 0.844,0.354 18 false iv, v 1.938,0.302 2.042,0.479 0.104,0.177 10 true 1 1.688,0.813 1.792,0.99 0.104,0.177 10 true 2 1.49,0.479 1.583,0.646 0.094,0.167 10 true 3 1.365,0.958 1.458,1.125 0.094,0.167 10 true 4 2.469,0.292 2.563,0.458 0.094,0.167 10 true 5 2.708,0.448 2.802,0.615 0.094,0.167 10 true 6 0.792,1.188 0.885,1.354 0.094,0.167 10 true 7 0.979,1.229 1.073,1.396 0.094,0.167 10 true 8 1.615,0.292 1.708,0.458 0.094,0.167 10 true 9 1.938,1.208 2.115,1.375 0.177,0.167 10 true 10 1.156,0.448 1.333,0.615 0.177,0.167 10 true 11 1.594,1.365 1.771,1.531 0.177,0.167 10 true 12 2.156,0.083 2.333,0.25 0.177,0.167 10 true 13 2.833,0.688 3.01,0.854 0.177,0.167 10 true 14 0.625,0.781 0.802,0.948 0.177,0.167 10 true 15 1.281,1.521 1.458,1.688 0.177,0.167 10 true 16 4.833,0.313 4.938,0.49 0.104,0.177 10 true 1 4.469,0.448 4.573,0.625 0.104,0.177 10 true 2 4.01,0.896 4.104,1.063 0.094,0.167 10 true 3 5.531,0.021 5.625,0.188 0.094,0.167 10 true 4 5.271,1.573 5.365,1.74 0.094,0.167 10 true 5 5.958,1.323 6.052,1.49 0.094,0.167 10 true 6 6.5,0.865 6.594,1.031 0.094,0.167 10 true 7 4.75,1.573 4.844,1.74 0.094,0.167 10 true 8 5.677,0.26 5.844,0.438 0.167,0.177 10 true *a 6.219,0.688 6.385,0.865 0.167,0.177 10 true *a 4.427,0.719 4.594,0.896 0.167,0.177 10 true *b 4.781,0.531 4.948,0.708 0.167,0.177 10 true *b 4.135,1.083 4.302,1.26 0.167,0.177 10 true *b 5.042,1.479 5.208,1.656 0.167,0.177 10 true *b 5.458,1.354 5.625,1.531 0.167,0.177 10 true *b 5.938,1.083 6.104,1.26 0.167,0.177 10 true *b
*a Bolt A *b Bolt B


i.

Step 1:

Uniformly tighten the 16 crankshaft bearing cap set bolts in several steps in the order shown in the illustration.

Torque:
61 N*m (622 kgf*cm, 45 ft.*lbf)


ii.

Step 2:

1. Mark the front side of the crankshaft bearing set cap bolts with paint.

2. Tighten the crankshaft bearing cap set bolts 90° in the order shown in step 1.


iii.

Check that the painted marks are now at a 90° angle to the front.


iv.

Install and uniformly tighten 8 new seal washers and the 8 bolts in several steps in the sequence shown in the illustration.

Torque:
25.7 N*m (262 kgf*cm, 19 ft.*lbf)

Standard Bolt:
Item Length
Bolt A 45 mm (1.77 in.)
Bolt B 30 mm (1.18 in.)


v.

Check that the crankshaft turns smoothly.


Hide 13101A 9.INSTALL PISTON PIN HOLE SNAP RING
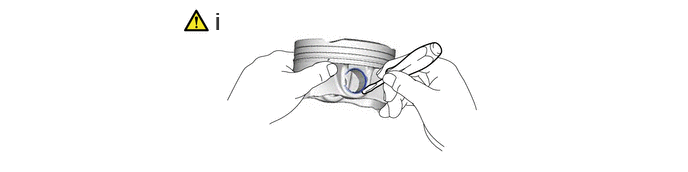
a.
A488509N01
2.24,0.073 2.521,0.427 0.281,0.354 18 false i

i.

Using a screwdriver, install a new piston pin hole snap ring to one side of the piston pin hole.

NOTICE:

Be sure that the end gap of the snap ring is not aligned with the pin hole cutout portion of the piston.


Hide 13101 10.INSTALL PISTON WITH PIN SUB-ASSEMBLY
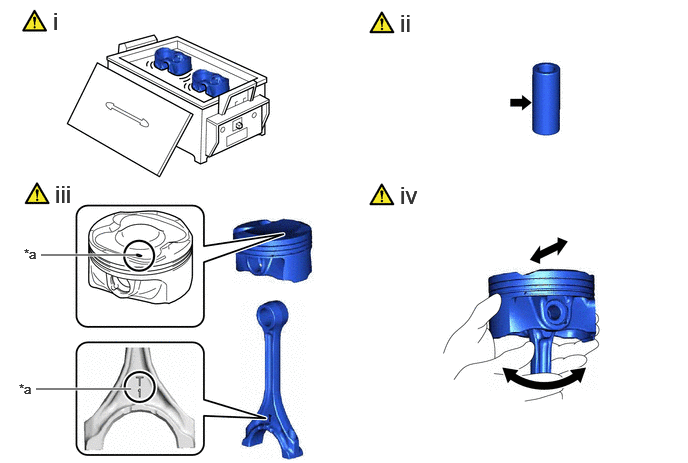
a.
A488510C01
0.427,2.656 1.417,2.656 true 0.375,4.052 1.365,4.052 true 0.198,3.969 0.469,4.25 0.271,0.281 10 false *a 0.25,2.563 0.521,2.844 0.271,0.281 10 false *a 0.552,0.073 0.906,0.469 0.354,0.396 18 false i 4.167,0.094 4.521,0.49 0.354,0.396 18 false ii 0.573,1.875 0.927,2.271 0.354,0.396 18 false iii 4.167,1.885 4.521,2.281 0.354,0.396 18 false iv
*a Front Mark - -


i.

Gradually heat the piston to approximately 80°C (176°F).


ii.

Coat the piston pin with engine oil.


iii.

Align the front marks of the piston and connecting rod, insert the connecting rod into the piston, and then push in the piston pin with your thumb until the pin comes into contact with the snap ring.

HINT:

The piston and pin are a matched set.


iv.

Check the fitting condition between the piston and piston pin by trying to move the piston back and forth on the piston pin.


Hide 13101A 11.INSTALL PISTON PIN HOLE SNAP RING
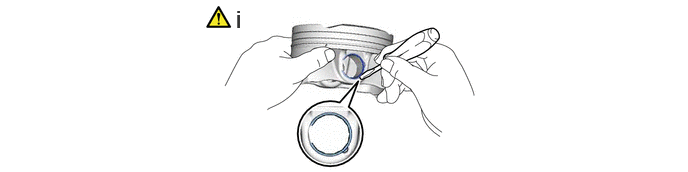
a.
A488511N01
2.458,0.052 2.74,0.406 0.281,0.354 18 false i

i.

Using a screwdriver, install a new piston pin hole snap ring to the other end of the piston pin hole.

NOTICE:

Be sure that the end gap of the snap ring is not aligned with the pin hole cutout portion of the piston.


Hide 13011 12.INSTALL PISTON RING SET

a.
A487743C01
2.542,5.229 2.75,5.229 2.75,5.229 3.25,4.885 true 4.729,2.073 4.729,1.594 true 2.677,1.323 3.396,1.323 true 2.594,1.552 3.313,1.552 true 2.677,1.729 3.396,1.729 true 4.667,2.885 4.958,3.104 0.292,0.219 10 false *1 6.063,2.896 6.354,3.135 0.292,0.24 10 false *2 2.719,4.667 3.01,4.885 0.292,0.219 10 false *3 3.563,3.802 3.865,4 0.302,0.198 10 false *4 3.583,5.521 3.833,5.781 0.25,0.26 10 false *5 2.365,5.146 2.667,5.365 0.302,0.219 10 false *a 4.667,2.094 4.885,2.302 0.219,0.208 10 false *b 0.354,0.26 0.74,0.667 0.385,0.406 18 false i 4.188,0.26 4.573,0.667 0.385,0.406 18 false ii 2.646,3.313 3.031,3.719 0.385,0.406 18 false iii 2.958,5.271 3.25,5.49 0.292,0.219 10 false *1 2.958,4.063 3.25,4.302 0.292,0.24 10 false *2 3.438,1.229 3.688,1.49 0.25,0.26 10 false *5 3.438,1.635 3.74,1.833 0.302,0.198 10 false *4 3.344,1.469 3.635,1.688 0.292,0.219 10 false *3
*1 No. 1 Compression Ring *2 No. 2 Compression Ring
*3 Oil Ring (Expander) *4 Oil Ring (Lower Side Rail)
*5 Oil Ring (Upper Side Rail) - -
*a Front Mark *b Painted Mark
V100135

Right Side - -


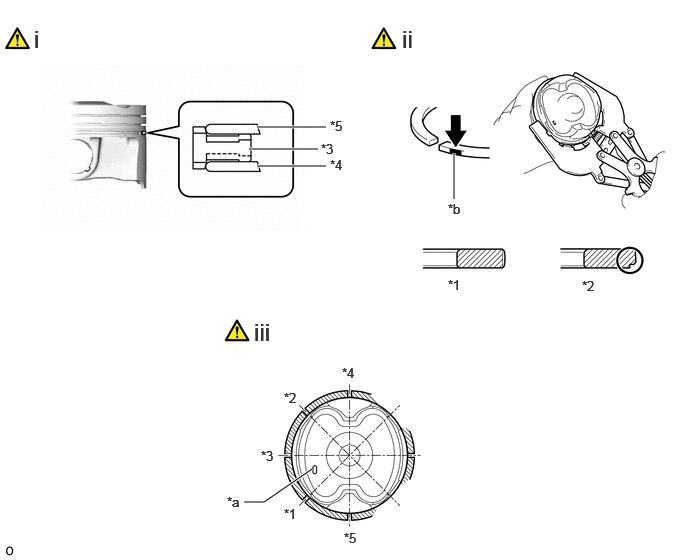
i.

Install the oil ring (expander) and 2 oil rings (side rails) by hand.


ii.

Using a piston ring expander, install the No. 1 compression ring and No. 2 compression ring.


iii.

Position the piston rings so that the ring ends are as shown in the illustration.


Hide 13041 13.INSTALL CONNECTING ROD BEARING
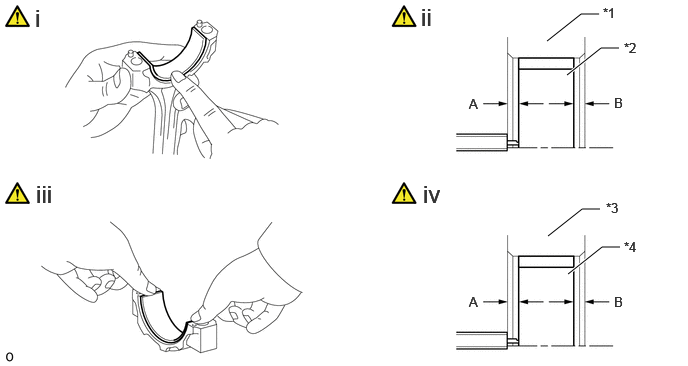
a.
A487748C01
5.698,0.427 6.052,0.146 6.052,0.146 6.24,0.146 true 5.906,0.781 6.26,0.5 6.26,0.5 6.448,0.5 true 5.708,2.458 6.063,2.177 6.063,2.177 6.25,2.177 true 5.917,2.854 6.271,2.573 6.271,2.573 6.458,2.573 true 6.281,0.052 6.51,0.313 0.229,0.26 10 false *1 6.5,0.417 6.823,0.677 0.323,0.26 10 false *2 0.365,0.042 0.729,0.396 0.365,0.354 18 false i 4.385,0.031 4.75,0.385 0.365,0.354 18 false ii 0.375,1.875 0.74,2.229 0.365,0.354 18 false iii 4.406,1.875 4.771,2.229 0.365,0.354 18 false iv 4.885,1 5.208,1.26 0.323,0.26 10 false A 6.396,0.99 6.719,1.25 0.323,0.26 10 false B 6.313,2.083 6.542,2.344 0.229,0.26 10 false *3 6.5,2.49 6.729,2.75 0.229,0.26 10 false *4 6.396,3.063 6.719,3.323 0.323,0.26 10 false B 4.885,3.063 5.208,3.323 0.323,0.26 10 false A
*1 Connecting Rod Sub-assembly *2 Connecting Rod Bearing
*3 Connecting Rod Cap *4 Connecting Rod Bearing


i.

Install the connecting rod bearing to the connecting rod sub-assembly.


ii.

Using a vernier caliper, measure the distance between the connecting rod sub-assembly edge and connecting rod bearing edge.

Dimension A - B or B - A:

0 to 0.7 mm (0 to 0.0276 in.)


NOTICE:
·

Clean the contact surface of the connecting rod bearing and connecting rod sub-assembly.

·

Do not apply engine oil to the connecting rod bearing or its contact surface.


iii.

Install the connecting rod bearing to the connecting rod cap.


iv.

Using a vernier caliper, measure the distance between the connecting rod cap edge and connecting rod bearing edge.

Dimension A - B or B - A:

0 to 0.7 mm (0 to 0.0276 in.)


NOTICE:
·

Clean the contact surface of the connecting rod bearing and connecting rod cap.

·

Do not apply engine oil to the connecting rod bearing or its contact surface.


Hide 14.INSTALL PISTON WITH CONNECTING ROD

a.
A487749C01
2.531,4.26 2.708,4.26 2.708,4.26 3.188,3.979 true 2.885,4.323 3.188,4.573 0.302,0.25 10 false *1 2.896,3.146 3.156,3.354 0.26,0.208 10 false *2 2.656,3.75 2.948,3.917 0.292,0.167 10 false *3 3.5,2.896 3.76,3.115 0.26,0.219 10 false *4 3.5,4.594 3.75,4.813 0.25,0.219 10 false *5 0.365,0.031 0.667,0.365 0.302,0.333 18 false i 2.365,4.167 2.667,4.375 0.302,0.208 10 false *a 2.656,2.771 2.958,3.104 0.302,0.333 18 false ii
*1 No. 1 Compression Ring *2 No. 2 Compression Ring
*3 Oil Ring (Expander) *4 Oil Ring (Lower Side Rail)
*5 Oil Ring (Upper Side Rail) - -
*a Front Mark - -


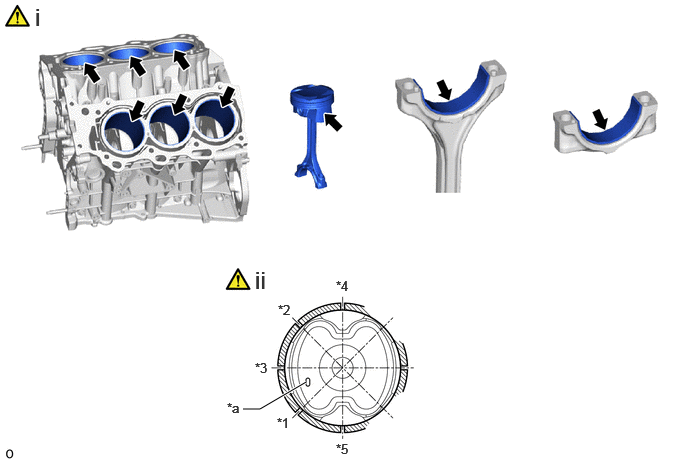
i.

Apply engine oil to the cylinder walls, pistons and surfaces of the connecting rod bearings.


ii.

Check the positions of the piston ring ends.
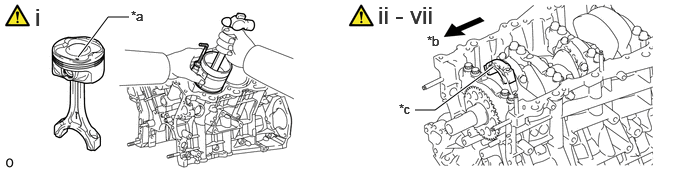


b.
A487750C01
0.813,0.594 1.125,0.177 1.125,0.177 1.344,0.177 true 5.135,0.698 4.531,1.146 4.531,1.146 4.323,1.146 true 1.365,0.083 1.635,0.344 0.271,0.26 10 false *a 4.448,0.344 4.76,0.542 0.313,0.198 10 false *b 4.156,1.052 4.438,1.281 0.281,0.229 10 false *c 0.365,0.031 0.667,0.344 0.302,0.313 18 false i 3.938,0.01 4.646,0.479 0.708,0.469 18 false ii - vii
*a Front Mark *b Front
*c Protrusion - -


i.

Using a hammer handle and piston ring compressor, press a piston with connecting rod into each cylinder with the front mark of the piston facing forward.


ii.

Set the connecting rod cap so that the protrusion is facing the correct direction.

NOTICE:

Match the numbered connecting rod cap with the connecting rod sub-assembly.


iii.

Apply a light coat of engine oil to the threads and under the heads of the connecting rod bolts.


iv.

Step 1:

1. Install and alternately tighten the connecting rod bolts of the connecting rod cap in several steps.

Torque:
24.5 N*m (250 kgf*cm, 18 ft.*lbf)

2. Mark the front side of each connecting rod capbolt with paint.


v.

Step 2:

Tighten the connecting rod bolts 90°.


vi.

Check that the painted marks are now at a 90° angle to the front.


vii.

Check that the crankshaft turns smoothly.


Hide 15.INSPECT CONNECTING ROD THRUST CLEARANCE